Showing 302 items matching "hands up for hands on"
-
 Federation University Historical Collection
Booklet, UBTec, 2008
... ...Hands up for hands on...UBTec is another opion for senior secondary students providing accredited, hands on learnign for Year 11 and Year 12 students in an adult learning environment. UBTec Enrols students who have not comnpleted Year 12. UBTec FedTec Technical Education Hands up for hands ...UBTec is another opion for senior secondary students providing accredited, hands on learnign for Year 11 and Year 12 students in an adult learning environment. UBTec Enrols students who have not comnpleted Year 12.Four page promotional pamphlet for UBTec ... technical education for Years 11 and 12 students. ubtec, fedtec, technical education, hands up for hands on -
 Bendigo Historical Society Inc.
Postcard - POSTCARD. GREAT EXTENDED HUSTLERS MINE, 1865
... Metal poppet head in centre of image, corrugated iron mining sheds on left hand side. Ladder extending up right hand side of poppet head. ...Metal poppet head in centre of image, corrugated iron mining sheds on left hand side. Ladder extending up right hand side of poppet head. ...Sepia coloured postcard. Metal poppet head in centre of image, corrugated iron mining sheds on left hand side. Ladder extending up right hand side of poppet head. On back: ROYAL HISTORICAL SOCIETY OF VICTORIA. Bendigo Branch Great Great Extended Hustlers. Locality. Hustlers Hill, Nth Bendigo Formed 1865 - Last production 1921 Depth of Shaft - 3470 feet Poppet Legs - Steel, 70 feet high Winding Engine: First motion 8ft. Drums. Gold Very Rich Total yield - 300,000 ozs. Dividends pounds 375,000 -
 Flagstaff Hill Maritime Museum and Village
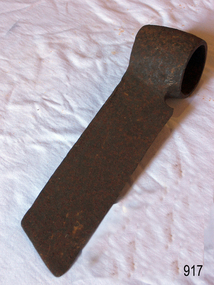
Tool - Froe, Late 19th to Early 20th century
... up through this socket. But some froes had eyes similar to those on axes for handles that were wedged. The froe handle is held in an upright position in one hand while the other hand drives the top of the blade downward with a wood froe club or mallet. ...up through this socket. But some froes had eyes similar to those on axes for handles that were wedged. The froe handle is held in an upright position in one hand while the other hand drives the top of the blade downward with a wood froe club or mallet. ...A froe was used for splitting, or riving, wood in the early days and was a skill practiced by craftsmen who made boards, shingles, c lapboards, fences, basket splints, chair parts, wagon spokes, lath, and more. Our ancestors used axes, gluts or wedges, froes, draw knives and spelk planes for splitting wood. The froe was designed in many sizes and designs for splitting timber. It is typically an L-shaped tool made up of a wedge-shaped blade with a dull, but not blunt, knife edge and a wood handle. Blades were usually straight with a socket forged at one end for a handle, but curved blades were also made. Most handles were round and tapered and were inserted up through this socket. But some froes had eyes similar to those on axes for handles that were wedged. The froe handle is held in an upright position in one hand while the other hand drives the top of the blade downward with a wood froe club or mallet. After a split is started, the froe is wiggled downward to lengthen it until the split is complete. Most old froes were hand forged, but they were also available in many catalogues. The 1873 D.R. Barton American catalogue offered straight froes at 12 1/2 cents per inch. You can still buy new froes from many tool manufacturers today.A tool that has not changed in design or use since its inception several hundred years ago to split timber for various uses.Froe, also called cooper's froe or stave froe, without handle.Noneflagstaff hill, warrnambool, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, froe, cooper's froe, stave froe, wood splitter, carpenders tools, coopers tool, splitting timber -
 Flagstaff Hill Maritime Museum and Village
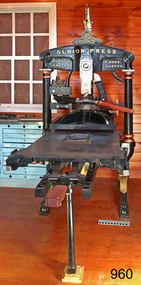
Equipment - Printing Press, Harrild and Sons, 1866
... up to good working order and organised the supply of appropriate printer’s type. The Albion hand operated printing press is significant for producing the first newspaper in Coleraine, Western Victoria and continuing production for over 100 years. The Albion is technologically significant as a working example of a hand ...This Albion printing press was manufactured by Harrild & Sons of London and exported in 1868 from London to the colonial Western Victoria town of Coleraine, population of 700 at that time. It was installed in the Colerain Albion printing office. It was used to print the first edition of the Coleraine Albion newspaper in 1868 and continued until publication ceased in 1974. The Albion Press is still being used today by a volunteer printer in the “Examiners Office” in the village at Flagstaff Hill. Amongst the items produced are printed paper bags for the Tea Rooms and posters for visitors. ALBION PRINTING PRESS The Albion press was invented and manufactured in London by Richard Whittaker Cope around 1820 and was still being produced in the 1930s. The Albion was manufactured under licence by several companies from the 1850s onwards, one of which was Harrild & Sons of Fleet Works, London. Harrild & Sons describes its business as “printing materials manufacturer”. The business was established in 1807 by Robert Harrild and named R. Harrild & Co. In 1813 he showed that rollers could be used to ink a printing plate instead of inking balls, the method in use at the time. He then established a company to make the rollers. Eventually his company would make other printing materials and equipment. Robert’s sons joined him in the 1830s, when the company was renamed Harrild & Sons, and they continued to run the company after his death in 1853 and up until the mid-1900s. COLERAINE ALBION PRINTING OFFICE The Coleraine Albion Printing Office was established by W.L. Ambler. The first issue of the Coleraine Albion was dated 4th January 1868. Arrangements had been made to receive news from Melbourne, nearby provinces, other colonies and England. The second issue on 18 January 1868 printed articles from many agencies, including the Melbourne Age and the Warrnambool Examiner. The Albion office was sold to William Hatherleigh, formerly of Portland, in October 1868. Thereafter the Albion office had many owners. The last was L. A. & E. Oliver, who took over in January 1972 and was the last to be stated as printers and publishers of the Coleraine Albion. The office was wound up in 1974. The Albion Press and other equipment was distributed to Star printing in Terang. Star Printing donated the Albion press to Flagstaff Hill Maritime Village around 1980 and Stan Philp, owner of Philprint in Warrnambool, transported it to Warrnambool, brought it up to good working order and organised the supply of appropriate printer’s type. The Albion hand operated printing press is significant for producing the first newspaper in Coleraine, Western Victoria and continuing production for over 100 years. The Albion is technologically significant as a working example of a hand operated printer from the mid-19th century. The use of the printer is demonstrated by volunteers at Flagstaff Hill, printing items such as lolly and treat bays for use in the Village. The Albion is socially significant for its role in the isolated provincial colony, providing communication with the outside world, both in Australia and overseas. Newspaper printers were often amongst the first businesses of a small town. Printing press; hand operated Albion Press, Patent 2105. The machine has an upright iron frame at the back that supports the upper press that has a wooden handled metal bar is attached. The frame and legs support a thick metal flatbed. A metal leg supports the front of the press bed. The iron work is painted black with gold highlights. The decorative legs are finished with the golden feet of an animal. The frame above the metal bed includes a crown shaped finial symbol above the maker’s emblem. The maker’s details and the name of the printer are embossed on the upright frame. A plaque with the patent number is below a Lion and Unicorn emblem.Embossed maker’s emblem [A red cross - above a double ring – square inside ring – three banners below ring]. - Inside the double rings “PRINTING MATERIALS MANUFACTURE” - Inside the square, intertwined text “H & S” [representing Harrild & Sons] - Inside the three banners ““FLEET” “WORKS.” “LONDON.E.C.” Embossed across the shoulders “ALBION PRESS / HARRILD & SONS, / MAKERS LONDON.” Emblem above plaque [Lion and Unicorn] Embossed on the plaque “PATENT / 2105” Stamped into upright machine part above the printing bed “2105 / 1866” flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, albion press, printing press, 1866 printing press, printing equipment, communications, coleraine albion printing office, coleraine newspaper, albion newspaper, south west victoria newspapers, harrild and sons london, richard whittaker cope, star printing terang, philprint, coleraine albion, hand operated press -
 Flagstaff Hill Maritime Museum and Village
Container - Ink Bottle, 19th to early-20th century
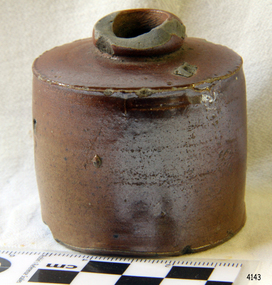
... This ink well is historically significant as it represents methods of hand written communication that were still common up until the mid-20th century, when fountain pens and ballpoint pens took over in popularity and convenience. flagstaff hill warrnambool shipwreck coast flagstaff hill maritime museum flagstaff hill maritime village maritime museum great ocean road shipwreck artefact writing equipment writing accessory office equipment stationery domestic stoneware clay ceramic pottery ink well inkwell ink bottle penny ink well nib pen dip pen ink hand writing record keeping household business vintage blotting paper dwarf bottle Ink bottle or ink well, sometimes called a Penny Ink Well. ...This design of ink bottle or ink well was commonly referred to as a ‘penny ink well’ because it was very inexpensive to produce. It is also known as a dwarf bottle. Pen and ink has been in use for hand writing from about the seventh century up until the mid-20th century. Up until around the mid-19th century a quill pen made from a bird’s feather was used. In the 1850s the steel point pen was invented and could be manufactured on machines in large quantities. In the 1880s a successful portable fountain pen was designed, giving a smooth flowing ink and ease of use. Ink wells, used with steel nib dip pens, were commonly used up until the mid-20th century. The pens only held a small amount of ink so users had to frequently dip the nib of the pen into an ink well for more ink. Hand writing with pen and ink left wet writing on the paper, so blotting paper was carefully used to absorb the excess ink and prevent smudging. Ink could be purchased, ready to use, or in the powdered form, which needed to be mixed with water. After the invention of fountain pens, which had a reservoir of ink, and then ballpoint pens, which also had ink that flowed freely, the dip pen was slowly replaced. However, artisans continue to use nib pens to create beautiful calligraphy.This ink well is historically significant as it represents methods of hand written communication that were still common up until the mid-20th century, when fountain pens and ballpoint pens took over in popularity and convenience.Ink bottle or ink well, sometimes called a Penny Ink Well. Cylindrical body, salt-glazed, brown ceramic stoneware bottle, handmade. Stoneware bottle. flagstaff hill, warrnambool, shipwreck coast, flagstaff hill maritime museum, flagstaff hill maritime village, maritime museum, great ocean road, shipwreck artefact, writing equipment, writing accessory, office equipment, stationery, domestic, stoneware, clay, ceramic, pottery, ink well, inkwell, ink bottle, penny ink well, nib pen, dip pen, ink, hand writing, record keeping, household, business, vintage, blotting paper, dwarf bottle -
 Flagstaff Hill Maritime Museum and Village
Tool - Hand Adze, A Mathieson and Son, First quarter of the 20th Century
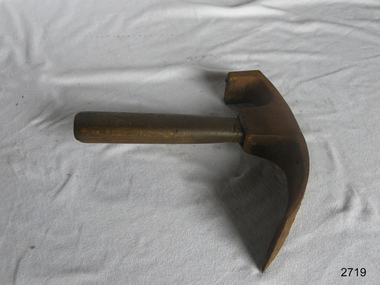
... hand woodworking, and as a hoe for agriculture and horticulture. Two basic forms of an adze are the hand adze (short hoe) a short handled tool swung with one hand and the foot adze (hoe) a long handled tool capable of powerful swings using both hands, the cutting edge usually striking at foot or shin level. Mathieson & Sons Maker: In 1792 John Manners had set up...hand woodworking, and as a hoe for agriculture and horticulture. Two basic forms of an adze are the hand adze (short hoe) a short handled tool swung with one hand and the foot adze (hoe) a long handled tool capable of powerful swings using both hands, the cutting edge usually striking at foot or shin level. Mathieson & Sons Maker: In 1792 John Manners had set up ...An adze is an ancient and versatile cutting tool similar to an axe but with the cutting edge perpendicular to the handle rather than parallel. Adzes are used for smoothing or carving wood in hand woodworking, and as a hoe for agriculture and horticulture. Two basic forms of an adze are the hand adze (short hoe) a short handled tool swung with one hand and the foot adze (hoe) a long handled tool capable of powerful swings using both hands, the cutting edge usually striking at foot or shin level. Mathieson & Sons Maker: In 1792 John Manners had set up a workshop making woodworking planes at 14 Saracens Lane Glasgow. He also had employed an apprentice Alexander Mathieson (1773-1851). But in the following year at Saracen's Lane, the 1841 census describes Alexander Mathieson as a master plane-maker now at 38 Saracen Lane with his son Thomas Adam working with him as a journeyman plane-maker. Presumably, Alexander must have taken over the premises and business of John Manners. Now that the business had Thomas Adam Mathieson working with his father it gradually grew and became more diversified, and it is recorded at the time by the Post-Office Glasgow Annual Directory that by 1847-1848 Alexander Mathieson was a “plane, brace, bit, auger & edge tool maker” In 1849 the firm of James & William Stewart at 65 Nicolson Street, Edinburgh was taken over and Thomas was put in charge of the business, trading under the name Thomas A. Mathieson & Co. as plane and edge-tool makers. Thomas's company went on to acquire the Edinburgh edge-tool makers “Charles & Hugh McPherson” and took over their premises in Gilmore Street. In the Edinburgh directory of 1856/7, the business is recorded as being Alexander Mathieson & Son, plane and edge-tool makers at 48 Nicolson Street and Paul's Work, Gilmore Street Edinburgh. The 1851 census Alexander is recorded as working as a tool and plane-maker employing eight men. Later that year Alexander died and his son Thomas took over the business. Under the heading of an edge-tool maker in the 1852/3 Post-Office Glasgow Annual Directory the firm is now listed as Alexander Mathieson & Son, with further entries as "turning-lathe and vice manufacturers". By the early 1850s, the business had moved to 24 Saracen Lane. The directory for 1857/8 records that the firm had moved again only a few years later to East Campbell Street, off the Gallowgate area, and that through further diversification was also manufacturing coopers' and tinmen's tools. The ten-yearly censuses report the firm's growth in 1861 stating that Thomas was a tool manufacturer employing 95 men and 30 boys; in 1871 he had 200 men working for him and in 1881 300 men. By 1899 the firm had been incorporated as Alexander Mathieson & Sons Ltd, even though only Alexander's son Thomas appears ever to have joined the firm so the company was still in his fathers' name. In September 1868 Thomas Mathieson put a notice in the newspapers of the Sheffield & Rotherham Independent and the Sheffield Daily Telegraph stating that his firm had used the trade-mark of a crescent and star "for some time" and that "using or imitating the Mark would be proceeded against for infringement". The firm had acquired its interest in the crescent-and-star mark from the heirs of Charles Pickslay, the Sheffield cutler who had registered it with the Cutlers' Company in 1833 and had died in 1852. The year 1868 seems also to be the one in which the name Saracen Tool Works was first adopted; not only does it figure at the foot of the notice in the Sheffield press, it also makes its first appearance in the firm's entry in the Post-Office Glasgow Annual Directory in the 1868/9 edition. As Thomas Mathieson's business grew, so too did his involvement in local public life and philanthropy. One of the representatives of the third ward on the town council of Glasgow, he became a river bailie in 1868, a magistrate in 1870 and a preceptor of Hutcheson's Hospital in 1878. He had a passion for books and was an "ardent Ruskinian". He served on the committee handling the bequest for the setting up of the Mitchell Library in Glasgow. When he died at Coulter Maynes near Biggar in 1899, he left an estate worth £142,764. The firm of Alexander Mathieson & Sons was one of the leading makers of hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperages and other industries, both locally and far and wide.Hand Adze or Cooper's adze No 4 A Mathieson & Sons Glasgowflagstaff hill, warrnambool, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, adze mathieson & sons, cooperage tools, woodworking, barrel making, working timber, joiners tools, carpenters tools -
 Flagstaff Hill Maritime Museum and Village
Equipment - Pump, circa 1930's - 1940's
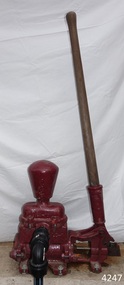
... hand operated, constant flow pressure pump. It would have been used to pump fluids from one area to another, for example from a dam to a tank or used as a bilge pump on a small vessel, mounted on the vessel’s bulkhead, floor or deck. This type of hand pump is sometimes called a ‘Reciprocating Suction Pump’. It has a mechanical pumping action of the lever moves the piston inside the pump up and down. The water is lifted from below the pump through the inlet pipe and into the pump’s cylinder. This action causes the lower valve to close and the piston’s valve opens and the pressure within the pump forces the water out of the pump through the exit pipe. The limitation of this type of pump is that it can only raise the water a maximum of about 7 metres from beneath the ground and yields 24-26 Litres per minute. This type of pump could be used for many purposes such as pumping water or fuel. McPherson’s 1940’s advertisement proclaims “For all jobs on the land – irrigation, spraying, tank, plumbing, fire-fighting – there’s a suitable “Ajax” pump. Send us the details of you pumping problem. Our Expert’s advice will help you choose the right pump – the one that will give you most years of PROFITABLE PUMPING.” (The Australasian (Melbourne) Sat. 26th October 1940.) McPherson’s Pty Ltd, the manufacturer, advertised a similar pump to this one in The Australasian (Melbourne) in 1936, calling it the Ajax Double Acting Hand...hand operated, constant flow pressure pump. It would have been used to pump fluids from one area to another, for example from a dam to a tank or used as a bilge pump on a small vessel, mounted on the vessel’s bulkhead, floor or deck. This type of hand pump is sometimes called a ‘Reciprocating Suction Pump’. It has a mechanical pumping action of the lever moves the piston inside the pump up and down. The water is lifted from below the pump through the inlet pipe and into the pump’s cylinder. This action causes the lower valve to close and the piston’s valve opens and the pressure within the pump forces the water out of the pump through the exit pipe. The limitation of this type of pump is that it can only raise the water a maximum of about 7 metres from beneath the ground and yields 24-26 Litres per minute. This type of pump could be used for many purposes such as pumping water or fuel. McPherson’s 1940’s advertisement proclaims “For all jobs on the land – irrigation, spraying, tank, plumbing, fire-fighting – there’s a suitable “Ajax” pump. Send us the details of you pumping problem. Our Expert’s advice will help you choose the right pump – the one that will give you most years of PROFITABLE PUMPING.” (The Australasian (Melbourne) Sat. 26th October 1940.) McPherson’s Pty Ltd, the manufacturer, advertised a similar pump to this one in The Australasian (Melbourne) in 1936, calling it the Ajax Double Acting Hand ...This pump is an Ajax Type L2 Series A model, made and sold by McPherson’s Pty Ltd of Melbourne circa 1930’s to 1940’s, is a mechanical, hand operated, constant flow pressure pump. It would have been used to pump fluids from one area to another, for example from a dam to a tank or used as a bilge pump on a small vessel, mounted on the vessel’s bulkhead, floor or deck. This type of hand pump is sometimes called a ‘Reciprocating Suction Pump’. It has a mechanical pumping action of the lever moves the piston inside the pump up and down. The water is lifted from below the pump through the inlet pipe and into the pump’s cylinder. This action causes the lower valve to close and the piston’s valve opens and the pressure within the pump forces the water out of the pump through the exit pipe. The limitation of this type of pump is that it can only raise the water a maximum of about 7 metres from beneath the ground and yields 24-26 Litres per minute. This type of pump could be used for many purposes such as pumping water or fuel. McPherson’s 1940’s advertisement proclaims “For all jobs on the land – irrigation, spraying, tank, plumbing, fire-fighting – there’s a suitable “Ajax” pump. Send us the details of you pumping problem. Our Expert’s advice will help you choose the right pump – the one that will give you most years of PROFITABLE PUMPING.” (The Australasian (Melbourne) Sat. 26th October 1940.) McPherson’s Pty Ltd, the manufacturer, advertised a similar pump to this one in The Australasian (Melbourne) in 1936, calling it the Ajax Double Acting Hand Pump. In 1942 another advertisement advised that a representative for a fire-fighting equipment supplier was visiting the western district of Victoria. The company could now supply double-action two-spray Ajax pumps at lower prices than similar pumps the district had recently purchased from Adelaide. McPHERSON’S FOUNDER and COMPANY TIMELINE 1860 – Thomas McPherson, a Scottish immigrant (c. 1853 ), founded McPherson’s in Melbourne, supplying pig iron (lead ingots imported as ballast in ships) to local manufacturers. 1882 – Thomas McPherson established a warehouse in Collins St Melbourne and included tools, steam fittings and machinery in his wares. The business expanded to include steam saw mills and became known as Thomas McPherson and Sons (William Murray and Edward). 1888 – Thomas passed away and his sons inherited the business. In 1896 William Murray became the sole proprietor after his brother Edward’s death. 1900 – The firm expanded, establishing Acme Bolt Company to manufacture nuts and bolts. 1912 – McPhersons Pty Ltd established a machinery warehouse and showroom in 554-556 Collins St Melbourne. McPherson’s went on to establish branches in Sydney (1911), Adelaide (1921) and Perth (1930) 1917 - McPherson’s supplied ‘dog spikes’ for the transcontinental railway, running from Eastern to Western Australia. 1918 – A tool works set up in Kensington, Melbourne, manufacturing Macson lathes and made machine tools that previously had to be imported. 1924 – The Bolt Works was transferred to a new building in Melbourne. McPhersons began making pumps. 1929 – McPherson retired. His son (Sir) William Edward McPherson (known as ‘WE’), was born in Hawthorne, Melbourne, in 1898. After his education he began work in his father’s Melbourne hardware and machinery business He took over as governing director when his father retired. 1929-1932 – McPherson’s supplied thousands of tons of rivets from its Richmond (Melbourne) Bolt Works for the construction of the Sydney Harbour Bridge. 1936 – McPherson’s Pty Ltd is advertising Ajax Pumps in newspapers 1934 – McPhersons purchased the property adjoining the warehouse in Collins Street, and during 1935-1936 built a new office and showrooms on the site of 546-445 Collins St. 1939 - McPherson’s acquired the Tool Equipment Co. Pty. Ltd and Associated Machine Tools Australia Pty Ltd was formed to separate McPherson’s machine-tool manufacturing and merchandising interests. 1939 – Ajax Pump Works, a foundry and pump manufacturing plant, was established in Tottenham, Melbourne, and the Ajax Bolt and Rivet Co Pty Ltd began manufacturing in New Zealand. 1944 - McPherson’s became a public company, McPherson’s Ltd. 1948 - The Ajax Pump Foundry opened at Kyneton, Victoria and in the post war years it grew to became a large manufacturer. 1980’s – Ajax Pumps brochure lists the address as 6 Buckhurst St, South Melbourne, Vic 3205 with the Telephone number 03 669 3588 1988 - Ajax Pumps acquired the Forrers Company, which was established in 1921. Manufacturing in Ipswich, Queensland, specialising in submersible sewage pumps. 1991 – KSB Ajax was formed, bringing together the companies KSB and Ajax Pumps 1993 – Manufacturing was moved to state-of-the-art premises in Tottenham, Victoria 2001 - The Forrers facility was moved to Tottenham. 2007 - Company name KSB Ajax Pumps was changed to KSB Australia Pty Ltd. 2009 - KSB Australia opened a branch in Townsville, Queensland. 2011 - KSB Australia moved to its dedicated Water and Waste Water Competence Centre in Bundamba, Queensland. DISPLAY OF THIS AJAX PUMP This pump was installed at Flagstaff Hill Maritime Village as part of a working display in the village by the Friends of Flagstaff Hill, in acknowledgement of the dedicated involvement of one of its long serving members, Bob Crossman. The display was officially opened 31st March 2018 and incorporates a restored Furphy Tank and Water Pipe Stand. The pump is used to draw water from the lake, through the water stand pipe and into the reconditioned Furphy Tank. This Ajax pump made by McPherson’s Pty Ltd is significant for its association with McPherson’s, a prominent manufacturer of hardware in Victoria. McPherson’s is famous for supplying ‘dog-spikes’ for the transcontinental railway (eastern to western Australia, 1917) and rivets for the Sydney Harbour Bridge (1929-1932). The Ajax pump is also of significance because of its association with McPherson’s Governing Director (Sir) William McPherson, former premier and treasurer in Victoria 1928-1929. The former McPherson’s Pty Ltd building in Collins Street Melbourne is now on the Victorian Heritage Register VHR H0942 This pump is representative of mechanical pumps popular in the early to mid-1900’s and still used today. Hand operated pressure pump, double acting. Cast metal case, painted red, with steel hose attachments and long metal lever. Pump is bolted to wooden plank. Model of pump is AJAX, Type L2, Series A pump. Embossed on lower section of pump "L2 - 10", "L2 - -1", "AJAX" “(?) –2-1” Embossed on lower handle “3-7” “L – 4” Embossed on attached plate “FOR SPARE PARTS / TYPE L2 / SERIES A / PUMP ASSEMBLED BY T R” Manufactured by McPherson’s Pty Ltd of Melbourne circa 1930’s - 1940’s.flagstaff hill, warrnambool, flagstaff hill maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, ajax pump works tottenham melbourne, ajax pump factory kyneton, william edward mcpherson, thomas mcpherson of melbourne, mcpherson’s pty ltd melbourne, acme bolt company, tool equipment co. pty. ltd, associated machine tools australia pty ltd, ajax bolt and rivet co. pty ltd new zealand, forrers company ipswich queensland, ksb ajax pumps, ksb australia pty ltd, macson lathes, tool manufacturer early to mid- 20th century, ajax double acting hand pump, ajax type l2 series a pump, qisjax pumps, water pump 1940’s, fuel pump 1940’s, hand operated constant flow pressure pump, reciprocating suction pump, agricultural hand pump, plumber’s hand pump, portable hand pump -
 Federation University Historical Collection
Postcard, Hands Across the Sea. New Zealand, Circa 1910
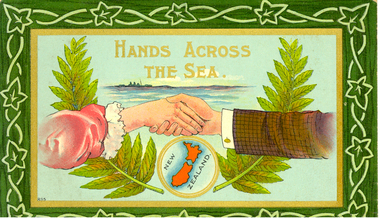
... Hand-coloured postcard in which the picture is framed by a border of a leaf and vine pattern. The picture is of the lower arms of a woman from the left hand side of the card and a man from the right hand side of the card shaking hands in the middle. Behind and below the hands is a small map of New Zealand in a golden circle. New Zealand fern is positioned from the circle up...Hand-coloured postcard in which the picture is framed by a border of a leaf and vine pattern. The picture is of the lower arms of a woman from the left hand side of the card and a man from the right hand side of the card shaking hands in the middle. Behind and below the hands is a small map of New Zealand in a golden circle. New Zealand fern is positioned from the circle up ...Frank Wright was a renown resident of Smeaton, where he was born. He lived at Laura Villa, and attended Smeaton State School. His father William was a gold miner and his mother's name was Sarah. Sarah spent six months in New Zealand in 1910. William and Sarah's family won many singing and instrumental awards. Frank was tutored by Percy Code and was awarded a gold medal for the highest marks in the ALCM examinations in the British Colonies at the age of seventeen years. He became the Australian Open Cornet Champion by the age of eighteen. A year later, Frank conducted the City of Ballarat Band, and later the Ballarat Soldiers’ Memorial Band. He formed the Frank Wright Frisco Band and Frank Wright and his Coliseum Orchestra. These bands won many South Street awards, and Frank as conductor won many awards in the Australian Band Championship contest. In 1933 Frank Wright sailed to England to conduct the famous St Hilda’s Band and was later appointed Musical Director of the London County Council, where he organized many amazing concerts in parks, in and around the London district. He was made Professor of Brass and Military Band Scoring and conducted at the Guildhall of Music and Drama. Frank was often invited to adjudicate Brass Band Championships around Europe, in Australia, including South Street and in New Zealand. The Frank Wright Medal at the Royal South Street competition is awarded to an individual recognized as making an outstanding contribution to brass music in Australia.Hand-coloured postcard in which the picture is framed by a border of a leaf and vine pattern. The picture is of the lower arms of a woman from the left hand side of the card and a man from the right hand side of the card shaking hands in the middle. Behind and below the hands is a small map of New Zealand in a golden circle. New Zealand fern is positioned from the circle up behind the arms to the top of the card on both sides and above the hands is a depiction of a ship sailing on the sea.The postcard contains a message to Frank Wright from his mother who is visiting New Zealand.frank wright, sarah wright, new zealand, postcard -
 Flagstaff Hill Maritime Museum and Village
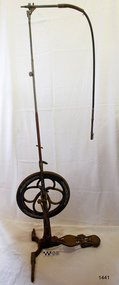
Equipment - Dentist Drill, Late 19th century
... hand tightened screw with a round knob. On the post just above the frame is a short metal, horizontal bar (to hold the hand-piece when it is not in use). A narrow tubular arm is attached to the top of the stand at a right angle and can move up and down. At the end of the arm is a firmly fixed, flexible rubber hose protected for a short distance by a sheath of thin metal. At the end of the hose there is a fitting where the drill’s hand...hand tightened screw with a round knob. On the post just above the frame is a short metal, horizontal bar (to hold the hand-piece when it is not in use). A narrow tubular arm is attached to the top of the stand at a right angle and can move up and down. At the end of the arm is a firmly fixed, flexible rubber hose protected for a short distance by a sheath of thin metal. At the end of the hose there is a fitting where the drill’s hand ...The design of this and other similar treadle powered dental engine (or dentist drill) was in common use by dentists from the 1870’s into the 1920's. When electricity became accessible to most communities the electrically powered dental engines began to take over from the treadle power. Over the ages teeth were extracted using picks and scissors and other gouging instruments. Bow drills, hand drills and even a "bur thimble" drill were later used to prepare cavities for filling. Some drills were made bendable by attaching flexible shanks between the metal bur and the handle, giving access to the teeth at the back of the mouth. Other mechanical devices were introduced along the way, such as clockwork drills, but they were hard to handle and inefficient. Over the centuries “dentistry has been performed by priests, monks and other healers. This was followed by barbers; the barber’s chair may well have been the precursor to the dental chair. “(SA Medical Heritage Society Inc.) In 1871 James Morrison patented the first commercially manufactured 'foot treadle dental engine', the first practica dental engine although others had been introduced as early as 1790 (by John Greenwood). Handmade steel burs or drills were introduced for dental handpieces, taking advantage of the significant increase in the speed of the drill. In 1891 the first machine-made steel burs were in use. The treadle drill reduced the time to prepare a cavity from hours to less than ten minutes. In 1876 the Samuel S. White Catalogue of Dentist Instruments listed a 12 ½ inch wheel diameter dental engine, with 14 bright steel parts, for sale at US $55 In today’s market, this is the equivalent to US $1200 approx. The specifications of that dental engine are very similar to the this one in our Flagstaff Hill Maritime Village’s collection. It is interesting to note that workings of a similar treadle dentist drill were used and modified to power a treadle spinning wheel of one of the volunteer spinners at Flagstaff Hill Maritime Village. The foot treadle dental engine was a milestone in dental history. “Historic importance of treadle powered machines; they made use of human power in an optimal way” (Lowtech Magazine “Short history of early pedal powered machines”) The invention of a machine to speed up the process of excavation of a tooth lead to the invention of new burs and drills for the handpieces, improving speed and the surgical process of dentistry. They were the fore-runner of today’s electrically powered dental engines. This treadle-powered dentist drill, or dentist engine, is made of iron and steel and provides power for a mechanical dental hand-piece that would be fitted with a dental tool. The drill has a three footed cast iron base, one foot being longer than the other two. A vertical C shaped frame is joined into the centre of the base, holding an axle that has a driving-wheel (or flywheel) and connecting to a crank. A slender, shoulder height post, made from telescoping pipes, joins into the top of this frame and is height adjusted by a hand tightened screw with a round knob. On the post just above the frame is a short metal, horizontal bar (to hold the hand-piece when it is not in use). A narrow tubular arm is attached to the top of the stand at a right angle and can move up and down. At the end of the arm is a firmly fixed, flexible rubber hose protected for a short distance by a sheath of thin metal. At the end of the hose there is a fitting where the drill’s hand-piece would be attached; a small, silver coloured alligator clip is also at the end. A treadle, or foot pedal, is hinged to the heel to the long foot of the base, and joined at the toe to the crank that turns the driving-wheel. There is a spring under the toe of the treadle. The metal driving-wheel has a wide rim. Touching the inside of the rim are four tubular rings that bulge towards the outside of the driving-wheel, away from the pole, and all meet at the hub of the axle. The axle is bulbous between the inside of the driving-wheel and the frame then passes through the frame and is attached on the other side. The driving-wheel has a groove around which a belt would sit. The belt would also fit around a pulley on the arm, at the top of the post. The pulley is joined to a rod inside the arm and this spins the drill's hand-piece and dental tool holder. The two shorter feet of the base are made from a long metal bar that has been curved outwards, and its centre is bolted to the base of the pole. Under the ends of the curved legs of the base are wedge shaped feet. The driving-wheel is decorated in light coloured paint on both sides, each side having three sets of floral decals evenly spaced around them, and each about a sixth of the wheel's circumference. Similar decoration is along the sides of the frame. The foot pedal has decorative cutout patterns in the centre of the foot and at the toe. On the long foot of the stand is some lettering with a fine, light coloured border around it. The lettering is hard to read, being a dark colour and flaking off. There are also remnants of fine, light coloured flourishes. The foot pedal has lettering of the maker’s trade mark cast into the metal at the ball of the foot. Lettering on the base is peeling and difficult to read. The foot pedal has a trade mark cast into it that looks like a combination of ‘C’ , ‘S’ , ‘A’, ‘R’. flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, dentist, teeth, dental drill, dental engine, treadle drill, foot powered drill, treadle engine, orthodontics, dental surgery, james morrison -
 Flagstaff Hill Maritime Museum and Village
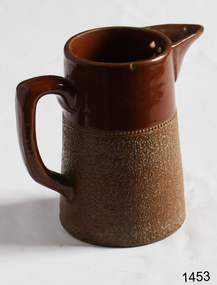
Domestic object - Jug
... Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands...Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands ...The Process of Making Pottery Decorating, Firing, Glazing, Making, Technical There is a rhythm and flow to clay. It can’t be done all at once! Even the making process! It can take weeks to get everything done, especially if you can only work on your pottery once a week! Even though we have three hour classes, it’s often just not enough time! Here is an overview of some of the processes so you have a bit more grasp on some of the technical stuff! Step One – Design There are SO many ideas out there for making stuff in clay! From delicate porcelain jewellery, through to heavy sculptural work and everything in between. Deciding your direction is sometimes not that easy – when you first start, try everything, you will naturally gravitate to the style that you enjoy! The options and variations are endless and can get a wee bit overwhelming too! Check in with me before you start to ensure your ideas will work, what order you might do things, how you could achieve the look you are seeking and any other technical data required! Step Two – Making Clay is thixotropic. This means that as you work with it, the clay first gets sloppier and wetter, before is begins to dry in the atmosphere. For most things, you simply can’t do all parts of the project at once. An example of work order might look like: Get last weeks work out from the shelves Prepare clay for today’s work – roll your clay, prepare balls for throwing, make the first stage of a pinch pot) Clean up last week’s work and put it on the shelf for bisque firing Check that you have any glazing to do – and do enough of it that you will have time to finish your main project Do the next step of your next project – there might be a further step that can’t be complete immediately, in that case, wrap your work well and put onto the shelves. Letting your work rest for a while can really help keep your work clean and professional looking. Many things require bagging under plastic to keep it ready for work the next week – put your name on the outside of the bag so you can find your work easily. We have stickers and markers. Consider how you want to decorate your work – coloured slip can be applied at a fairly wet stage (remembering that it will make your work even wetter!). Trying to apply slip to dry clay won’t work! If you want to do sgraffito – you will need to keep the work leather hard (a state of dryness where you can still work the clay with a little effort and a little water and care). Step Three – Drying Most of the time your work can go into the rack uncovered to let it dry out for the following week. If you want to continue forming or shaping you will need to double bag your work – put your work on a suitable sized bat and put the bat in a bag so the base of the bag is under the bat, then put another bag over the top of the work and tuck the top of the bag under the bat. If you want to trim (or turn) your thrown work the following week, it should also be double bagged. If your work is large, delicate, or of uneven thicknesses, you should lightly cover your work for drying. When considering the drying process, bare in mind the weather, humidity and wind! The hotter and dryer, the faster things dry and work can dry unevenly in the shelves – this can lead to cracking – another time to lightly cover your work for drying. Step Four – Trimming and Cleaning Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands – keep everything gentle and with your fingers spread as much as possible. Try to not pick up things like plates too much, and always with both hands! Before your work can be bisque fired it should be “cleaned up”. You work won’t go into the kiln if it has sharp edges – when glazed, sharp edges turn into razor blades! Use a piece of fly wire to rub the work all over – this will scratch a little so be light handed. Use a knife or metal kidney to scrape any areas that require a bit more dynamic treatment than the fly wire offers! Finally, a very light wipe over with a slightly damp sponge can help soften and soothe all of your edges and dags! Trimming thrown work: If you are planning to trim (or turn) your thrown work (and you should be), make sure you bag it well – your work should be leather hard to almost dry for easiest trimming. Use this step to finish the work completely – use a metal kidney to polish the surface, or a slightly damp sponge to give a freshly thrown look. Wipe the sponge around the rim after trimming, and check the inside of the pot for dags! Trimming slip cast work: Usually I will trim the rims of your work on the wheel the following day to make that stage easier, however you will still need to check your work for lumps and bumps. Last but not least – check that your name is still clearly on the bottom of your work. Step Five – Bisque Firing When the work is completely dry it can go into the bisque kiln. The bisque kiln is fired to 1000°C. This process burns off the water in the clay as well as some of the chemically bound water. The structure of the clay is not altered that much at this temperature. Inside the bisque kiln, the work is stacked a little, small bowl inside a larger bowl and onto a heavy plate. Smaller items like decorations or drink coasters might get stacked several high. Consideration is paid to the weight of the stack and shape of the work. A bisque kiln can fire about one and a half times the amount of work that the glaze kiln can fire. The firing takes about 10 hours to complete the cycle and about two days to cool down. Once it has been emptied the work is placed in the glaze room ready for you to decorate! Step Six – Glazing Decorating your work with colour can be a lot of fun – and time consuming! There are three main options for surface treatment at this stage: Oxide Washes Underglazes Glazes Washes and underglazes do not “glaze” the work – It will still need a layer of glaze to fully seal the clay (washes don’t need glaze on surfaces not designed for food or liquid as they can gloss up a little on their own). Underglazes are stable colourants that turn out pretty much how they look in the jar. They can be mixed with each other to form other colours and can be used like water colours to paint onto your work. Mostly they should have a clear glaze on top to seal them. Oxides are a different species – the pink oxide (cobalt) wash turns out bright blue for instance. They don’t always need a glaze on top, and some glazes can change the colour of the wash! The glazes need no other “glaze” on top! Be careful of unknown glaze interactions – you can put any combination of glaze in a bowl or on a plate, but only a single glaze on the outside of any vertical surface! Glazes are a chemical reaction under heat. We don’t know the exact chemicals in the Mayco glazes we use. I can guess by the way they interact with each other, however, on the whole, you need to test every idea you have, and not run the test on a vertical surface! Simply put, glaze is a layer of glass like substance that bonds with the clay underneath. Clay is made of silica, alumina and water. Glaze is made of mostly silica. Silica has a melting point of 1700°C and we fire to 1240°C. The silica requires a “flux” to help it melt at the lower temperature. Fluxes can be all sorts of chemicals – a common one is calcium – calcium has a melting point of 2500°C, however, together they both melt at a much lower temperature! Colourants are metal oxides like cobalt (blue), chrome (green through black), copper (green, blue, even red!), manganese (black, purple and pink) iron (red brown), etc. Different chemicals in the glaze can have dramatic effects. for example, barium carbonate (which we don’t use) turns manganese bright pink! Other elements can turn manganese dioxide brown, blue, purple and reddish brown. Manganese dioxide is a flux in and of itself as well. So, glazes that get their black and purple colours, often interact with other glazes and RUN! Our mirror black is a good example – it mixes really well with many glazes because it fluxes them – causes them to melt faster. It will also bring out many beautiful colours in the glazes because it’s black colouring most definitely comes from manganese dioxide! Glaze chemistry is a whole subject on it’s own! We use commercial Mayco glazes on purpose – for their huge range of colour possibilities, stability, cool interactions, artistic freedom with the ability to easily brush the glazes on and ease of use. We currently have almost 50 glazes on hand! A major project is to test the interactions of all glazes with each other. That is 2,500 test tiles!!!! I’m going to make the wall behind the wheels the feature wall of pretty colours! Step Seven – Glaze (Gloss or sometimes called “Glost”) Firing Most of the time this is the final stage of making your creation (but not always!) The glaze kiln goes to 1240°C. This is called cone 6, or midrange. It is the low end of stoneware temperatures. Stoneware clays and glazes are typically fired at cone 8 – 10, that is 1260 – 1290°C. The energy requirement to go from 1240°C to 1280°C is almost a 30% more! Our clay is formulated to vitrify (mature, turn “glass-like”) at 1240°, as are our glazes. A glaze kiln take around 12 hours to reach temperature and two to three days to cool down. Sometimes a third firing process is required – this is for decoration that is added to work after the glaze firing. For example – adding precious metals and lustres. this firing temperature is usually around 600 – 800°C depending upon the techniques being used. There are many students interested in gold and silver trims – we will be doing this third type of firing soon! After firing your work will be in the student finished work shelves. Remember to pay for it before you head out the door! There is a small extra charge for using porcelain clay (it’s more than twice the price of regular clay), and for any third firing process! Once your work has been fired it can not turn back into clay for millennia – so don’t fire it if you don’t like it! Put it in the bucket for recycling. https://firebirdstudios.com.au/the-process-of-making-pottery/The form of the jug has been in use for many centuries.Stoneware jug. Two tone brown glaze with pierced lip behind spout. Spout chipped.None.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, jug, ceramic jug -
 Flagstaff Hill Maritime Museum and Village
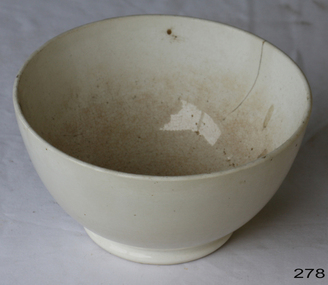
Domestic object - Bowl, Late 19th or early 20th Century
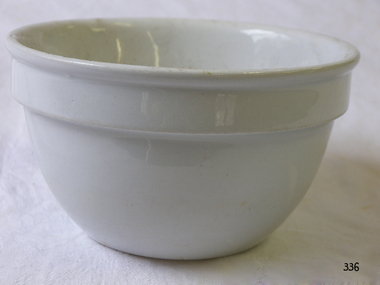
... Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands...Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands ...The Process of Making Pottery Decorating, Firing, Glazing, Making, Technical There is a rhythm and flow to clay. It can’t be done all at once! Even the making process! It can take weeks to get everything done, especially if you can only work on your pottery once a week! Even though we have three hour classes, it’s often just not enough time! Here is an overview of some of the processes so you have a bit more grasp on some of the technical stuff! Step One – Design There are SO many ideas out there for making stuff in clay! From delicate porcelain jewellery, through to heavy sculptural work and everything in between. Deciding your direction is sometimes not that easy – when you first start, try everything, you will naturally gravitate to the style that you enjoy! The options and variations are endless and can get a wee bit overwhelming too! Check in with me before you start to ensure your ideas will work, what order you might do things, how you could achieve the look you are seeking and any other technical data required! Step Two – Making Clay is thixotropic. This means that as you work with it, the clay first gets sloppier and wetter, before is begins to dry in the atmosphere. For most things, you simply can’t do all parts of the project at once. An example of work order might look like: Get last weeks work out from the shelves Prepare clay for today’s work – roll your clay, prepare balls for throwing, make the first stage of a pinch pot) Clean up last week’s work and put it on the shelf for bisque firing Check that you have any glazing to do – and do enough of it that you will have time to finish your main project Do the next step of your next project – there might be a further step that can’t be complete immediately, in that case, wrap your work well and put onto the shelves. Letting your work rest for a while can really help keep your work clean and professional looking. Many things require bagging under plastic to keep it ready for work the next week – put your name on the outside of the bag so you can find your work easily. We have stickers and markers. Consider how you want to decorate your work – coloured slip can be applied at a fairly wet stage (remembering that it will make your work even wetter!). Trying to apply slip to dry clay won’t work! If you want to do sgraffito – you will need to keep the work leather hard (a state of dryness where you can still work the clay with a little effort and a little water and care). Step Three – Drying Most of the time your work can go into the rack uncovered to let it dry out for the following week. If you want to continue forming or shaping you will need to double bag your work – put your work on a suitable sized bat and put the bat in a bag so the base of the bag is under the bat, then put another bag over the top of the work and tuck the top of the bag under the bat. If you want to trim (or turn) your thrown work the following week, it should also be double bagged. If your work is large, delicate, or of uneven thicknesses, you should lightly cover your work for drying. When considering the drying process, bare in mind the weather, humidity and wind! The hotter and dryer, the faster things dry and work can dry unevenly in the shelves – this can lead to cracking – another time to lightly cover your work for drying. Step Four – Trimming and Cleaning Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands – keep everything gentle and with your fingers spread as much as possible. Try to not pick up things like plates too much, and always with both hands! Before your work can be bisque fired it should be “cleaned up”. You work won’t go into the kiln if it has sharp edges – when glazed, sharp edges turn into razor blades! Use a piece of fly wire to rub the work all over – this will scratch a little so be light handed. Use a knife or metal kidney to scrape any areas that require a bit more dynamic treatment than the fly wire offers! Finally, a very light wipe over with a slightly damp sponge can help soften and soothe all of your edges and dags! Trimming thrown work: If you are planning to trim (or turn) your thrown work (and you should be), make sure you bag it well – your work should be leather hard to almost dry for easiest trimming. Use this step to finish the work completely – use a metal kidney to polish the surface, or a slightly damp sponge to give a freshly thrown look. Wipe the sponge around the rim after trimming, and check the inside of the pot for dags! Trimming slip cast work: Usually I will trim the rims of your work on the wheel the following day to make that stage easier, however you will still need to check your work for lumps and bumps. Last but not least – check that your name is still clearly on the bottom of your work. Step Five – Bisque Firing When the work is completely dry it can go into the bisque kiln. The bisque kiln is fired to 1000°C. This process burns off the water in the clay as well as some of the chemically bound water. The structure of the clay is not altered that much at this temperature. Inside the bisque kiln, the work is stacked a little, small bowl inside a larger bowl and onto a heavy plate. Smaller items like decorations or drink coasters might get stacked several high. Consideration is paid to the weight of the stack and shape of the work. A bisque kiln can fire about one and a half times the amount of work that the glaze kiln can fire. The firing takes about 10 hours to complete the cycle and about two days to cool down. Once it has been emptied the work is placed in the glaze room ready for you to decorate! Step Six – Glazing Decorating your work with colour can be a lot of fun – and time consuming! There are three main options for surface treatment at this stage: Oxide Washes Underglazes Glazes Washes and underglazes do not “glaze” the work – It will still need a layer of glaze to fully seal the clay (washes don’t need glaze on surfaces not designed for food or liquid as they can gloss up a little on their own). Underglazes are stable colourants that turn out pretty much how they look in the jar. They can be mixed with each other to form other colours and can be used like water colours to paint onto your work. Mostly they should have a clear glaze on top to seal them. Oxides are a different species – the pink oxide (cobalt) wash turns out bright blue for instance. They don’t always need a glaze on top, and some glazes can change the colour of the wash! The glazes need no other “glaze” on top! Be careful of unknown glaze interactions – you can put any combination of glaze in a bowl or on a plate, but only a single glaze on the outside of any vertical surface! Glazes are a chemical reaction under heat. We don’t know the exact chemicals in the Mayco glazes we use. I can guess by the way they interact with each other, however, on the whole, you need to test every idea you have, and not run the test on a vertical surface! Simply put, glaze is a layer of glass like substance that bonds with the clay underneath. Clay is made of silica, alumina and water. Glaze is made of mostly silica. Silica has a melting point of 1700°C and we fire to 1240°C. The silica requires a “flux” to help it melt at the lower temperature. Fluxes can be all sorts of chemicals – a common one is calcium – calcium has a melting point of 2500°C, however, together they both melt at a much lower temperature! Colourants are metal oxides like cobalt (blue), chrome (green through black), copper (green, blue, even red!), manganese (black, purple and pink) iron (red brown), etc. Different chemicals in the glaze can have dramatic effects. for example, barium carbonate (which we don’t use) turns manganese bright pink! Other elements can turn manganese dioxide brown, blue, purple and reddish brown. Manganese dioxide is a flux in and of itself as well. So, glazes that get their black and purple colours, often interact with other glazes and RUN! Our mirror black is a good example – it mixes really well with many glazes because it fluxes them – causes them to melt faster. It will also bring out many beautiful colours in the glazes because it’s black colouring most definitely comes from manganese dioxide! Glaze chemistry is a whole subject on it’s own! We use commercial Mayco glazes on purpose – for their huge range of colour possibilities, stability, cool interactions, artistic freedom with the ability to easily brush the glazes on and ease of use. We currently have almost 50 glazes on hand! A major project is to test the interactions of all glazes with each other. That is 2,500 test tiles!!!! I’m going to make the wall behind the wheels the feature wall of pretty colours! Step Seven – Glaze (Gloss or sometimes called “Glost”) Firing Most of the time this is the final stage of making your creation (but not always!) The glaze kiln goes to 1240°C. This is called cone 6, or midrange. It is the low end of stoneware temperatures. Stoneware clays and glazes are typically fired at cone 8 – 10, that is 1260 – 1290°C. The energy requirement to go from 1240°C to 1280°C is almost a 30% more! Our clay is formulated to vitrify (mature, turn “glass-like”) at 1240°, as are our glazes. A glaze kiln take around 12 hours to reach temperature and two to three days to cool down. Sometimes a third firing process is required – this is for decoration that is added to work after the glaze firing. For example – adding precious metals and lustres. this firing temperature is usually around 600 – 800°C depending upon the techniques being used. There are many students interested in gold and silver trims – we will be doing this third type of firing soon! After firing your work will be in the student finished work shelves. Remember to pay for it before you head out the door! There is a small extra charge for using porcelain clay (it’s more than twice the price of regular clay), and for any third firing process! Once your work has been fired it can not turn back into clay for millennia – so don’t fire it if you don’t like it! Put it in the bucket for recycling. https://firebirdstudios.com.au/the-process-of-making-pottery/ The bowl is an example of kitchenware used in the 19th century and still in use today.Bowl white ceramic. Crack on side. Badly stained.Backstamp very faint and unable to be read.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, mixing bowl, food preparation, kitchen equipment, ceramic -
 Flagstaff Hill Maritime Museum and Village
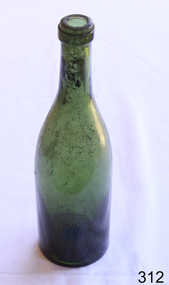
Container - Bottle, Late 19th century or early 20th century
... up to 200 bottles an hour. This process has been refined to the point where modern machines can yield more than 600 containers per minute. Blown vs. Manufactured Glass Bottles Nowadays, glass bottles, jars, and cups are usually manufactured on a bigger scale than is found in individual glassblowing studios. If we still depended on hand-blown glass for all of our glass containers, we would see some major differences in the process of creating bottles and jars. First, there's the time. Hand...up to 200 bottles an hour. This process has been refined to the point where modern machines can yield more than 600 containers per minute. Blown vs. Manufactured Glass Bottles Nowadays, glass bottles, jars, and cups are usually manufactured on a bigger scale than is found in individual glassblowing studios. If we still depended on hand-blown glass for all of our glass containers, we would see some major differences in the process of creating bottles and jars. First, there's the time. Hand ...Glass manufacturing has evolved over thousands of years. Glass making has been traced back to 3500 BC in Mesopotamia. The earliest known glass objects were beads, perhaps made by accident while working with metal. In the late Bronze Age, several civilizations discovered how to make vessels and glass bottles by wrapping threads of melted glass around cores of sand or clay. Later, moulds were used to form dishes and table wares. Around the 1st century BC, glassblowing was discovered. This made glass containers less expensive than pottery. Mould-blown glass, the process of blowing a piece of molten glass into a wooden or metal mould, was invented during the 1st century AD. This technique was faster with more consistent results. It paved the way for mass production. It wasn’t until the late 1800s that the production process to become more efficient. In 1887, a company in England created a semi-automatic process that could produce up to 200 bottles an hour. This process has been refined to the point where modern machines can yield more than 600 containers per minute. Blown vs. Manufactured Glass Bottles Nowadays, glass bottles, jars, and cups are usually manufactured on a bigger scale than is found in individual glassblowing studios. If we still depended on hand-blown glass for all of our glass containers, we would see some major differences in the process of creating bottles and jars. First, there's the time. Hand blowing glass takes a significant amount of time, even for one simple container. In contrast, hundreds of jars per minute can be made using modern technology. This leads to the second advantage: price. Because of the automated and streamlined process, the price for manufactured containers is much lower than that of hand-blown glass. Third, manufactured bottles will be much more consistently uniform than bottles blown by hand. Automated glass manufacturing produces nearly identical batches of jars. Glass blowing is awesome for unique, beautiful pieces of art. But for lots of lower priced and uniformly shaped containers, automatic manufacturing is the preferred method to create glass bottles and jars. https://www.containerandpackaging.com/resources/glass-bottles-brief-history The invention and development of glass for domestic items including bottles, has been nothing short of revolutionary. The use of glass bottles, that could be easily washed, led to improved hygiene, and mass manufacturing of drinks of all types, including milk, cordial and alcoholic beverages.Green Glass Bottle Possibly a ginger beer bottle.Concave indentation at the base. Also on base are two raised lumps. flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, glass -
 Flagstaff Hill Maritime Museum and Village
Domestic object - Bowl
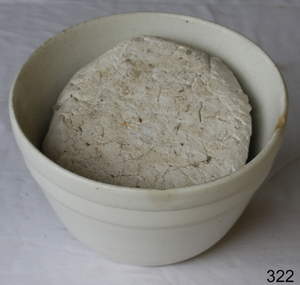
... Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands...Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands ...The Process of Making Pottery Decorating, Firing, Glazing, Making, Technical There is a rhythm and flow to clay. It can’t be done all at once! Even the making process! It can take weeks to get everything done, especially if you can only work on your pottery once a week! Even though we have three hour classes, it’s often just not enough time! Here is an overview of some of the processes so you have a bit more grasp on some of the technical stuff! Step One – Design There are SO many ideas out there for making stuff in clay! From delicate porcelain jewellery, through to heavy sculptural work and everything in between. Deciding your direction is sometimes not that easy – when you first start, try everything, you will naturally gravitate to the style that you enjoy! The options and variations are endless and can get a wee bit overwhelming too! Check in with me before you start to ensure your ideas will work, what order you might do things, how you could achieve the look you are seeking and any other technical data required! Step Two – Making Clay is thixotropic. This means that as you work with it, the clay first gets sloppier and wetter, before is begins to dry in the atmosphere. For most things, you simply can’t do all parts of the project at once. An example of work order might look like: Get last weeks work out from the shelves Prepare clay for today’s work – roll your clay, prepare balls for throwing, make the first stage of a pinch pot) Clean up last week’s work and put it on the shelf for bisque firing Check that you have any glazing to do – and do enough of it that you will have time to finish your main project Do the next step of your next project – there might be a further step that can’t be complete immediately, in that case, wrap your work well and put onto the shelves. Letting your work rest for a while can really help keep your work clean and professional looking. Many things require bagging under plastic to keep it ready for work the next week – put your name on the outside of the bag so you can find your work easily. We have stickers and markers. Consider how you want to decorate your work – coloured slip can be applied at a fairly wet stage (remembering that it will make your work even wetter!). Trying to apply slip to dry clay won’t work! If you want to do sgraffito – you will need to keep the work leather hard (a state of dryness where you can still work the clay with a little effort and a little water and care). Step Three – Drying Most of the time your work can go into the rack uncovered to let it dry out for the following week. If you want to continue forming or shaping you will need to double bag your work – put your work on a suitable sized bat and put the bat in a bag so the base of the bag is under the bat, then put another bag over the top of the work and tuck the top of the bag under the bat. If you want to trim (or turn) your thrown work the following week, it should also be double bagged. If your work is large, delicate, or of uneven thicknesses, you should lightly cover your work for drying. When considering the drying process, bare in mind the weather, humidity and wind! The hotter and dryer, the faster things dry and work can dry unevenly in the shelves – this can lead to cracking – another time to lightly cover your work for drying. Step Four – Trimming and Cleaning Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands – keep everything gentle and with your fingers spread as much as possible. Try to not pick up things like plates too much, and always with both hands! Before your work can be bisque fired it should be “cleaned up”. You work won’t go into the kiln if it has sharp edges – when glazed, sharp edges turn into razor blades! Use a piece of fly wire to rub the work all over – this will scratch a little so be light handed. Use a knife or metal kidney to scrape any areas that require a bit more dynamic treatment than the fly wire offers! Finally, a very light wipe over with a slightly damp sponge can help soften and soothe all of your edges and dags! Trimming thrown work: If you are planning to trim (or turn) your thrown work (and you should be), make sure you bag it well – your work should be leather hard to almost dry for easiest trimming. Use this step to finish the work completely – use a metal kidney to polish the surface, or a slightly damp sponge to give a freshly thrown look. Wipe the sponge around the rim after trimming, and check the inside of the pot for dags! Trimming slip cast work: Usually I will trim the rims of your work on the wheel the following day to make that stage easier, however you will still need to check your work for lumps and bumps. Last but not least – check that your name is still clearly on the bottom of your work. Step Five – Bisque Firing When the work is completely dry it can go into the bisque kiln. The bisque kiln is fired to 1000°C. This process burns off the water in the clay as well as some of the chemically bound water. The structure of the clay is not altered that much at this temperature. Inside the bisque kiln, the work is stacked a little, small bowl inside a larger bowl and onto a heavy plate. Smaller items like decorations or drink coasters might get stacked several high. Consideration is paid to the weight of the stack and shape of the work. A bisque kiln can fire about one and a half times the amount of work that the glaze kiln can fire. The firing takes about 10 hours to complete the cycle and about two days to cool down. Once it has been emptied the work is placed in the glaze room ready for you to decorate! Step Six – Glazing Decorating your work with colour can be a lot of fun – and time consuming! There are three main options for surface treatment at this stage: Oxide Washes Underglazes Glazes Washes and underglazes do not “glaze” the work – It will still need a layer of glaze to fully seal the clay (washes don’t need glaze on surfaces not designed for food or liquid as they can gloss up a little on their own). Underglazes are stable colourants that turn out pretty much how they look in the jar. They can be mixed with each other to form other colours and can be used like water colours to paint onto your work. Mostly they should have a clear glaze on top to seal them. Oxides are a different species – the pink oxide (cobalt) wash turns out bright blue for instance. They don’t always need a glaze on top, and some glazes can change the colour of the wash! The glazes need no other “glaze” on top! Be careful of unknown glaze interactions – you can put any combination of glaze in a bowl or on a plate, but only a single glaze on the outside of any vertical surface! Glazes are a chemical reaction under heat. We don’t know the exact chemicals in the Mayco glazes we use. I can guess by the way they interact with each other, however, on the whole, you need to test every idea you have, and not run the test on a vertical surface! Simply put, glaze is a layer of glass like substance that bonds with the clay underneath. Clay is made of silica, alumina and water. Glaze is made of mostly silica. Silica has a melting point of 1700°C and we fire to 1240°C. The silica requires a “flux” to help it melt at the lower temperature. Fluxes can be all sorts of chemicals – a common one is calcium – calcium has a melting point of 2500°C, however, together they both melt at a much lower temperature! Colourants are metal oxides like cobalt (blue), chrome (green through black), copper (green, blue, even red!), manganese (black, purple and pink) iron (red brown), etc. Different chemicals in the glaze can have dramatic effects. for example, barium carbonate (which we don’t use) turns manganese bright pink! Other elements can turn manganese dioxide brown, blue, purple and reddish brown. Manganese dioxide is a flux in and of itself as well. So, glazes that get their black and purple colours, often interact with other glazes and RUN! Our mirror black is a good example – it mixes really well with many glazes because it fluxes them – causes them to melt faster. It will also bring out many beautiful colours in the glazes because it’s black colouring most definitely comes from manganese dioxide! Glaze chemistry is a whole subject on it’s own! We use commercial Mayco glazes on purpose – for their huge range of colour possibilities, stability, cool interactions, artistic freedom with the ability to easily brush the glazes on and ease of use. We currently have almost 50 glazes on hand! A major project is to test the interactions of all glazes with each other. That is 2,500 test tiles!!!! I’m going to make the wall behind the wheels the feature wall of pretty colours! Step Seven – Glaze (Gloss or sometimes called “Glost”) Firing Most of the time this is the final stage of making your creation (but not always!) The glaze kiln goes to 1240°C. This is called cone 6, or midrange. It is the low end of stoneware temperatures. Stoneware clays and glazes are typically fired at cone 8 – 10, that is 1260 – 1290°C. The energy requirement to go from 1240°C to 1280°C is almost a 30% more! Our clay is formulated to vitrify (mature, turn “glass-like”) at 1240°, as are our glazes. A glaze kiln take around 12 hours to reach temperature and two to three days to cool down. Sometimes a third firing process is required – this is for decoration that is added to work after the glaze firing. For example – adding precious metals and lustres. this firing temperature is usually around 600 – 800°C depending upon the techniques being used. There are many students interested in gold and silver trims – we will be doing this third type of firing soon! After firing your work will be in the student finished work shelves. Remember to pay for it before you head out the door! There is a small extra charge for using porcelain clay (it’s more than twice the price of regular clay), and for any third firing process! Once your work has been fired it can not turn back into clay for millennia – so don’t fire it if you don’t like it! Put it in the bucket for recycling. https://firebirdstudios.com.au/the-process-of-making-pottery/ This bowl is an example of kitchenware used in the 19th century and still in use today.Bowl white ceramic plain that has two sets of edging around lip. Inside bowl has plaster designed to look like cooking mixture.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, kitchen equipment, ceramic -
 Flagstaff Hill Maritime Museum and Village
Domestic object - Bowl, J & G Meakin, Late 19th or early 20th Century
... Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands...Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands ...The Process of Making Pottery Decorating, Firing, Glazing, Making, Technical There is a rhythm and flow to clay. It can’t be done all at once! Even the making process! It can take weeks to get everything done, especially if you can only work on your pottery once a week! Even though we have three hour classes, it’s often just not enough time! Here is an overview of some of the processes so you have a bit more grasp on some of the technical stuff! Step One – Design There are SO many ideas out there for making stuff in clay! From delicate porcelain jewellery, through to heavy sculptural work and everything in between. Deciding your direction is sometimes not that easy – when you first start, try everything, you will naturally gravitate to the style that you enjoy! The options and variations are endless and can get a wee bit overwhelming too! Check in with me before you start to ensure your ideas will work, what order you might do things, how you could achieve the look you are seeking and any other technical data required! Step Two – Making Clay is thixotropic. This means that as you work with it, the clay first gets sloppier and wetter, before is begins to dry in the atmosphere. For most things, you simply can’t do all parts of the project at once. An example of work order might look like: Get last weeks work out from the shelves Prepare clay for today’s work – roll your clay, prepare balls for throwing, make the first stage of a pinch pot) Clean up last week’s work and put it on the shelf for bisque firing Check that you have any glazing to do – and do enough of it that you will have time to finish your main project Do the next step of your next project – there might be a further step that can’t be complete immediately, in that case, wrap your work well and put onto the shelves. Letting your work rest for a while can really help keep your work clean and professional looking. Many things require bagging under plastic to keep it ready for work the next week – put your name on the outside of the bag so you can find your work easily. We have stickers and markers. Consider how you want to decorate your work – coloured slip can be applied at a fairly wet stage (remembering that it will make your work even wetter!). Trying to apply slip to dry clay won’t work! If you want to do sgraffito – you will need to keep the work leather hard (a state of dryness where you can still work the clay with a little effort and a little water and care). Step Three – Drying Most of the time your work can go into the rack uncovered to let it dry out for the following week. If you want to continue forming or shaping you will need to double bag your work – put your work on a suitable sized bat and put the bat in a bag so the base of the bag is under the bat, then put another bag over the top of the work and tuck the top of the bag under the bat. If you want to trim (or turn) your thrown work the following week, it should also be double bagged. If your work is large, delicate, or of uneven thicknesses, you should lightly cover your work for drying. When considering the drying process, bare in mind the weather, humidity and wind! The hotter and dryer, the faster things dry and work can dry unevenly in the shelves – this can lead to cracking – another time to lightly cover your work for drying. Step Four – Trimming and Cleaning Up Your work is dry! It is called greenware now and it is at it’s most fragile! Handle everything with two hands. I often refer to soft hands – keep everything gentle and with your fingers spread as much as possible. Try to not pick up things like plates too much, and always with both hands! Before your work can be bisque fired it should be “cleaned up”. You work won’t go into the kiln if it has sharp edges – when glazed, sharp edges turn into razor blades! Use a piece of fly wire to rub the work all over – this will scratch a little so be light handed. Use a knife or metal kidney to scrape any areas that require a bit more dynamic treatment than the fly wire offers! Finally, a very light wipe over with a slightly damp sponge can help soften and soothe all of your edges and dags! Trimming thrown work: If you are planning to trim (or turn) your thrown work (and you should be), make sure you bag it well – your work should be leather hard to almost dry for easiest trimming. Use this step to finish the work completely – use a metal kidney to polish the surface, or a slightly damp sponge to give a freshly thrown look. Wipe the sponge around the rim after trimming, and check the inside of the pot for dags! Trimming slip cast work: Usually I will trim the rims of your work on the wheel the following day to make that stage easier, however you will still need to check your work for lumps and bumps. Last but not least – check that your name is still clearly on the bottom of your work. Step Five – Bisque Firing When the work is completely dry it can go into the bisque kiln. The bisque kiln is fired to 1000°C. This process burns off the water in the clay as well as some of the chemically bound water. The structure of the clay is not altered that much at this temperature. Inside the bisque kiln, the work is stacked a little, small bowl inside a larger bowl and onto a heavy plate. Smaller items like decorations or drink coasters might get stacked several high. Consideration is paid to the weight of the stack and shape of the work. A bisque kiln can fire about one and a half times the amount of work that the glaze kiln can fire. The firing takes about 10 hours to complete the cycle and about two days to cool down. Once it has been emptied the work is placed in the glaze room ready for you to decorate! Step Six – Glazing Decorating your work with colour can be a lot of fun – and time consuming! There are three main options for surface treatment at this stage: Oxide Washes Underglazes Glazes Washes and underglazes do not “glaze” the work – It will still need a layer of glaze to fully seal the clay (washes don’t need glaze on surfaces not designed for food or liquid as they can gloss up a little on their own). Underglazes are stable colourants that turn out pretty much how they look in the jar. They can be mixed with each other to form other colours and can be used like water colours to paint onto your work. Mostly they should have a clear glaze on top to seal them. Oxides are a different species – the pink oxide (cobalt) wash turns out bright blue for instance. They don’t always need a glaze on top, and some glazes can change the colour of the wash! The glazes need no other “glaze” on top! Be careful of unknown glaze interactions – you can put any combination of glaze in a bowl or on a plate, but only a single glaze on the outside of any vertical surface! Glazes are a chemical reaction under heat. We don’t know the exact chemicals in the Mayco glazes we use. I can guess by the way they interact with each other, however, on the whole, you need to test every idea you have, and not run the test on a vertical surface! Simply put, glaze is a layer of glass like substance that bonds with the clay underneath. Clay is made of silica, alumina and water. Glaze is made of mostly silica. Silica has a melting point of 1700°C and we fire to 1240°C. The silica requires a “flux” to help it melt at the lower temperature. Fluxes can be all sorts of chemicals – a common one is calcium – calcium has a melting point of 2500°C, however, together they both melt at a much lower temperature! Colourants are metal oxides like cobalt (blue), chrome (green through black), copper (green, blue, even red!), manganese (black, purple and pink) iron (red brown), etc. Different chemicals in the glaze can have dramatic effects. for example, barium carbonate (which we don’t use) turns manganese bright pink! Other elements can turn manganese dioxide brown, blue, purple and reddish brown. Manganese dioxide is a flux in and of itself as well. So, glazes that get their black and purple colours, often interact with other glazes and RUN! Our mirror black is a good example – it mixes really well with many glazes because it fluxes them – causes them to melt faster. It will also bring out many beautiful colours in the glazes because it’s black colouring most definitely comes from manganese dioxide! Glaze chemistry is a whole subject on it’s own! We use commercial Mayco glazes on purpose – for their huge range of colour possibilities, stability, cool interactions, artistic freedom with the ability to easily brush the glazes on and ease of use. We currently have almost 50 glazes on hand! A major project is to test the interactions of all glazes with each other. That is 2,500 test tiles!!!! I’m going to make the wall behind the wheels the feature wall of pretty colours! Step Seven – Glaze (Gloss or sometimes called “Glost”) Firing Most of the time this is the final stage of making your creation (but not always!) The glaze kiln goes to 1240°C. This is called cone 6, or midrange. It is the low end of stoneware temperatures. Stoneware clays and glazes are typically fired at cone 8 – 10, that is 1260 – 1290°C. The energy requirement to go from 1240°C to 1280°C is almost a 30% more! Our clay is formulated to vitrify (mature, turn “glass-like”) at 1240°, as are our glazes. A glaze kiln take around 12 hours to reach temperature and two to three days to cool down. Sometimes a third firing process is required – this is for decoration that is added to work after the glaze firing. For example – adding precious metals and lustres. this firing temperature is usually around 600 – 800°C depending upon the techniques being used. There are many students interested in gold and silver trims – we will be doing this third type of firing soon! After firing your work will be in the student finished work shelves. Remember to pay for it before you head out the door! There is a small extra charge for using porcelain clay (it’s more than twice the price of regular clay), and for any third firing process! Once your work has been fired it can not turn back into clay for millennia – so don’t fire it if you don’t like it! Put it in the bucket for recycling. https://firebirdstudios.com.au/the-process-of-making-pottery/This bowl was made by renowned pottery company J & G Meakin of England. The firm was established in the mid-1800's. The bowl is an example of kitchenware used in the 19th century and still in use today.Bowl; white ceramic, round and tapering inwards towards base. Made by J and G Meakin England.On base, 'Ironstone China Reg SOL 391413' with symbolflagstaff hill, flagstaff hill maritime museum and village, warrnambool, maritime museum, maritime village, great ocean road, shipwreck coast, mixing bowl, food preparation, j & g meakin, pottery, stoke-on-trent, kitchen equipment, ceramic -
 Flagstaff Hill Maritime Museum and Village
Tool - Angular Bit Stock extension, 1897-1922
... up and till 1922. The tool was manufactured from 1897 until this date and is sought out by collectors of vintage tools. flagstaff hill warrnambool flagstaff-hill flagstaff-hill-maritime-museum maritime-museum shipwreck-coast flagstaff-hill-maritime-village Tools Screw Driver Angular Hand operated Driver Tool Accessory Millers Falls Co. USA Model 109 Universal Angular hand ...Millers Falls Co. is a tool manufacturing company originally based in Millers Falls, Massachusetts. It was established in Greenfield, Massachusetts in 1868 as Gunn & Amidon by Levi J. Gunn and Charles H. Amidon. Gunn and Amidon, along with a third partner, Henry L. Pratt built a factory in the north of Greenfield. After the Greenfield factory burned down, the company was reorganized as the Millers Falls Manufacturing Co. It merged with Backus Vise Co. in 1872 to form the Millers Falls Co. In 1931 Millers Falls tools purchased the majority of the shares of Goodell-Pratt tools and merged with that manufacturer in 1932.In 1962 the company was acquired by Ingersoll Rand. In 1982, Ingersoll Rand sold the Millers Falls business to the newly created Millers Falls Tool Co. The company was head quartered in Alpha, New Jersey. Since 2002 the company trademark has belonged to Hangzhou Great Star Industrial Co., Ltd, of Hangzhou, China.An interesting an unusual tool made by the Millers Falls Tool company that continued to be featured in it’s catalogue up and till 1922. The tool was manufactured from 1897 until this date and is sought out by collectors of vintage tools.Universal Angular hand operated bit stock with spring type alligator jaws, main casting is Japanned bright parts are nickel plated item used with a bit & brace as an extension or angular borer. Millers Falls Co. USA Model 109flagstaff hill, warrnambool, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, tools, screw driver, angular hand operated driver, tool accessory -
 Flagstaff Hill Maritime Museum and Village
Tool - Complex Wood Plane, Late 19th to Early 20th century
... hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up...hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up ...A moulding plane is a specialised plane used for making the complex shapes found in wooden mouldings that are used to decorate furniture or other wooden objects. Traditionally, moulding planes were blocks of wear-resistant hardwood, often beech or maple, which were worked to the shape of the intended moulding. The blade or iron was likewise formed to the intended moulding profile and secured in the body of the plane with a wooden wedge. A traditional cabinetmakers shop might have many, perhaps hundreds, of moulding planes for the full range of work to be performed. Large crown mouldings required planes of six or more inches in width, which demanded great strength to push and often had additional peg handles on the sides, allowing the craftsman's apprentice or other workers to pull the plane ahead of the master who guided it. Company History: The firm of Alexander Mathieson & Sons was one of the leading makers of hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up his plane-making workshop on Saracen Lane off the Gallowgate in the heart of Glasgow, not far from the Saracen's Head Inn, where Dr Johnson and James Boswell had stayed on their tour of Scotland in 1773. Alexander Mathieson (1797–1851) is recorded in 1822 as a plane-maker at 25 Gallowgate, but in the following year at 14 Saracen's Lane, presumably having taken over the premises of John Manners. The 1841 national census described Alexander Mathieson as a master plane-maker at 38 Saracen Lane with his son Thomas Adam working as a journeyman plane-maker. In 1849 the firm of James & William Stewart at 65 Nicolson Street, Edinburgh was taken over and Thomas was put in charge of the business, trading under the name Thomas A. Mathieson & Co. as plane and edge-tool makers. Thomas's company acquired the Edinburgh edge-tool makers Charles & Hugh McPherson and took over their premises in Gilmore Street. The Edinburgh directory of 1856/7 the business is recorded as being Alexander Mathieson & Son, plane and edge-tool makers at 48 Nicolson Street and Paul's Work, Gilmore Street. The 1851 census records indicate that Alexander was working as a tool and plane-maker employing eight men. Later that year Alexander died and his son Thomas took over the business. Under the heading of an edge-tool maker in the 1852/3 (Post-Office Glasgow Annual Directory) the firm is now listed as Alexander Mathieson & Son. By the early 1850s, the business had moved to 24 Saracen Lane. The directory for 1857/8 records that the firm had moved again only a few years later to East Campbell Street, also off the Gallowgate, and that through further diversification was also manufacturing coopers' and tinmen's tools. The ten-yearly censuses log the firm's growth and in 1861 Thomas was a tool manufacturer employing 95 men and 30 boys; in 1871 he had 200 men working for him and in 1881 300 men. By 1899 the firm had been incorporated as Alexander Mathieson & Sons Ltd, even though only Alexander's son Thomas appears ever to have joined the firm. A vintage tool made by a well-known firm made for other firms and individuals that worked in wood. The tool was used before routers and spindle moulders came into use after World War ll, a time when to produce a decorative moulding for a piece of furniture or other items this had to be accomplished by hand using one of these types of planes. A significant item from the mid to late 19th century that today is quite rare and sought after by collectors. It gives us a snapshot of how furniture was made predominately by hand and with tools that were themselves hand made shows the craftsmanship used to make such a unique item. Ogee Complex Moulding Plane Alex Mathieson & Son. Stamped W Worrel, (owner) & No 2.flagstaff hill, warrnambool, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, alexander mathieson & sons, complex moulding plane, carpenders tools, cabinet makers tools, wood working tools, wood planes -
 Flagstaff Hill Maritime Museum and Village
Tool - Spokeshave, Mathieson and Son, 1860 to 1910
... hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up...hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up ...A spokeshave is a hand tool used to shape and smooth woods in woodworking jobs such as making cart wheel spokes, chair legs, paddles, bows, and arrows. The tool consists of a blade fixed into the body of the tool, which has a handle for each hand. Historically, a spokeshave was made with a wooden body and metal cutting blade. With industrialization metal bodies displaced wood in mass-produced tools. Being a small tool, spokeshaves are not suited to working large surfaces. The name spokeshave dates back to at least the 16th century, though the early history of the tool is not well documented. The name spokeshave reflects the early use of the tool by wheel wrights. The first spokeshaves were made of wood usually beech with steel blades, before being largely superseded by the development of metal-bodied spokeshaves in the latter half of the 19th century, though many woodworkers still use wooden spokeshaves. Due to their widespread use and versatility vintage wooden spokeshaves remain commonly available and relatively low in price. Spokeshaves consist of a blade or iron secured to the body or stock of the tool, which has two handles – one for each hand. The bottom surface of the tool is called the sole. The blade can be removed for sharpening, and adjusted to vary the depth of the cut. An early design consisted of a metal blade with a pair of tangs to which the wooden handles were attached, as with a draw knife. Unlike a draw knife, but like a plane, spokeshaves typically have a sole plate that fixes the angle of the blade relative to the surface being worked. There are a wide variety of different types of spokeshave, suited to different trades and applications. Company History: The firm of Alexander Mathieson & Sons was one of the leading makers of hand tools in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperage's and other industries, both locally and far and wide. The year 1792 was deemed by the firm to be that of its foundation it was in all likelihood the year in which John Manners had set up his plane-making workshop on Saracen Lane off the Gallowgate in the heart of Glasgow, not far from the Saracen's Head Inn, where Dr Johnson and James Boswell had stayed on their tour of Scotland in 1773. Alexander Mathieson (1797–1851) is recorded in 1822 as a plane-maker at 25 Gallowgate, but in the following year at 14 Saracen's Lane, presumably having taken over the premises of John Manners. The 1841 national census described Alexander Mathieson as a master plane-maker at 38 Saracen Lane with his son Thomas Adam working as a journeyman plane-maker. In 1849 the firm of James & William Stewart at 65 Nicolson Street, Edinburgh was taken over and Thomas was put in charge of the business, trading under the name Thomas A. Mathieson & Co. as plane and edge-tool makers. Thomas's company acquired the Edinburgh edge-tool makers Charles & Hugh McPherson and took over their premises in Gilmore Street. The Edinburgh directory of 1856/7 the business is recorded as being Alexander Mathieson & Son, plane and edge-tool makers at 48 Nicolson Street and Paul's Work, Gilmore Street. The 1851 census records indicate that Alexander was working as a tool and plane-maker employing eight men. Later that year Alexander died and his son Thomas took over the business. Under the heading of an edge-tool maker in the 1852/3 (Post-Office Glasgow Annual Directory) the firm is now listed as Alexander Mathieson & Son. By the early 1850s, the business had moved to 24 Saracen Lane. The directory for 1857/8 records that the firm had moved again only a few years later to East Campbell Street, also off the Gallowgate, and that through further diversification was also manufacturing coopers' and tin men's tools. The ten-yearly censuses log the firm's growth and in 1861 Thomas was a tool manufacturer employing 95 men and 30 boys; in 1871 he had 200 men working for him and in 1881 300 men. By 1899 the firm had been incorporated as Alexander Mathieson & Sons Ltd, even though only Alexander's son Thomas appears ever to have joined the firm.A vintage tool made by a well-known firm made for other firms and individuals that worked in wood. The tool was used to shape various items mainly in use by wheel wrights. A significant vintage item from the mid to late 19th century that today is quite sought after by collectors. It gives us a snapshot of how trade people predominately worked materials such as wood by hand and with tools that were themselves hand made shows the craftsman's art of the time. Spokeshave with blade 4 inches wide.Mathieson and Son Glasgow. flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, spokeshave, mathieson and son, carpentry tools, wheel wright tools -
 Flagstaff Hill Maritime Museum and Village
Tool - Setting Hammer, Vaughan & Bushnell Mfg. Co, Mid-20th Century
... up a blacksmith shop in a room behind a hardware store owned by Sidney Bushnell. On June 15, 1869, Alexander was granted U.S. Patent No. 91,387 for his Improved Post Auger. Customer satisfaction with Vaughan post augers led to requests for other hand tools, and Alexander soon found himself in the custom tool business. Since that time, Vaughan has been transformed from a small maker of hand...up a blacksmith shop in a room behind a hardware store owned by Sidney Bushnell. On June 15, 1869, Alexander was granted U.S. Patent No. 91,387 for his Improved Post Auger. Customer satisfaction with Vaughan post augers led to requests for other hand tools, and Alexander soon found himself in the custom tool business. Since that time, Vaughan has been transformed from a small maker of hand ...The company Vaughan & Bushnell Mfg. Co. was founded in Peoria, Illinois, by Alexander Vaughan. It began as a plumbing business, which in those days consisted of digging wells and piping water into the kitchens of the local citizenry. Alexander's business prospered, but the inventive, 18-year-old blacksmith had his eye on bigger things. Alexander had an idea for improving the design of the augers used for digging fencing post holes. He turned this idea into reality, and believing that Chicago would outstrip Peoria as a business centre, moved to the Windy City. He set up a blacksmith shop in a room behind a hardware store owned by Sidney Bushnell. On June 15, 1869, Alexander was granted U.S. Patent No. 91,387 for his Improved Post Auger. Customer satisfaction with Vaughan post augers led to requests for other hand tools, and Alexander soon found himself in the custom tool business. Since that time, Vaughan has been transformed from a small maker of hand tools to one of the world's largest manufacturers of striking tools that today are still producing quality tools for the world's markets.Vaugahn & Co. was a significant USA company that became the leader in the manufacture of striking tools that have been exported all over the world. Hammer: tinner's setting or pairing hammer. The head has a square poll and a wedge. Stamped with the inscription. Manufactured in the UK by Vaughan. Stamped "Vaughan "flagstaff hill, warrnambool, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, hammer, setting hammer, tinners hammer, tool, striking tool, alexander vaughan, vaughan & bushnell mfg. co, tinner's pairing hammer, tinner's setting hammer, pairing hammer, tin smith, metal work, metal work equipment, vaughan -
 Mission to Seafarers Victoria
Painting - Oil painting, Madeline M.Ravenna Lewellin, Start Point Light, Devonshire, 1875
... up of stormy grey clouds. A rocky cliff face can be seen on the right-hand side of the painting. A small church can be seen on the hillside. The ship on the left third of the painting sits on the horizon line of the sea. The centre ship with two masts appears to be leaning to the right and its deck is exposed to the viewer showing four men attempting to handle the masts and rigging. The left-hand...up of stormy grey clouds. A rocky cliff face can be seen on the right-hand side of the painting. A small church can be seen on the hillside. The ship on the left third of the painting sits on the horizon line of the sea. The centre ship with two masts appears to be leaning to the right and its deck is exposed to the viewer showing four men attempting to handle the masts and rigging. The left-hand ...This painting was made after an artwork by Wilhelm Melby held at the National Gallery of Victoria. Melby is a Danish artist (1824-1882). It depicts a famous Devonshire coastal region famous now for its lighthouse and the pick up point for the pilot when entering waters approaching Dartmouth. The sailing vessels pre-date the construction of the famous lighthouse. Over the centuries the view would have been familiar to many sailors as they left or approached the English mainland and south coast ports in the English Channel. Madeline Mary Ravenna Lewellin (1854 – 24 November 1944) was born in Victoria to Dr John Henry Hill Lewellin, a physician, and Grace Elizabeth (née Danneby). She was one of five daughters, and the family lived in Prahran. Lewellin's brother, Captain Herbert Gordon Hill Lewellin, was a commander in the P. and O. fleet (apprentice on the Romanoff, Lieutenant RNR on the HMS Arethusa in 1899, RMS Mongolia in 1913 sunk in 1917, Naldera in 1920). She studied painting at the National Gallery School in 1879 under Eugene von Guerard. She's also known for collecting and painting specimens, and became a member of the Field Naturalists Club of Victoria in 1885. In 1884 she won a silver medal for her studies of fungi. She collected plants for Australian botanist Ferdinand von Mueller, and the variety of Dicrastylis lewellinii (Purple sand-sage) is named after her. Miss Lewellin, who had a love of the sea and ships as subject matter is listed in 1910 as a donor as a 10/6 member donating to the motor launch fund and in 1918 as a working member of the Ladies Harbour Lights Guild which involved regular volunteer shifts at the Mission to Seamen on canteen and other duties. The painting was donated by Miss Lewellin in 1918 and hanged above the stage in the main hall; it appears on several postcards of the time.Marine art, Maritime artThis oil painting has a dark polished wood and gold leaf slip. The painting depicts two masted boats. The choppy sea takes up the lower-third of the painting, and the other two-thirds of the image of made up of stormy grey clouds. A rocky cliff face can be seen on the right-hand side of the painting. A small church can be seen on the hillside. The ship on the left third of the painting sits on the horizon line of the sea. The centre ship with two masts appears to be leaning to the right and its deck is exposed to the viewer showing four men attempting to handle the masts and rigging. The left-hand ship with three masts is surrounded by two grey distant silhouetted mast ships. There are three seagulls at the upper left-centre of the image. There are another three gulls down on the lower-left of the image. Front: ENGRAVED PLAQUE: Start Point Light. Devonshire. SIGNATURE: After W. Melby / M.M.R Lewellin. 1875. Reverse: IN BLACK MARKER PEN: * Hang from two points * WHITE STICKER WITH CONSERVATOR DETAILS: Art Conservation Frames / 118 Bridport Street, Albert Park, VIC, 3206 / 9696 9066 / artconservationframers.com.aupainting, ships, mast, church, sea, storm, oil painting, seagulls, madeline r. lewellin, artwork-paintings, ngv, wilhelm melby, eugene von guerard, botanist, rms mongolia, captain herbert gordon hill lewellin (1862-1935), paddy lewellin, reproduction, seascape, danger -
 Mission to Seafarers Victoria
Plaque - Wall Plaque, Lightkeepers of the Mission to Seamen, c.1950
... The Lightkeepers Auxiliary was also active with the Mission in Williamstown where they helped raised the funds to set up the new mission in the E,S & A Bank in 1943 which was furnished thanks to the High Commission of Canada. wooden platter mission flags nora o'connor lightkeepers' auxiliary lightkeeper overseas missions vancouver canada british columbia mission to seamen indigo ink stamp : hand painted (1st word almost indecipherable) Circular , varnished wooden tray or plaque with beaded edge froming 'lip". Oval hand ...Original owner Nora O’Connor the donor’s adopted aunt, migrated to Canada during WW2 and also worked as volunteer at the Vancouver Mission to Seamen where she met her husband Edward O’Connor who later migrated to Australia. NB Lightkeeper membership category across many of the Missions globally, was usually reserved for women busy as home-makers with children and also as a Junior membership category for children.The platter was accompanied by other materials from the Vancouver club of Senior Light keepers and together the material provides a parallel insight and reference to this group. It also provides a historical link within the worldwide network that is now recognised as the Mission to Seafarers. The Lightkeepers Auxiliary was also active with the Mission in Williamstown where they helped raised the funds to set up the new mission in the E,S & A Bank in 1943 which was furnished thanks to the High Commission of Canada.Circular , varnished wooden tray or plaque with beaded edge froming 'lip". Oval hand painted design of two flags on flag pole, one yellow hoist above blue flag with horizontal white stripe across centre, on a ground of turquoise green. U.C. Lettering in gilt around edge of design (see title). On verso, ink stamp plus an old hanging metal wire.indigo ink stamp : hand painted (1st word almost indecipherable)wooden platter, mission flags, nora o'connor, lightkeepers' auxiliary, lightkeeper, overseas missions, vancouver, canada, british columbia, mission to seamen -
 Federation University Historical Collection
Document - Correspondence, Richard Squire Mining Correspondence
... Included was a one page letter from Ned to Mr Squire with an information on the progress at the tunnel and with the information that his hands were cracked so badly that he was wearing two socks on each hand, dated Saturday. .137) A one page letter which family news and a paragraph about the figures in his calculations, dated 21/10/33. On the back side was a letter from E Squire (his wife) to Tom, Hazel & boys again with family and personal information, dated 22nd 10/33. .138) A three page letter with the disappointing news that the English consortium would not take up the option on the Mt Mercer lease and gave his opinion that it was self interest that stopped it going ahead. ...Included was a one page letter from Ned to Mr Squire with an information on the progress at the tunnel and with the information that his hands were cracked so badly that he was wearing two socks on each hand, dated Saturday. .137) A one page letter which family news and a paragraph about the figures in his calculations, dated 21/10/33. On the back side was a letter from E Squire (his wife) to Tom, Hazel & boys again with family and personal information, dated 22nd 10/33. .138) A three page letter with the disappointing news that the English consortium would not take up the option on the Mt Mercer lease and gave his opinion that it was self interest that stopped it going ahead. ...Seems that Tom pays Ned's wages. Numerous bores were sunk , some were opened out and driven in the direction of the reef. Numerous Cross cuts were also made from the main tunnel.Unless otherwise stated the letters are from Dad (Richard Squire) to Tom, Hazel & Kiddies all. .1) Handwritten two page letter from Richard Squire to 'Tom & Hazel & little men' with information regarding the Leigh River Tunnel at Mount Mercer, dated 6/8/28. .2) Handwritten three page letter with information regarding mining operations dated 27.6.29. .3) Handwritten three page letter from Richard Squire to 'Tom & Hazel & Flock' with queries regarding the health of one of their children, other personal information and information regarding mining operations dated 18/7/29. .4) Handwritten one page letter from Richard Squire to 'Tom' dated 20/7/29, regarding the enclosed handwritten receipt with stamp for Call of two shares costing 8 pounds 7 shillings and 2 pence in Leigh River Tunnel Syndicate from Richard Squire dated 13th July 1927. .5) Handwritten two page letter from Richard Squire to 'Tom & Hazel & Pinchers' regarding his health, other personal information and information about the four page report of position of work at 'Leigh River Tunnel' enclosed. The letter is dated 29/11/29 and the report dated Nov 28th 29. .6) Handwritten two page letter with personal information and a suggestion that Tom learn to swim dated 13th Jan 30. .7) Handwritten two page report by Richard Squire regarding Leigh River Tunnel Syndicate plus a one page 'Rough Section' drawing of the tunnel dated 29th April 1930. .8) Typed one page report by Richard Squire regarding Leigh River Tunnel Syndicate and the findings of a new shaft dated 9th December 30. .9) Handwritten one page letter by Richard Squire to 'Tom' regarding mining operations and four handwritten receipts for payment of Calls from Richard Squire and Mr H McLeod and Mr E McLeod with stamps. .10) Handwritten two page letter regarding a meeting he had with the Secretary for Mines, Mr Whitehead dated 22 Feb 1931. .11) Handwritten two page letter regarding the difficulties in financing the mining operation occasioned by the interference of the government department dated 12th Mar 31. .12) Handwritten one page letter regarding the delay in the submission of his letter to the Gold Committee and with details of plans he had sent to Tom separately, dated 1st April 31. .13) Handwritten two page letter by Richard Squire to 'Tom' regarding personal matters including his health and also information regarding Tunnel work, dated May 11th 31. .14) Handwritten two page letter regarding the mine work, how his new employee, Ned, was going and also his health, dated Thur 21st May 31. .15) Handwritten two page letter regarding the Tunnel progress and financial matters dated Tue 26th May. .16) Handwritten three page letter regarding the Tunnel progress dated Thur June 11th. .17) Handwritten two page letter regarding the Tunnel progress, an issue relating to Ned's taxation assessment and his own health, dated 28th June 31. .18) Handwritten three page letter with detailed information on the Tunnel progress and information regarding his health, dated Thur July 23rd. .19) Handwritten two page letter regarding the Tunnel progress and some personal greetings, dated Thur July 30th 31. .20) Handwritten two page letter regarding the Tunnel progress, an agreement with Messrs Read & Peers? and a renaming of a Prospect as Lawaluk instead of Mount Mercer, dated Sun 2nd Aug 31. .21) Handwritten three page letter regarding the Tunnel progress, the lease agreement on Mr Read's property at Mount Mercer which he had been unable to pay and a parsley root remedy which a Ballarat Chinese herbalist had prescribed for his catarrh and had been effective, dated Thur 13th Aug 31. .22) Handwritten two page letter regarding the efficacy of the parsley (root) water in healing his catarrh and detailed progress report on the Tunnel which showed a little gold in the uncovered 'wash', dated Mon 24th Aug. .23) Handwritten three page letter regarding the progress of the Tunnel and one of the bores sunk also mentions his health, dated Mon Sept 7th. .24) Handwritten three page letter regarding the Tunnel progress in detail and an account of his illness, dated Thur 24th Sept. .25) Handwritten two page letter regarding the Tunnel progress in detail and his health which had been poor, dated Thur Oct 8th 31. .26) Handwritten four page letter regarding the Tunnel progress in detail, dated Thur Oct 22. .27) Handwritten four page letter regarding a detailed report of the Tunnel progress including the news of some show of gold and other personal matters including advising Tom not to drive there when he would have to drive home in the dark because of the accidents caused by 'Boosy Drivers', dated Thur Nov 19th 31. .28) Handwritten two page letter regarding the continued promising Tunnel progress, dated Thur Nov 26th. .29) Handwritten two page letter regarding Tunnel progress and personal matters relating to the coming Christmas visit, dated Thur Dec 3rd 1931. .30) Handwritten two page letter regarding Tunnel progress and personal matters regarding the impending visit by the family, dated Sun Dec 6th 31. .31) Handwritten two page letter regarding his health and the treatment proscribed by a Chinese herbalist and also some information about his expenses, dated Sunday 25/1/32. .32) Handwritten four page letter regarding Tunnel progress including a small diagram and further information on his health, dated Thur 25th Feb 32. .33) Handwritten three page letter regarding Tunnel progress and some personal and family information, dated Mon 21st 32. .34) Handwritten one page letter regarding some personal matters and information about the Tunnel progress, dated Thus 31st Mar. .35) Handwritten two page letter regarding detailed information about the Tunnel as well as a one page diagram of the Drives being excavated, dated Sun night 3rd April. .36). Handwritten three page letter from his home in Prahran regarding a mixture of personal matters and matters relating to the Tunnel, dated 18/4/32. .37) Handwritten one page letter regarding enclosed three shares which were to be placed as he was very short of funds, dated 19-4-32. .38) Handwritten two page letter from his home in Prahran regarding work carried out by Ned at the Tunnel and family matters, dated 6/5/32. .39) Handwritten one page letter from his home in Prahran regarding work carried out by Ned at the Tunnel, dated 10/5/32 plus an attached one page letter written by Ned (E. Woodlook) to 'Mr Squire' regarding regarding Tunnel progress, dated Saturday. .40) Handwritten two page letter from his home in Prahran regarding Tunnel progress and some personal matters, dated 27/5/32 plus an attached one page letter written by Ned to 'Mr Squire' regarding Tunnel progress and with the information that the rats were bad in Richard's hut, dated Friday. .41) Handwritten two page letter from his home in Prahran regarding Tunnel progress, dated 3/6/32 plus a two page letter written by E.Woodlock to 'Mr Squire' regarding Tunnel progress as well as person matters regarding his health, dated Friday (27th May 32 written in pencil by Richard). .42) Handwritten three page letter from his home in Prahran regarding tunnel progress and financial matters, also detailed information about the Madison's Tunnel, dated 8/6/32, plus a one page letter from E. Woodlock (Ned) to 'Mr Squire' regarding Tunnel progress dated Saturday (4 June, 32). .43) Handwritten three page letter from his home Prahran regarding a sketch he had made of Madison's Tunnel and the Mercer Shaft (not present) and the similarity of other mines with barely Payable gold, dated 13/6/32. plus a one page letter from E. Woodlock to 'Mr Squire' regarding Tunnel progress dated Saturday. .44) Handwritten one page letter by Richard Squire to 'Tom' from his home in Prahran with some personal information as well as the hope to return to Mt Mercer as he felt he was now well, not dated, plus a two page letter from E. Woodlock to 'Mr Squire' regarding duty stamps sent and Tunnel progress dated Saturday. .45) Handwritten two page letter from his home in Prahran regarding the progress of the Tunnel, dated 21/6/32, plus a one page letter from E. Woodlock regarding the progress of the Tunnel work, dated Monday (20/6/32). .46) Handwritten three page letter from his home in Prahran regarding the price of gold and the effect that mining Payable gold in the Madison Tunnel could have, dated 27/6/32. .47) Handwritten three page letter by Richard Squire to Tom, Hazel & Kiddies all' from his home in Prahran regarding his thoughts on the Madison Tunnel at Piggoreet, dated Mon 4th July 32, plus two one page letters by E Woodlock to 'Mr Squire' regarding the Tunnel work and more personal things, dated Wednesday (June 29th 32) and Saturday (July 2nd). .48) Handwritten two page letter from his home in Prahran regarding his intention to return to the diggings in a small car procured for his use and his intention to re-peg the Leigh River Lease in another name, dated Sun 17/7/32, plus a two page and a one page letter by E Woodlock to 'Mr Squire' regarding progress at the Tunnel dated Thursday (7th July) and Tuesday (12th July 32). .49) Handwritten one page letter by E Woodlock to Mr Squire detailing the tunnel work and other work related details dated Saturday (16th July 32), plus a one page letter by 'Dad' (Richard Squire) to 'Tom, Hazel & Kiddies all' regarding the letter sent by Ned (E Woodlock) and the ongoing work. He also talks about the health of Mam, his wife, dated 19th July 32. .50) Handwritten one page letter regarding the work at the tunnel and with the information that he was to finally return to the mine, dated 22/7/32, plus a one page letter by E Woodlock to Mr Squire about the ongoing work, dated Wednesday (20th July). .51) Handwritten two page letter written from Mt Mercer, regarding the works in the Mt Mercer Tunnel (mentioning South Cockloft). He also details that the drive from town (Melbourne) took 4 gallons of petrol, dated Thur 28th July 32. .52) Handwritten 3 page letter detailing the work carried on at the tunnels and with the information that underground gas had halted work temporarily. He was keen that Tom should visit one weekend soon, dated Sat 6th Aug 1932. .53) Handwritten four page letter detailing the work and new bore holes near Madisons Tunnel. The No 1 tunnel work had to be suspended due to continued gas filling the diggings every time the barometric pressure dropped. On the last page was a rough sketch of the area which was being worked, dated 19th Aug 32. .54) Handwritten two page letter regarding Tom's proposed visit to the site and some plans that he should bring with him. He also spoke of a pup that he was housing till Tom came, dated 21/8/32. .55) Handwritten one page letter encouraging Tom to bring skid chains for his vehicle as the road was muddy when he came on the weekend. He gave a brief account of the work and of the pup's progress, dated 25/8/32 .56) Handwritten three page letter regarding the weather and the relief he felt at knowing Tom and his companions had arrived safely home. He also thanked Tom for the cheques for Ned and detailed a little of the work at the tunnel and the need for more explosives as well as the fact that they had had to put a lock on the door of the hut to stop intruders, dated Sun Sept 4th 32. .57) Handwritten one page letter regarding the ongoing work at the tunnel, dated Thur Sept 8/32. .58) Handwritten two page letter written from Prahran, regarding his trip home, work at the tunnel and with information about the enclosed receipts, dated 16/9/32. Also included was a one page letter from E Woodlock to Mr Squire regarding the work at the tunnel, dated Wednesday. .59) Handwritten one page letter from Dad (Richard Squire) to 'Tom, Hazel & Kiddies all' written from Mt Mercer, regarding the work at the tunnel and the effect that 2 inches of rain had on the work, dated Wed Sept 20th 32. .60) Handwritten two page letter regarding the work at the tunnel and with the information that Mr Read who owned the property where the tunnel was located, had a serious accident in Melbourne, dated Thur 29th Sept 30 (this 1930 date is a mistake as the information contained in this letter follows on from his previous letter dated 20th Sept 32). .61) Handwritten one page letter regarding the work at the tunnel with the encouraging information that flecks of gold were found in about half a dish (mining pan), dated Thur Sept 22nd. .62) Handwritten two page letter regarding the progress at the tunnel and the difficulties of the work and thanks for Ned's cheque. Also mentioned was the information that Mr Read had a fractured pelvis and would be in hospital for two months, so Mrs Read with her father was looking after the shearing, dated Thur 6th Oct. .63) Handwritten two page letter with a third page of a diagram of a cross section of the Leigh River Tunnel, including the new tunnel and Madisons tunnel, with detailed description of the work in the tunnel, dated Sat 8th Oct. .64) Handwritten two page letter written from Prahran, giving detailed information of the tunnel and the expected outcome of the work. He also commented that he was to visit Mr Read in hospital, dated 14/10/32. .65) Handwritten two page letter written from Mt Mercer, giving information about the work in the tunnel and his visit to Mr Read, dated Wed 19th Oct. Enclosed also was a one page letter from E Woodlock to Mr Squire giving an account of his work in the tunnel, dated Thursday. .66) Handwritten one page letter regarding the work in the tunnel, dated Sun Oct 23/32. .67) Handwritten two page letter from Dad & Jim (Richard Squire) to 'Tom, Hazel & Kiddies all' regarding the receipt of Ned's wages cheque and the insurance of Ned's person as well as a detailed description of the tunnel and its relationship to Madisons Tunnel. He also gives some indication of his health, dated Tue Nov 1st 32. .68) Handwritten on page letter written from Prahran, giving a small amount of information about the tunnel work as well as his visit to see Mr Read and some personal information, undated. Enclosed also is a one page letter by E Woodlock to Mr Squire about the work in the tunnel, dated Thursday. .69) Handwritten one page letter with little information, dated 11/11/32. Also enclosed is a one page letter from E Woodlock to Mr Squire about the work in the tunnel, dated Thursday. .70) Handwritten three page letter with detailed information about the tunnel work and an aside about Jim's help and the he suffered from "Imaginitis imagines he sees a speck of gold in every bit of gravel met", dated 10/11/32. .71) Handwritten two page letter with detailed information on the work as their tunnel crossed with the old Madison Tunnel, dated Thur 17th Nov. .72) Handwritten three page letter detailing information on an application for a 500 acre lease which was posted at the Grenville Post Office and how it would impact on their lease. The upshot was that their leases would need to be re-pegged and the fee to publish a Notice of Application on their Leigh River claim was necessary to pay and he wondered if one of their investors would pay the 10 pounds necessary to secure the claim. He also spoke of perhaps forming a Company to put a plant on their Mt Mercer shaft as he felt that the gold would be of a payable quantity, dated Sunday 20th Nov, Also included was a note written by Ned (Edward Woodlock) who had copied the Notice of Application. .73) Handwritten two page letter detailing information found in Madison's Tunnel as it related to their own tunnels, particularly No 2 tunnel and how far he felt he would need to tunnel to reach an improvement in the 'wash', dated Thur 24th Nov. .74) Handwritten one page letter thanking him for the cheque the investor, Mr Wilkinson had provided for the Notice of Application for the Mt Mercer old Lease of 828 acres. He also gave some information about how it was originally farm labourers who only worked this lease and only when they had no other work. He also gave some personal information about Mam's birthday, dated Mon Nov 28th 32. .75) Handwritten two page letter by Dad (Richard Squire) to 'Tom, Hazel & Kiddies 3' written from Prahran, telling them that they had received Ned Cheque and that that Jim and He had come home. He also detailed an incident that Jim had had with a tyre blowout whilst on his way to get explosives and post the Notice of Application in the Warden's Office in Ballarat. The stub axle had bent and Jim had to ride a bike to get a new one and after changing the inner tube of the tyre they were able to drive back to Melbourne and were in the process on having the tyre re-treaded, dated 6/12/32. .76) Handwritten one page letter explaining how he and Mam had contracted colds and that his kidneys had some of their of trouble. He hoped to return to Mt Mercer on the weekend, dated 18th Jan 33. Also included was a handwritten two page letter by E Woodlock to Mr Squire giving information about the tunnel work, an injury to his hand and the fact that he had only 3 picks that were any good. He also asked for some vegetables, tomatoes and bacon when Richard returned, dated Saturday. .77) Handwritten one page letter written from Mt Mercer, giving information about the tunnel work, now 97'6" in and how he had expected to have already come upon the Madison's gold bearing gravel wash, dated Wed 25th Jan 33. .78) Handwritten two page letter with detailed information about how the tunnel had cut across a second Madison's tunnel and the prospects in this tunnel looked more promising. He also stated that he had not been well the last few days, dated Frid 27th 33 .79) Handwritten one page letter with information about the shotty gold found and the tunnel work and that he would test the value of the wash where the gold was found, dated Mon 30th Jan. .80) Handwritten short note of one page giving sketchy information about the tunnel work, dated Tue 31st Jan 33. .81) Handwritten two page letter giving information about his dealings with the Secretary for Mines relating to the fact that because the application for lease was identical to the old lease, they therefore should not need to pay for a full survey costing 7 pounds, just an inspection. He also detailed the workings and asks for more parsley roots to be sent to him, dated Thur Feb 9th 33. .82) Handwritten one page letter stating that he had received Ned's cheque and information about the workings, the coarse gold found and the fact they were going home for fresh food, dated Tue 14th 33. .83) Handwritten two page letter giving detailed information on the progress of the tunnelling as well as the information that Len and Max had come to visit the site and that Len had brought with him Keating, who he detested and pondered the reason for his bringing the man. As they were leaving Max "told Ned he thought they were going down to Ice Mam". Richard was worried about paying the 7 pounds ten shillings for the Department of Mines survey and was loath to put in another 20 pounds for another share of the mine to pay for it. He gave his thanks for a parcel of parsley he'd received , dated Tue 21st Feb 33. .84) Handwritten two page letter written saying that he had received Ned's cheque (for wages) and giving detailed information on the progress and for the need to timber the drive and have the bottom stoped up. He had no timber or laths left and was concerned about the cost necessary to satisfy the Mines Department. He mentions the possibility of insolvency. Fine gold had been found but not like the Madison's tunnel, dated Tue 28th Feb 33. .85) Handwritten two page letter written giving detailed information of the progress in the tunnel and with the expectation that they would soon meet the same wash which was in Madison's Tunnel. He also personal information about his health. the parsley roots received and the apples which Jim had "burgled", dated Sun 5th Mar 33. .86) Handwritten four page letter by with a very detailed account of the progress of the tunnelling and the reason why the expected intersection with the Madison wash did not occur, but with the hope that this intersection would soon occur, then they would be able to meet expenses. He also talked about not being able to pay for the lease but had the hope they they would not be too rigid in their case. He added some personal information about Jim not having the makings of a miner, catching rabbits "for the pot" and the fact that Mr Read was so much better that he was able to ride his horse, dated Sat 11th Mar 33. .87) Handwritten one page letter written from Prahran, acknowledging the receipt of Ned's cheque, a note about the work at the tunnel and some personal information, dated 21/3/33. .88) Handwritten one page letter written from Mt Mercer, saying that there was little change in the tunnel but that he was would open a cross cut north, dated Thur 23 March 33. .89) Handwritten note of a half page telling them that he had cross cut the tunnel, dated Sat 25th Mar. .90) Handwritten one page letter with progress of the tunnelling and where it is in relation to Madison's Tunnel, dated Thur 30th Mar 33. .91) Handwritten three page letter with the first part of the letter talking about the personal and financial worries he and his family had with travelling and mining expenses as well as Ned's wages which could not have been managed without Judy's little car, Jim's help and the payment of Ned's wages by Tom. He went on to give detailed information of the tunnelling and then talked about a letter received by the Department of Mines regarding the non payment of the lease and that a Notice of Abandonment would be published if not paid. Lastly he talked about the struggle he had had with this process and that it was only because of Tom's help that he had been able to continue this far, dated Sun 2/4/33. .92) A one page letter with information about the progress as well as the information that he had not heard from the Mines Department regarding the lease, and the the 1000 sq ft Miners Right Claim was secure, dated Thur 6th April. .93) A three page letter with detailed information about the work in the tunnel and also detailed explanation of the leases he has pegged and repegged. He also thanked Tom for paying the balance which was owed to the Department and informed Tom that he was going home, dated Tues 11th April 33. .94) A four page letter written from Prahran, thanking Tom for Ned's cheque and with information about the work still being carried on by Ned. He also talked about the pegging of the Mt Mercer claim and the cost of the advertisement and application and survey fees to secure the site as well as his opinion of the probable value of the gold from this site. He also stated that he really needed more investment from those who had initially invested with him or from new investors, dated 17/4/33. Included was a one page letter from Edward Woodlock (Ned) to Mr Squire regarding the work he was carrying out at the tunnel, dated Saturday. .95) A three page letterwritten from Mt Mercer, regarding the work in the tunnel and the quality of the gold found and the direction they will take. He also stated that he was posting letters to the original investors to see if they would contribute to the cost of the lease and also talked about another man who had a Notice of Application posted at Grenville for the water rights for a 25 miles long area and a dam. His Capital is 300 pounds and the supposition is that he wants to 'unwater' the leads, dated Frid 20th April. .96) A one page letter regarding the continued work in the tunnel and how his suppositions seemed to be correct, dated Thur 27th April 33. .97) A three page letter thanking Tom for Ned's cheque of 6 pounds 7 shillings and 6 pence. He also gave detailed information about the tunneling and the type of ground found and his next intentions. He also gave further information about the Notice of Application at Grenville which was posted by B Ryan, Agent for Western Deep Leads Coy Limited for 6000 acres, dated Sun 30th April 33. As well is a note detailing the information copied from the Notice. .98) A two page handwritten letter detailing the work being carried out as well as a complaint that he had not heard from the men he had written to, dated Thur 4th May 33. .99) A one page handwritten letter regarding the tunnel work and informing Tom that the gold found is shotty, dated Sat 6th May 33. .100) A four page handwritten letter written from Prahran, detailing the tunnel work and informing that the gold prospects were better in no.1 cross cut south and there was also payable fair gold where they were currently working, if worked in bulk. He also talked about the possibility of new investors as the old ones had not responded to his letter and the necessity of securing the leases, dated 11th May 1933. .101) A one page handwritten letter by E. Woodlock (Ned) to Mr Squire regarding the work going on, dated Thursday. .102) A six page handwritten letter written from Prahran historically detailing the acquisition of the two leases at Mt Mercer, 35 years earlier, with M C Donnely/Donney and Jas Clements, including Madisons. He goes on to clarify Tom's suggestion regarding the Leases and the Companies to be floated, then details the the shafts, bores, tunnels and Deep Leads held in the leases and then goes on to say what his next steps would be, dated 13th May 33. .103) A two page letter written from Mt Mercer detailing the continued work in the tunnel with the added information that because of the incline it was taking two men to push the truck up the tunnel. Richard also told of the need to take more parsley water for his condition, dated Thur 18th 33. .104) A three page letter with a very detailed description of the work in the tunnel. Richard also told that he had run out of metal rails and was having to use timber as a substitute. He was also to re-peg the North and South Leases in the morning, dated Sun 21st May 33. .105) A two page letter detailing the work in the tunnel and saying that there was a hundred feet of rail locked in by a fall in the No.2 Tunnel and he was hoping to get them out to replace the wooden rails as they made for heavy work on the inclines. He also said that he had a letter from the Department telling him to communicate with the Surveyor in Ballarat, dated Wed 24th May. .106) A three page letter acknowledging Ned's cheque as well as information about the work in the tunnel, including that he had been able to retrieve 45 feet of rail and would get more when needed. He said he was pleased that Tom and Mr Wilkinson were making a trip on Saturday to see him. He talked of the weather and the fact that the bread was a week old, so to bring enough to last till the Monday. Among other things he also spoke of Tom revising the Plans and also having a Share book printed and the name was to be the Ballarat Deep Leads Extension for which there could possibly be 3 Companies, dated Sun 28th May. .107) A one page letter with information about the work in the tunnel and also a weather update and the best way to come, dated Wed 31 May 33. .108) A two page letter written from Prahran, explaining a visit to the Leigh River Shaft to get whim rope, whip wheels and sundry items. He shifted some equipment and built a new forge and was to fix and mount a windlass and rope to enable Ned to get the truck up the incline of the tunnel. He also spoke of the work being undertake by Ned then when on to more personal correspondence about a birthday present for one of Tom's boys, dated 9/6/33. .109) A two page letter acknowledging receipt of the 'Prospectus of the Ballarat Deep Leads Extension Syndicate' and 'Share Certificate'. The No.1 Lease was in Ned's name and the No.2 Lease was in Jim's name to avoid inquisitive interest. Jim logged a Notice of Application and paid the fees. Richard acknowledged receipt of Ned's cheque and asked for 5 pounds as his finances were 'rather tight', dated 14/6/33. Included was a 1 page letter from Ned to Mr Squire regarding the work in the mine, dated Saturday. .110) A one page letter written from Mt Mercer giving information about what was happening in the new x cut N near the mouth of the tunnel, dated Friday 16/6/33. .111) A one page letter telling about the work and that he had fixed an old shed of Mr Reads for the forge. Mr Read and Mr Cameron visited and Richard was hopeful that Mr Cameron, the owner of the land in the North Lease would be easy as regards an agreement, dated June 22/33. .112) A two page letter which talked about his health, the mine, the local J.P. who had lost his eye in a shearing accident and the surveyors visit, He also spoke about contacting the Gold Mines Ltd and the Berry Leads Company, dated Tue 27th 33. Also included was a letter to the Mines Department and a receipt from the Mines Department for the sum of 7 pounds 10 shillings as well as the Lease Applications from the newspaper dated June 13th 1933. .113) A two page letter complaining of the charge made by the Mines Department for a Surveyors Inspection. He also wrote of trying to set up a float for the mine which he would do when he returned home.He also explained the current findings at the mine, dated Sun 2nd July 1933. .114) A one page note written from Prahran informing Tom that he had not yet heard from Gold Mines Ltd and also that there was a hitch with the lease on the house, but this was to hopefully be fixed the following day. He also spoke of Tom's trip home (completed in tow), dated 18/7/33. .115) A two page letter recounting some of the difficulties they were having with the new owners of the house they leased in Prahran. He also spoke of the fact that the Mines Department had requested another 10 pounds although they had not yet completed the survey on either mine, dated 21/7/1933. Also included was a one page letter from E. Woodlock (Ned) to Mr Squire about the workings, dated Tuesday and a letter from the Gold Mines of Australia Limited saying that the information he had supplied was now with their engineers, dated 20th July, 1933. .116) A three page letter written from Armidale saying that Mam (his wife) was fretting with the move to this house. He also told of the rejection by the Gold Mines of Australia Limited of his proposal to invest in his Mt Merser Mine, stating that he believed that Jim Clements who had been the manager when the mine had previously been opened, had most likely "thrown all the cold water he could" on the proposal. He spoke at length about how this man had run the mine into the ground and his own involvement with the winding up of the company. He went on to say that he would approach Ryall to see if he was interested in investing, dated 28/7/33. Included was the letter from Gold Mines of Australia Limited, dated 26th July, 1933. .117) A two page letter written from Prahran telling of the move to another house where Mam was quite settled. He also wrote of the work Ned was carrying out at the mine as well as personal and family news. He wrote that as he had not heard from Ryall, he would visit him the following day, dated 6/8/33. Also included was a two page letter from E Woodlock to Mr Squire giving detailed information of the progress at the tunnel, as well as asking for a new pair of boots as the ground was so wet his were letting in the water, dated Thursday. .118) A two page letter explaining about a letter he received from Mr Cameron who believed he had found gold as well as some personal information and his health, dated 8/8/33. Also included was a one page letter from Neil W Cameron to R B Squire telling about some specks of gold he'd found in a post hole, dated July 31st 33. Thirdly was a one page letter from Ned to Mr Squire explaining the work he was doing in the tunnel, dated Saturday. .119) A one page note saying that he did not like the enclosed 2 copies of the typed Agreement of the Leigh River Gold Mining Company with William Ryall, but asked Tom's advice. dated 9/8/33. .120) A two page letter dealing mainly about the work going on at the new house and the settling in process. He also wrote about the proposed Agreement with Ryall, dated 11/8/33. Also included was a one page letter from Mr Ryall to R B Squire from which part of the left hand side had been severed, dated 10th August 1933. .121) A one page note from R B Squire to W Ryall dated 14/8/33, with attached one page of information and figures. Also attached a one page letter from R B Squire to W Ryall asking if Ryall would be interested viewing the plans for an alluvial mining proposition, dated 27/7/33. .122) A three page letter mainly about the visit to Ryall and a Mr Cundy about the proposed agreement with his concerns about the language and terms of the agreement, dated Sun 21st 33. Also included was a letter from Ned to Mr Squire about the continued work in the tunnel and the fact that two of the pick heads had cracked and would have to be fixed, dated Thursday. .123) A two page letter dealing with a meeting had with Ryall and others in a private office regarding the interest in investing in the mining proposition, dated 23/8/33. .124) A four page letter dealing mainly with the work at the tunnel and exploratory diggings at the spot Mr Cameron had written about as well as the damage done to the car on the way to the workings, dated 29/8/33. .125) A one page letter telling of a proposed meeting with Mr Taylor and a Mr Bowler, who may turn out to be Alan Bowler who he knew, regarding the Mr Mercer Float scheduled for the following day, dated 30/8/33. .126) A five page letter explaining the content of the meeting held with Mr Bowler, who represented an English consortium which was interested in the Mt Mercer site. He explained the terms that the consortium would offer if they went ahead, This included 25 % shares in the mine but no money, which he bemoaned because of the shortness of their cash reserves. He went on to detail the 4 distinct deposits of wash in this field, which he believed were unique in the Ballarat district. He also stated that he had not heard from Mr Ryall. He closed by talking about the water levels in the mine, dated 1/9/33. .127) A two page letter saying that he had written an 11 page report on the Mt Mercer field for the English consortium as well as a private letter for the chairman.He also reported that he had been to see Ryall. Neither party knew that he was talking to the other. added was some personal information, dated 6/9/33. .128) A one page letter telling of a meeting with Mr Bowler and Mr Tayler who carefully went through his report. It was then being typed. He believed he had two strong supporters, dated 7/9/33. Also included was a 2 page note from A Bowler to R B Squire asking him to bring the report into the office the following day to be perused and typed, dated Sept 6th 33. .129) A two page letter with personal encouragement for one of the children. The letter then goes on with more information about the meeting with Mr Tayler and Bowler and his impressions of their interest. He also talked about the one of the experts who was to examine the site and also about the report which was now typed and a copy sent to Tom, dated 8/9/33. .130) A one page letter keeping him informed of progress. The expert was away but would be briefed on his return. He also thanked Tom for a cheque, which was used to get the car 'Liz' back in order for the trip to be made with the experts at a later date. He informed Tom of his intention to return to Mt Mercer, dated 13/9/33. .131) A one page letter written from Mt Mercer telling of the trip from Melbourne and the weather. He spoke of what was happening in the tunnel and that he had not yet heard from any of the interested parties, dated Tue 19th Sept. .132) A five page letter written from Prahran with detailed information about the tunnels, the washes and the shows. He also detailed his meeting with Bryant 38 years ago at the No 1 at Carisbrook and how he had given him assistance at that time and subsequently as well as giving his version of a potted history of Bryant, dated 29/9/33. .133) A two page letter with information about the arrival of the chairman of the English group and that Ned had shown Mr Kermode around the site, dated 6/10/33. Also included was a cutting from the Age about the arrival of Mr F W Baker, representing a large English financial group interested in Victorian deep lead propositions, dated Oct 6th. As well were two, one page letters from Ned (E Woodlock) to Tom, regarding the work in the tunnels, the bad air and the hopes of a successful float, dated Tuesday and Wednesday. .134) A one page letter thanking them for the gift of eggs and parsley. He also talked about a letter from Bowler regarding the business of the experts and that their leases would be seen in due course, dated 10/10/33. Included was a one page letter from A Bowler to P B Squires saying that Mt Mercer site was receiving attention but that no decision had as yet been made, dated Oct 9th 1933. .135) A three page letter written from Prahran giving information about Richards visit and conversation with Mr Ryall, who indicated that no decision had as yet been made regarding his proposal. He also included some personal information about members of the family, dated 18/10/33. Included was a one page letter from Ned (E Woodlock) to Tom with information about the tunnelling progress in no.2 tunnel and the bad air that drove them out for a time, dated Saturday. .136) A one page letter containing a brief update on the state of affairs , dated 20/10/33. Included was a one page letter from Ned to Mr Squire with an information on the progress at the tunnel and with the information that his hands were cracked so badly that he was wearing two socks on each hand, dated Saturday. .137) A one page letter which family news and a paragraph about the figures in his calculations, dated 21/10/33. On the back side was a letter from E Squire (his wife) to Tom, Hazel & boys again with family and personal information, dated 22nd 10/33. .138) A three page letter with the disappointing news that the English consortium would not take up the option on the Mt Mercer lease and gave his opinion that it was self interest that stopped it going ahead. He then gave two options as to the way forward, dated 24/10/33. Also included was a typed one page letter from W C Tayler to R B Squire informing him of a letter stating that the proposal had been turned down, dated 23rd October 1933. .139) A three page letter informing of further developments with Mr Tayler who asked for the plans to be left at the office till the following week as there was another company who may yet be interested to take up the option, dated 27/10/33. .140) A one page letter asking for 9 copies of the old agreement to be typed for the 3 Syndicate members, Rice, Cameron and McNaughton, dated 5/11/33. .141) A three page letter regarding the decision by the Syndicate to reopen the LRG shaft and the practical issues of timber acquisition and probable costs. He then went on to talk about Mam's indisposition and treatment by the herbalist, Goon, dated 8/11/33. Also included was a newspaper clipping from the Age entitled 'Inquiries for properties at Ballarat'. .142) A three page letter giving all the news regarding the agreements, the costs and the way forward. He also spoke of his wife's improvement and other personal information, dated 11/11/33. .143) A two page letter written from Mt Mercer regarding the difficulties in obtaining the timbers and tanks needed to reopen the shaft and the state of all the existing fittings and what would be needed to get the site operational again. His agreement with Mr Read had duly been signed, dated Thurs 16th 33. .144) A two page letter with further information about the progress with acquiring and repairing the shaft site, dated Mon Nov 20th 33. .145) A three page letter informing that the timber for the whim & shaft were being delivered and the area had been cleared out for the poppet heads. The top of the shaft had been cleared ready for re-framing and other work had been carried out. Liz, the car had broken down and Jim was in the process of fixing her. He concluded with information about his and his wife's health, dated Sun 26th Nov 33. .146) A four page letter with news of Mam's health, the problems associated with fixing the car and the floods which stopped Jim from going to Ballarat and washed away the Gary Bridge which affected the mail and had halted work at the shaft, as well as delaying the second delivery of timber, dated Sun Dec 3rd. .147) richard squire, william ryall, jim clements, gold mines of australia limited, e woodlock, ned woodlock, neil w cameron, alan bowler, mr cundy, don mcnaughton, mr rice -
 Marysville & District Historical Society
Postcard (item) - Novelty postcard, Valentine Publishing Co. Pty. Ltd, ALL THE BEST FROM MARYSVILLE, 1940's-1960's
... In his right hand is a glass tankard of beer and in his left hand is a pipe. The title of the postcard is across the top edge of the postcard. There is a lift-up...In his right hand is a glass tankard of beer and in his left hand is a pipe. The title of the postcard is across the top edge of the postcard. There is a lift-up ...A novelty postcard with pull-out strip of 9 miniature photographs that was produced by the Valentine Publishing Co as a souvenir of Marysville.A novelty postcard with pull-out strip of 9 miniature photographs that was produced by the Valentine Publishing Co as a souvenir of Marysville.ALL THE BEST FROM/ MARYSVILLE 1997 PRINTED PAPER MAILING NOVELTY TO OPEN RAISE FLAP From VALENTINE'S "MAIL NOVELTY" POST CARD COPYRIGHT Printed in Great Britain Tomarysville, victoria, postcard, souvenir, valentine publishing co, crossways cabaret (image 1), taggerty river (image 2), acheron way (image 3), blacks spur road (image 4), nicholl's lookout (image 5), main street marysville (image 6), sugarloaf bay eildon (image 7), steavenson falls (image 8), cumberland falls (image 9) -
 Marysville & District Historical Society
Postcard (item) - Colour postcard, Nucolorvue Productions Pty. Ltd, Pack Road from F.J. Barton Bridge, Pre 2009
... hand news/ of you. Regards,/ Elsie Walker A colour photograph of the F.J. Barton Bridge looking up Murchison Street in Marysville in Victoria. There is a hand ...A colour photograph of Murchison Street from the F.J. Barton Bridge in Marysville in Victoria.A colour photograph of Pack Road from the F.J. Barton Bridge in Marysville in Victoria. Labeling is incorrect. The view is looking down Murchison Street from the F.J. Barton Bridge. The F.J. Barton Bridge was named after Frederick John Barton. The Barton Family were amongst Marysville's first pioneering families. This postcard was published by Nucolorvue Productions as a souvenir of Marysville.NU-COLOR-VUE/ OF / AUSTRALIA MARYSVILLE, VICTORIA. Pack Road from F.J. BARTON/ BRIDGE. PLACE/ STAMP/ HERE POST CARD NCV.172 - NUCOLORVUE PRODUCTIONS PTY. LTD./ COPYRIGHT Printed in Australia (Note our new/ bridge) Hullo Dot,/ Very pleased to/ have the chance to meet someone who/ can tell us your news. All the best from/ all the family here at Marysville/ Terry. Dear Dot,/ Good to hear/ first hand news/ of you. Regards,/ Elsie Walkermarysville, f.j. barton bridge, murchison street, victoria, postcard, souvenir, nucolorvue productions, fj barton -
Federation University Historical Collection
Document - Document - Letter, Ballarat Junior Technical School: Letters relating to change of school - Peter Schoutens, 1958
... Hand written letter from Peter stating his new school and requesting the syllabus for some of the technical subjects. He is finding it hard to catch up due to the different styles in teaching. ballarat junior technical school head master l garner peter schoutens character reference scholastic abilities standard completed in ballarat mitchelton state high school brisbane syllabus .1: page, typed. .2: lined, hand written in blue pen Ballarat Junior Technical School: Letters relating to change of school - Peter Schoutens, 1958 Document Document - Letter ....1: Letter written by L Garner to the Head Master of the school Peter Schoutens would be attending after moving from Ballarat to Brisbane, Queensland. It is a reference and states the level of education Peter has attained. It also gives a character reference. .2: Hand written letter from Peter stating his new school and requesting the syllabus for some of the technical subjects. He is finding it hard to catch up due to the different styles in teaching..1: page, typed. .2: lined, hand written in blue penballarat junior technical school, head master, l garner, peter schoutens, character reference, scholastic abilities, standard completed in ballarat, mitchelton state high school, brisbane, syllabus -
 Marysville & District Historical Society
Letter (item) - Hand written letter, 03-11-1934
... hand written letter accepting the offer of a position as a cook at Marysville House. The writer also requests an advancement of wages to enable them to settle up at their current employer and travel to Marysville. Marysville House was built in the late 1920s by Arthur Dickinson. A digital copy of a hand written letter accepting the offer of a position as a cook at Marysville House. The writer also requests an advancement of wages to enable them to settle up at their current employer and travel to Marysville. Marysville House was built in the late 1920s by Arthur Dickinson. marysville victoria australia marysville house arthur james dickinson grace dickinson arnold spooner eileen marie spooner eileen marie dickinson grace sweetland eric dowdle elsie may denton elsie may dickinson peter dickinson linda dickinson 2009 black saturday bushfires letter A digital copy of a hand ...A digital copy of a hand written letter accepting the offer of a position as a cook at Marysville House. The writer also requests an advancement of wages to enable them to settle up at their current employer and travel to Marysville. Marysville House was built in the late 1920s by Arthur Dickinson.A digital copy of a hand written letter accepting the offer of a position as a cook at Marysville House. The writer also requests an advancement of wages to enable them to settle up at their current employer and travel to Marysville. Marysville House was built in the late 1920s by Arthur Dickinson.marysville, victoria, australia, marysville house, arthur james dickinson, grace dickinson, arnold spooner, eileen marie spooner, eileen marie dickinson, grace sweetland, eric dowdle, elsie may denton, elsie may dickinson, peter dickinson, linda dickinson, 2009 black saturday bushfires, letter -
 Lara RSL Sub Branch
British Commonwealth of Nations flag circ world war 1, British Commonwealth of Nations flag world war 1
... Flag White Ensign is made up from Commonwealth Countries and displayed as a flag- Top left-hand corner British flag, right-hand top corner Coat of arms of South Africa, bottom-left Coat of Arms for Canada, Bottom right corner Advance Australia Coat of Arms, flag center is for India is a yellow and red rosette and New Zealand is represented by four white 5 pointed stars centralized as representation of the Southern Cross....British Imperial Forces involved in World War 1 Rear representation, british expeditionary forces flag union jack white ensign coat of arms of south africa coat of arms canada coat of arms advance australia rosette of india The flag on the left border is marked with "Groves" Flag White Ensign is made up from Commonwealth Countries and displayed as a flag- Top left-hand corner British flag, right-hand top corner Coat of arms of South Africa, bottom-left Coat of Arms for Canada, Bottom right corner Advance Australia Coat of Arms, flag center is for India is a yellow and red rosette and New Zealand is represented by four white 5 pointed stars centralized as representation of the Southern Cross. ...British Imperial Forces involved in World War 1Rear representation, Flag White Ensign is made up from Commonwealth Countries and displayed as a flag- Top left-hand corner British flag, right-hand top corner Coat of arms of South Africa, bottom-left Coat of Arms for Canada, Bottom right corner Advance Australia Coat of Arms, flag center is for India is a yellow and red rosette and New Zealand is represented by four white 5 pointed stars centralized as representation of the Southern Cross.The flag on the left border is marked with "Groves"british expeditionary forces flag, union jack, white ensign, coat of arms of south africa, coat of arms canada, coat of arms advance australia, rosette of india -
 Lara RSL Sub Branch
Cloth Badge, HMAS Vendetta
... up until 1978. In October 1979, the destroyer was decommissioned, and served as a parts hulk for sister ship HMAS Vampire. Vendetta was sold for ship breaking in January 1987. Cloth Badge for HMAS Vendetta DD-08 hmas vendetta royal australian navy ran cloth badge hand holding dagger dd-08 HMAS Vendetta DD-08 with hand holding dagger in centre of badge Circular cloth badge HMAS Vendetta Cloth Badge ...Cloth badge for HMAS Vendetta DD-08. HMAS Vendetta was one of three Daring class destroyers built for and operated by the Royal Australian Navy (RAN). The destroyer was built by Williamstown Naval Dockyard and entered service in 1958. During her early career, Vendetta was deployed to the Far East Strategic Reserve on multiple occasions. In 1965 and 1966, the destroyer undertook deterrence patrols during the Indonesia-Malaysia Confrontation. Along with several runs escorting the troop transport HMAS Sydney to Vietnam, from late 1969 to early 1970 Vendetta was assigned to combat operations, and became the only Australian-built warship to serve in a shore bombardment role during the Vietnam War. The ship underwent a two-year modernisation from 1971 to 1973, and in December 1974 was one of thirteen RAN warships involved in Operation Navy Help Darwin after Cyclone Tracy devastated Darwin. Several more deployments were made to the Far East, up until 1978. In October 1979, the destroyer was decommissioned, and served as a parts hulk for sister ship HMAS Vampire. Vendetta was sold for ship breaking in January 1987.Cloth Badge for HMAS Vendetta DD-08Circular cloth badgeHMAS Vendetta DD-08 with hand holding dagger in centre of badgehmas vendetta, royal australian navy, ran, cloth badge, hand holding dagger, dd-08 -
 Shepparton RSL Sub Branch
Uniform, trousers, Conway Bros. PTY. LTD, 1969
... up at the front with 6 plastic buttons. There is an additional strip of fabric attached to the right-hand fly which can be fastened with an extra button on the interior of the left-hand fly. ...(end of box containing words) NAME.....DOCKSEY (‘Docksey is in hand-written black ink) ARMY No.....216308 (numbers also hand-written in black ink) (the number 40 is also wrtten in faded black ink in the top right corner of the label) khaki coloured trousers which are composed of a heavy fabric. The trousers button up at the front with 6 plastic buttons. There is an additional strip of fabric attached to the right-hand ...These trousers are part of a Royal Australian Army Ordnance Corps uniform. The Royal Australian Army Ordnance Corps (RAAOC) is responsible for various logistics and organisational operations, such as maintenance of parachutes, fuel distribution, personnel administration, exlosive disposal and laundy operations. The trousers were manufactured in 1969 and were worn by an unknown RAAOC serviceman. The patches on the sleeves of the corresponding jacket denote that he had earned qualifications as a parachuter and a marksman and that he was a Warrant Officer 1. Due to the period of manufacture it can be presumed that the serviceman whom this uniform belonged to served in the Vietnam War.As historic military uniform trousers dating to 1968, it is presumed that this item would have been used in service during the Vietnam War. The wearer of the uniform is unknown, however the patches and flashes attached signify that the serviceman worked for the Royal Australian Army Ordnance Corps, earned qualifications as a parachuter and marksman and ranked highly as a Warrant Officer 1. The item is representative of a type of uniform worn by high ranking RAAOC servicemen during the 1960’s. It is also in very good condition for its age.khaki coloured trousers which are composed of a heavy fabric. The trousers button up at the front with 6 plastic buttons. There is an additional strip of fabric attached to the right-hand fly which can be fastened with an extra button on the interior of the left-hand fly. There are an additional 6 buttons along the interior waistband. There are also three buttons on the exterior waistband down the front and a buckle. The buttons are composed of brown plastic. There are two open hip pockets, one on either side, and another button-up pocket on the right-hand side of the back. There is a white label with inscriptions attached to the interior of the back pocket with an extra piece of fabric attached for mending patches.Printed in black inscriptions on the white label: CONWAY BROS. PTY. LTD ADELAIDE 1969 (a broad arrow) Class 8405-66-025-6183 A W M 7 (these characters are stamped in faded black ink) SIZE & WAIST 33R MATCHING JACKET 37-38R in a box are the words: DRY CLEAN ONLY. Re-press on original seams. Creases set by Si-ro-set. Mending patch attached. (end of box containing words) NAME.....DOCKSEY (‘Docksey is in hand-written black ink) ARMY No.....216308 (numbers also hand-written in black ink) (the number 40 is also wrtten in faded black ink in the top right corner of the label)military, army, raaoc, marksman, royal australian army ordnance corps, parachuting, warrant officer, uniform, trousers -
 Flagstaff Hill Maritime Museum and Village
Leisure object - Snuff, Fribourg & Treyer, 1900's
... hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up...hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up ...This dry tobacco variety of snuff is a finely ground, flavoured tobacco intended to be sniffed into the nose (not further into the sinuses or throat). It can vary in grind, blend and moistness. Snuff sniffing has been popular, particularly amongst the aristocracy, since the 1600’s and into the 1900’s and is becoming popular again as an alternative to smoking. It delivers a ‘hit’ of nicotine with lingering flavours that last for 15 to 20 minutes. It can be used by pinching a small amount from the container with thumb and forefinger then holding the pinched fingers to each nostril and giving a quick short sniff to transfer the snuff into the nostril. Another way is to sniff it from the ‘anatomical snuff box’, the depression on the back of the hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up to 2 years, and for up to 6 months once the packet is opened and kept in a cool dark place. The most popular line of the Wilson’s snuffs is the SP line’s ‘Best SP Snuff”. They are also still selling Fribourg & Treyer’s “French Carrotte” and “Hot Dry Toast”. This snuff was part of Dr Angus's personal effects and was donated to Flagstaff Hill Maritime Village by the family of Doctor William Roy Angus, Surgeon and Oculist. It is part of the “W.R. Angus Collection” that includes historical medical equipment, surgical instruments and material once belonging to Dr Edward Ryan and Dr Thomas Francis Ryan, (both of Nhill, Victoria) as well as Dr Angus’ own belongings. The Collection’s history spans the medical practices of the two Doctors Ryan, from 1885-1926 plus that of Dr Angus, up until 1969. ABOUT THE “W.R.ANGUS COLLECTION” Doctor William Roy Angus M.B., B.S., Adel., 1923, F.R.C.S. Edin.,1928 (also known as Dr Roy Angus) was born in Murrumbeena, Victoria in 1901 and lived until 1970. He qualified as a doctor in 1923 at University of Adelaide, was Resident Medical Officer at the Royal Adelaide Hospital in 1924 and for a period was house surgeon to Sir (then Mr.) Henry Simpson Newland. Dr Angus was briefly an Assistant to Dr Riddell of Kapunda, then commenced private practice at Curramulka, Yorke Peninsula, SA, where he was physician, surgeon and chemist. In 1926, he was appointed as new Medical Assistant to Dr Thomas Francis Ryan (T.F. Ryan, or Tom), in Nhill, Victoria, where his experiences included radiology and pharmacy. In 1927 he was Acting House Surgeon in Dr Tom Ryan’s absence. Dr Angus had become engaged to Gladys Forsyth and they decided he would take time to further his studies overseas in the UK in 1927. He studied at London University College Hospital and at Edinburgh Royal Infirmary and in 1928, was awarded FRCS (Fellow from the Royal College of Surgeons), Edinburgh. He worked his passage back to Australia as a Ship’s Surgeon on the on the Australian Commonwealth Line’s T.S.S. Largs Bay. Dr Angus married Gladys in 1929, in Ballarat. (They went on to have one son (Graham 1932, born in SA) and two daughters (Helen (died 12/07/1996) and Berenice (Berry), both born at Mira, Nhill ) Dr Angus was a ‘flying doctor’ for the A.I.M. (Australian Inland Ministry) Aerial Medical Service in 1928 . The organisation began in South Australia through the Presbyterian Church in that year, with its first station being in the remote town of Oodnadatta, where Dr Angus was stationed. He was locum tenens there on North-South Railway at 21 Mile Camp. He took up this ‘flying doctor’ position in response to a call from Dr John Flynn; the organisation was later known as the Flying Doctor Service, then the Royal Flying Doctor Service. A lot of his work during this time involved dental surgery also. Between 1928-1932 he was surgeon at the Curramulka Hospital, Yorke Peninsula, South Australia. In 1933 Dr Angus returned to Nhill where he’d previously worked as Medical Assistant and purchased a share of the Nelson Street practice and Mira hospital from Dr Les Middleton one of the Middleton Brothers, the current owners of what was once Dr Tom Ryan’s practice. Dr L Middleton was House Surgeon to the Nhill Hospital 1926-1933, when he resigned. [Dr Tom Ryan’s practice had originally belonged to his older brother Dr Edward Ryan, who came to Nhill in 1885. Dr Edward saw patients at his rooms, firstly in Victoria Street and in 1886 in Nelson Street, until 1901. The Nelson Street practice also had a 2 bed ward, called Mira Private Hospital ). Dr Edward Ryan was House Surgeon at the Nhill Hospital 1884-1902 . He also had occasions where he successfully performed veterinary surgery for the local farmers too. Dr Tom Ryan then purchased the practice from his brother in 1901. Both Dr Edward and Dr Tom Ryan work as surgeons included eye surgery. Dr Tom Ryan performed many of his operations in the Mira private hospital on his premises. He too was House Surgeon at the Nhill Hospital 1902-1926. Dr Tom Ryan had one of the only two pieces of radiology equipment in Victoria during his practicing years – The Royal Melbourne Hospital had the other one. Over the years Dr Tom Ryan gradually set up what was effectively a training school for country general-practitioner-surgeons. Each patient was carefully examined, including using the X-ray machine, and any surgery was discussed and planned with Dr Ryan’s assistants several days in advance. Dr Angus gained experience in using the X-ray machine there during his time as assistant to Dr Ryan. Dr Tom Ryan moved from Nhill in 1926. He became a Fellow of the Royal Australasian College of Surgeons in 1927, soon after its formation, a rare accolade for a doctor outside any of the major cities. He remained a bachelor and died suddenly on 7th Dec 1955, aged 91, at his home in Ararat. Scholarships and prizes are still awarded to medical students in the honour of Dr T.F. Ryan and his father, Dr Michael Ryan, and brother, John Patrick Ryan. ] When Dr Angus bought into the Nelson Street premises in Nhill he was also appointed as the Nhill Hospital’s Honorary House Surgeon 1933-1938. His practitioner’s plate from his Nhill surgery states “HOURS Daily, except Tuesdays, Fridays and Saturday afternoons, 9-10am, 2-4pm, 7-8pm. Sundays by appointment”. This plate is now mounted on the doorway to the Port Medical Office at Flagstaff Hill Maritime Village, Warrnambool. Dr Edward Ryan and Dr Tom Ryan had an extensive collection of historical medical equipment and materials spanning 1884-1926 and when Dr Angus took up practice in their old premises he obtained this collection, a large part of which is now on display at the Port Medical Office at Flagstaff Hill Maritime Village in Warrnambool. During his time in Nhill Dr Angus was involved in the merging of the Mira Hospital and Nhill Public Hospital into one public hospital and the property titles passed on to Nhill Hospital in 1939. In 1939 Dr Angus and his family moved to Warrnambool where he purchased “Birchwood,” the 1852 home and medical practice of Dr John Hunter Henderson, at 214 Koroit Street. (This property was sold in1965 to the State Government and is now the site of the Warrnambool Police Station. ). The Angus family was able to afford gardeners, cooks and maids; their home was a popular place for visiting dignitaries to stay whilst visiting Warrnambool. Dr Angus had his own silk worm farm at home in a Mulberry tree. His young daughter used his centrifuge for spinning the silk. Dr Angus was appointed on a part-time basis as Port Medical Officer (Health Officer) in Warrnambool and held this position until the 1940’s when the government no longer required the service of a Port Medical Officer in Warrnambool; he was thus Warrnambool’s last serving Port Medical Officer. (The duties of a Port Medical Officer were outlined by the Colonial Secretary on 21st June, 1839 under the terms of the Quarantine Act. Masters of immigrant ships arriving in port reported incidents of diseases, illness and death and the Port Medical Officer made a decision on whether the ship required Quarantine and for how long, in this way preventing contagious illness from spreading from new immigrants to the residents already in the colony.) Dr Angus was a member of the Australian Medical Association, for 35 years and surgeon at the Warrnambool Base Hospital 1939-1942, He served as a Surgeon Captain during WWII 1941-45, in Ballarat, Victoria, and in Bonegilla, N.S.W., completing his service just before the end of the war due to suffering from a heart attack. During his convalescence he carved an intricate and ‘most artistic’ chess set from the material that dentures were made from. He then studied ophthalmology at the Royal Melbourne Eye and Ear Hospital and created cosmetically superior artificial eyes by pioneering using the intrascleral cartilage. Angus received accolades from the Ophthalmological Society of Australasia for this work. He returned to Warrnambool to commence practice as an ophthalmologist, pioneering in artificial eye improvements. He was Honorary Consultant Ophthalmologist to Warrnambool Base Hospital for 31 years. He made monthly visits to Portland as a visiting surgeon, to perform eye surgery. He represented the Victorian South-West subdivision of the Australian Medical Association as its secretary between 1949 and 1956 and as chairman from 1956 to 1958. In 1968 Dr Angus was elected member of Spain’s Barraquer Institute of Barcelona after his research work in Intrasclearal cartilage grafting, becoming one of the few Australian ophthalmologists to receive this honour, and in the following year presented his final paper on Living Intrasclearal Cartilage Implants at the Inaugural Meeting of the Australian College of Ophthalmologists in Melbourne In his personal life Dr Angus was a Presbyterian and treated Sunday as a Sabbath, a day of rest. He would visit 3 or 4 country patients on a Sunday, taking his children along ‘for the ride’ and to visit with him. Sunday evenings he would play the pianola and sing Scottish songs to his family. One of Dr Angus’ patients was Margaret MacKenzie, author of a book on local shipwrecks that she’d seen as an eye witness from the late 1880’s in Peterborough, Victoria. In the early 1950’s Dr Angus, painted a picture of a shipwreck for the cover jacket of Margaret’s book, Shipwrecks and More Shipwrecks. She was blind in later life and her daughter wrote the actual book for her. Dr Angus and his wife Gladys were very involved in Warrnambool’s society with a strong interest in civic affairs. Their interests included organisations such as Red Cross, Rostrum, Warrnambool and District Historical Society (founding members), Wine and Food Society, Steering Committee for Tertiary Education in Warrnambool, Local National Trust, Good Neighbour Council, Housing Commission Advisory Board, United Services Institute, Legion of Ex-Servicemen, Olympic Pool Committee, Food for Britain Organisation, Warrnambool Hospital, Anti-Cancer Council, Boys’ Club, Charitable Council, National Fitness Council and Air Raid Precautions Group. He was also a member of the Steam Preservation Society and derived much pleasure from a steam traction engine on his farm. He had an interest in people and the community He and his wife Gladys were both involved in the creation of Flagstaff Hill, including the layout of the gardens. After his death (28th March 1970) his family requested his practitioner’s plate, medical instruments and some personal belongings be displayed in the Port Medical Office surgery at Flagstaff Hill Maritime Village, and be called the “W. R. Angus Collection”. The W.R. Angus Collection is significant for still being located at the site it is connected with, Doctor Angus being the last Port Medical Officer in Warrnambool. The collection of medical instruments and other equipment is culturally significant, being an historical example of medicine from late 19th to mid-20th century. Dr Angus assisted Dr Tom Ryan, a pioneer in the use of X-rays and in ocular surgery. Snuff in metal cylinder, part of the W.R. Angus Collection. Small silver metal cylinder with screw cap containing dark, fragrant ground substance. . Snuff aroma is “High Dry Toast”. Label on cylinder has information about the maker. The snuff container has been opened.Print on label reads "Fribourg & Treyer brand, est. 1720, Tobacconists & Purveyors of Foreign Snuff, to their Majesties the Kings of Stanober and Belgium, the Dukes of Sussex, Cambridge and Duchesses of Kent. No. 34 Upper End of the Haymarket W.S.1. Lloyds Leadenhal St, E.C.3, 130 High St Oxford and 18 Burlington Arcade, W.1".Symbol of a crown above a topless pyramid.flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, dr w r angus, snuff, hot dry toast, fribourg & treyer, tobacco sniffing, personal effects -
 Flagstaff Hill Maritime Museum and Village
Leisure object - Snuff, c. 1900's
... hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up...hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up ...This dry tobacco variety of snuff is a finely ground, flavoured tobacco intended to be sniffed into the nose (not further into the sinuses or throat). It can vary in grind, blend and moistness. Snuff sniffing has been popular, particularly amongst the aristocracy, since the 1600’s and into the 1900’s and is becoming popular again as an alternative to smoking. It delivers a ‘hit’ of nicotine with lingering flavours that last for 15 to 20 minutes. It can be used by pinching a small amount from the container with thumb and forefinger then holding the pinched fingers to each nostril and giving a quick short sniff to transfer the snuff into the nostril. Another way is to sniff it from the ‘anatomical snuff box’, the depression on the back of the hand between base of thumb and forefinger. The user can also purchase a specially crafted snuff box or a bullet shaped nasal dispenser. A useful accessory to have on hand is a handkerchief, as the process of inhaling snuff can cause sneezing and increased nasal discharge. Snuff will keep in its sealed packet for up to 2 years, and for up to 6 months once the packet is opened and kept in a cool dark place. The most popular line of the Wilson’s snuffs is the SP line’s ‘Best SP Snuff”. They are also still selling Fribourg & Treyer’s “French Carrotte” and “Hot Dry Toast”. This snuff container was part of Dr. W.R. Angus' own personal effects. It was donated to Flagstaff Hill Maritime Village by the family of Doctor William Roy Angus, Surgeon and Oculist. It is part of the “W.R. Angus Collection” that includes historical medical equipment, surgical instruments and material once belonging to Dr Edward Ryan and Dr Thomas Francis Ryan, (both of Nhill, Victoria) as well as Dr Angus’ own belongings. The Collection’s history spans the medical practices of the two Doctors Ryan, from 1885-1926 plus that of Dr Angus, up until 1969. ABOUT THE “W.R.ANGUS COLLECTION” Doctor William Roy Angus M.B., B.S., Adel., 1923, F.R.C.S. Edin.,1928 (also known as Dr Roy Angus) was born in Murrumbeena, Victoria in 1901 and lived until 1970. He qualified as a doctor in 1923 at University of Adelaide, was Resident Medical Officer at the Royal Adelaide Hospital in 1924 and for a period was house surgeon to Sir (then Mr.) Henry Simpson Newland. Dr Angus was briefly an Assistant to Dr Riddell of Kapunda, then commenced private practice at Curramulka, Yorke Peninsula, SA, where he was physician, surgeon and chemist. In 1926, he was appointed as new Medical Assistant to Dr Thomas Francis Ryan (T.F. Ryan, or Tom), in Nhill, Victoria, where his experiences included radiology and pharmacy. In 1927 he was Acting House Surgeon in Dr Tom Ryan’s absence. Dr Angus had become engaged to Gladys Forsyth and they decided he would take time to further his studies overseas in the UK in 1927. He studied at London University College Hospital and at Edinburgh Royal Infirmary and in 1928, was awarded FRCS (Fellow from the Royal College of Surgeons), Edinburgh. He worked his passage back to Australia as a Ship’s Surgeon on the on the Australian Commonwealth Line’s T.S.S. Largs Bay. Dr Angus married Gladys in 1929, in Ballarat. (They went on to have one son (Graham 1932, born in SA) and two daughters (Helen (died 12/07/1996) and Berenice (Berry), both born at Mira, Nhill ) Dr Angus was a ‘flying doctor’ for the A.I.M. (Australian Inland Ministry) Aerial Medical Service in 1928 . The organisation began in South Australia through the Presbyterian Church in that year, with its first station being in the remote town of Oodnadatta, where Dr Angus was stationed. He was locum tenens there on North-South Railway at 21 Mile Camp. He took up this ‘flying doctor’ position in response to a call from Dr John Flynn; the organisation was later known as the Flying Doctor Service, then the Royal Flying Doctor Service. A lot of his work during this time involved dental surgery also. Between 1928-1932 he was surgeon at the Curramulka Hospital, Yorke Peninsula, South Australia. In 1933 Dr Angus returned to Nhill where he’d previously worked as Medical Assistant and purchased a share of the Nelson Street practice and Mira hospital from Dr Les Middleton one of the Middleton Brothers, the current owners of what was once Dr Tom Ryan’s practice. Dr L Middleton was House Surgeon to the Nhill Hospital 1926-1933, when he resigned. [Dr Tom Ryan’s practice had originally belonged to his older brother Dr Edward Ryan, who came to Nhill in 1885. Dr Edward saw patients at his rooms, firstly in Victoria Street and in 1886 in Nelson Street, until 1901. The Nelson Street practice also had a 2 bed ward, called Mira Private Hospital ). Dr Edward Ryan was House Surgeon at the Nhill Hospital 1884-1902 . He also had occasions where he successfully performed veterinary surgery for the local farmers too. Dr Tom Ryan then purchased the practice from his brother in 1901. Both Dr Edward and Dr Tom Ryan work as surgeons included eye surgery. Dr Tom Ryan performed many of his operations in the Mira private hospital on his premises. He too was House Surgeon at the Nhill Hospital 1902-1926. Dr Tom Ryan had one of the only two pieces of radiology equipment in Victoria during his practicing years – The Royal Melbourne Hospital had the other one. Over the years Dr Tom Ryan gradually set up what was effectively a training school for country general-practitioner-surgeons. Each patient was carefully examined, including using the X-ray machine, and any surgery was discussed and planned with Dr Ryan’s assistants several days in advance. Dr Angus gained experience in using the X-ray machine there during his time as assistant to Dr Ryan. Dr Tom Ryan moved from Nhill in 1926. He became a Fellow of the Royal Australasian College of Surgeons in 1927, soon after its formation, a rare accolade for a doctor outside any of the major cities. He remained a bachelor and died suddenly on 7th Dec 1955, aged 91, at his home in Ararat. Scholarships and prizes are still awarded to medical students in the honour of Dr T.F. Ryan and his father, Dr Michael Ryan, and brother, John Patrick Ryan. ] When Dr Angus bought into the Nelson Street premises in Nhill he was also appointed as the Nhill Hospital’s Honorary House Surgeon 1933-1938. His practitioner’s plate from his Nhill surgery states “HOURS Daily, except Tuesdays, Fridays and Saturday afternoons, 9-10am, 2-4pm, 7-8pm. Sundays by appointment”. This plate is now mounted on the doorway to the Port Medical Office at Flagstaff Hill Maritime Village, Warrnambool. Dr Edward Ryan and Dr Tom Ryan had an extensive collection of historical medical equipment and materials spanning 1884-1926 and when Dr Angus took up practice in their old premises he obtained this collection, a large part of which is now on display at the Port Medical Office at Flagstaff Hill Maritime Village in Warrnambool. During his time in Nhill Dr Angus was involved in the merging of the Mira Hospital and Nhill Public Hospital into one public hospital and the property titles passed on to Nhill Hospital in 1939. In 1939 Dr Angus and his family moved to Warrnambool where he purchased “Birchwood,” the 1852 home and medical practice of Dr John Hunter Henderson, at 214 Koroit Street. (This property was sold in1965 to the State Government and is now the site of the Warrnambool Police Station. ). The Angus family was able to afford gardeners, cooks and maids; their home was a popular place for visiting dignitaries to stay whilst visiting Warrnambool. Dr Angus had his own silk worm farm at home in a Mulberry tree. His young daughter used his centrifuge for spinning the silk. Dr Angus was appointed on a part-time basis as Port Medical Officer (Health Officer) in Warrnambool and held this position until the 1940’s when the government no longer required the service of a Port Medical Officer in Warrnambool; he was thus Warrnambool’s last serving Port Medical Officer. (The duties of a Port Medical Officer were outlined by the Colonial Secretary on 21st June, 1839 under the terms of the Quarantine Act. Masters of immigrant ships arriving in port reported incidents of diseases, illness and death and the Port Medical Officer made a decision on whether the ship required Quarantine and for how long, in this way preventing contagious illness from spreading from new immigrants to the residents already in the colony.) Dr Angus was a member of the Australian Medical Association, for 35 years and surgeon at the Warrnambool Base Hospital 1939-1942, He served as a Surgeon Captain during WWII 1941-45, in Ballarat, Victoria, and in Bonegilla, N.S.W., completing his service just before the end of the war due to suffering from a heart attack. During his convalescence he carved an intricate and ‘most artistic’ chess set from the material that dentures were made from. He then studied ophthalmology at the Royal Melbourne Eye and Ear Hospital and created cosmetically superior artificial eyes by pioneering using the intrascleral cartilage. Angus received accolades from the Ophthalmological Society of Australasia for this work. He returned to Warrnambool to commence practice as an ophthalmologist, pioneering in artificial eye improvements. He was Honorary Consultant Ophthalmologist to Warrnambool Base Hospital for 31 years. He made monthly visits to Portland as a visiting surgeon, to perform eye surgery. He represented the Victorian South-West subdivision of the Australian Medical Association as its secretary between 1949 and 1956 and as chairman from 1956 to 1958. In 1968 Dr Angus was elected member of Spain’s Barraquer Institute of Barcelona after his research work in Intrasclearal cartilage grafting, becoming one of the few Australian ophthalmologists to receive this honour, and in the following year presented his final paper on Living Intrasclearal Cartilage Implants at the Inaugural Meeting of the Australian College of Ophthalmologists in Melbourne In his personal life Dr Angus was a Presbyterian and treated Sunday as a Sabbath, a day of rest. He would visit 3 or 4 country patients on a Sunday, taking his children along ‘for the ride’ and to visit with him. Sunday evenings he would play the pianola and sing Scottish songs to his family. One of Dr Angus’ patients was Margaret MacKenzie, author of a book on local shipwrecks that she’d seen as an eye witness from the late 1880’s in Peterborough, Victoria. In the early 1950’s Dr Angus, painted a picture of a shipwreck for the cover jacket of Margaret’s book, Shipwrecks and More Shipwrecks. She was blind in later life and her daughter wrote the actual book for her. Dr Angus and his wife Gladys were very involved in Warrnambool’s society with a strong interest in civic affairs. Their interests included organisations such as Red Cross, Rostrum, Warrnambool and District Historical Society (founding members), Wine and Food Society, Steering Committee for Tertiary Education in Warrnambool, Local National Trust, Good Neighbour Council, Housing Commission Advisory Board, United Services Institute, Legion of Ex-Servicemen, Olympic Pool Committee, Food for Britain Organisation, Warrnambool Hospital, Anti-Cancer Council, Boys’ Club, Charitable Council, National Fitness Council and Air Raid Precautions Group. He was also a member of the Steam Preservation Society and derived much pleasure from a steam traction engine on his farm. He had an interest in people and the community He and his wife Gladys were both involved in the creation of Flagstaff Hill, including the layout of the gardens. After his death (28th March 1970) his family requested his practitioner’s plate, medical instruments and some personal belongings be displayed in the Port Medical Office surgery at Flagstaff Hill Maritime Village, and be called the “W. R. Angus Collection”. The W.R. Angus Collection is significant for still being located at the site it is connected with, Doctor Angus being the last Port Medical Officer in Warrnambool. The collection of medical instruments and other equipment is culturally significant, being an historical example of medicine from late 19th to mid-20th century. Dr Angus assisted Dr Tom Ryan, a pioneer in the use of X-rays and in ocular surgery. Snuff in metal cylinder, part of the W.R. Angus Collection. Small silver metal cylinder with screw cap. Snuff aroma is “French Carotte”, The label gives details of the snuff and its maker. The cylinder has been opened. The label reads “Fribourg & Treyer brand, est. 1720, Tobacconists & Purveyors of Foreign Snuff, to their Majesties the Kings of Hanover and Belgium, the Dukes of Sussex, Cambridge and Duchess of Kent. No. 34 Upper End of the Haymarket W.S.1. Lloyds Leadenhall St, E.C.3, 130 High St Oxford and 18 Burlington Arcade, W.1.Symbol of a crown above a topless pyramid. Telephone Whitehall 1305, 14 c.c”flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, dr w r angus, snuff, hot dry toast, fribourg & treyer, tobacco sniffing, personal effects
