Showing 270 items matching "early machinery"
-
 Kiewa Valley Historical Society
VHS Video - Kiewa, Kiewa Compile, Date compiled 25th Nov. 1998
... ...early machinery...The additional resources provided by the State Electricity Commission of Victoria of "alpine bush" fire control and management, together with an ongoing educational scheme for school children in learning about what constitutes the Alpine country's unique environment, are a very important offshoot, benefitting to both the communities within the Kiewa Valley and regional Victoria. kiewa hydro electricity state electricity commission of victoria construction towns 1940s 1960s mt beauty bogong falls creek clover power station mckay power station bill sutton news film construction workers early machinery Titled "Kiewa Compile" with 4 short films titled 1. ...The construction and development of the Kiewa Hydro scheme showing its construction and the people in work and play during its duration. It also shows the development of Mt Beauty and Bogong townships. The films were used as News Reels, Tourist Information and Entertainment.This item provids a snap shot in time (1990) when the Kiewa Valley was still relatively under populated and holiday houses owned by city bound workers was still relatively insignificant. As more and more holiday makers retire to a small but friendly region(Kiewa Valley and Mount Beauty) the increase in visitor numbers will affect the local rural bush scene more and more. The changes that will occur (in time) can be measured against the scenes presented in this video. The additional resources provided by the State Electricity Commission of Victoria of "alpine bush" fire control and management, together with an ongoing educational scheme for school children in learning about what constitutes the Alpine country's unique environment, are a very important offshoot, benefitting to both the communities within the Kiewa Valley and regional Victoria.This VHS tape is stored within its own plastic cover which has a front side Titled "KIEWA in the MAKING". The VHS tape is nestled within a formed inner structure which not only prevents the tape from moving to and fro but also unnecessary intrusion of foreign particles. Titled "Kiewa Compile" with 4 short films titled 1. Kiewa in the Making 2. Kiewa Capers 3. It only seems like yesterday 4. Kiewa.kiewa, hydro electricity, state electricity commission of victoria, construction towns, 1940s 1960s, mt beauty, bogong, falls creek, clover power station, mckay power station, bill sutton, news film, construction workers, early machinery -
 Tatura Irrigation & Wartime Camps Museum
Photograph, Dhurringile Mansion Wheat Grader, 1931
... Early example of farm machinery. Contractors would go from farm to farm...Early example of farm machinery. Contractors would go from farm to farm Tom Hastie's farm early farm equipment Hec. ...Early example of farm machinery. Contractors would go from farm to farmBlack and white photograph of wheat grader Hec. McLennan's wheat grader at Tom Hastie's farm 1931.tom hastie's farm, early farm equipment -
Moorabbin Air Museum
Document (Item) - Cloud Seeding In Australia
... Description: 6 x Assorted B&W Photos wg: Early flying boats Helicopters machinery Black Hawk/ Sea Hawk Level of Importance: . ...Description: 6 x Assorted B&W Photos wg: Early flying boats Helicopters machinery Black Hawk/ Sea Hawk Level of Importance: . ...Description: 6 x Assorted B&W Photos wg: Early flying boats Helicopters machinery Black Hawk/ Sea Hawk Level of Importance: . -
 Myrtleford and District Historical Society
Colourized Photograph, "Planting Tobacco N.E. Victoria
... It depicts early post-war machinery in use at the time until affordable modern tractors were available. ...It depicts early post-war machinery in use at the time until affordable modern tractors were available. ...The photograph depicts the 2nd important stage in tobacco growing--transplanting seedlings into open paddocks. It depicts early post-war machinery in use at the time until affordable modern tractors were available. The planting machine has probably been adapted from the horse-drawn era pre-World War 2. The scene is one near Myrtleford in the Ovens Valley.The photograph depicts the slow adaptation of modern tobacco farming methods in the immediate post-war period and the type of terain suitable for tobacco growing. The labour intensive nature of tobacco planting is also depicted.A colourized photograph of tobacco planting activity in a paddock near Myrtleford.Inscription: Planting Tobacco N.E. Victoria"tobacco farming tobacco planting machinery -
 Bendigo Historical Society Inc.
Document - HERCULES AND ENERGETIC MINES - NOTES ON THE HERCULES AND ENERGETIC MINES
... Notes include Location, depth of shafts, plant and machinery, Early History and Prominence. Reference: Mines Dept Special Edition Australian Mining Standard 1.6.1899, Mines Dept Booklet Bendigo Goldfield 1936, Mines Dept Annual and Quarterly Reports, Annals of Bendigo Mining Sections 1876 - 1921, A Richardson, The Bendigo Goldfield Registry J N Macartney 1.3.1871, Mines Dept Bulletin No 30 h Herman 1914, Bendigo Amalgamated Goldfields Coy Financial Reports 1920. ...Notes include Location, depth of shafts, plant and machinery, Early History and Prominence. Reference: Mines Dept Special Edition Australian Mining Standard 1.6.1899, Mines Dept Booklet Bendigo Goldfield 1936, Mines Dept Annual and Quarterly Reports, Annals of Bendigo Mining Sections 1876 - 1921, A Richardson, The Bendigo Goldfield Registry J N Macartney 1.3.1871, Mines Dept Bulletin No 30 h Herman 1914, Bendigo Amalgamated Goldfields Coy Financial Reports 1920. ...Four typed copies of notes on the Hercules and Energetic Mines. Notes include Location, depth of shafts, plant and machinery, Early History and Prominence. Reference: Mines Dept Special Edition Australian Mining Standard 1.6.1899, Mines Dept Booklet Bendigo Goldfield 1936, Mines Dept Annual and Quarterly Reports, Annals of Bendigo Mining Sections 1876 - 1921, A Richardson, The Bendigo Goldfield Registry J N Macartney 1.3.1871, Mines Dept Bulletin No 30 h Herman 1914, Bendigo Amalgamated Goldfields Coy Financial Reports 1920. There are three typed copies, also the original handwritten notes.mine, gold, hercules and energetic mines, notes on the hercules and energetic mines, the north energetic, the victoria pilot, plan of leases of 1870, bendigo amalgamated goldfields company, sheepshead line, central blue, big blue, mines dept special edition australian mining standard 1.6.1899, mines dept booklet bendigo goldfield 1936, annals of bendigo mining sections 1876 - 1921, a richardson -
 Bendigo Historical Society Inc.
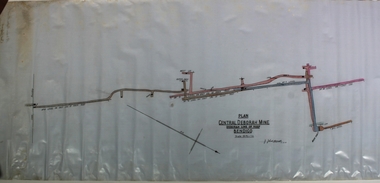
Plan - Central Deborah Gold Mine, J.J. Caldwell, 1945
... It was listed on the Victorian Heritage Register on 18 November 1999.[1] The mine was opened in 1939 by the Central Deborah Gold Mining Company during a 1930s revival of the gold industry, extending an existing 108 ft shaft from many years earlier with new machinery. It was one of the last mines to open on the Bendigo goldfields and one of the few to stay open during World War II. ...It was listed on the Victorian Heritage Register on 18 November 1999.[1] The mine was opened in 1939 by the Central Deborah Gold Mining Company during a 1930s revival of the gold industry, extending an existing 108 ft shaft from many years earlier with new machinery. It was one of the last mines to open on the Bendigo goldfields and one of the few to stay open during World War II. ...The Central Deborah Gold Mine is situated at 76 Violet Street, Bendigo. The mine operated from 1939 through to 1954 and extracted 929 kg of gold. The Central Deborah Gold Mine is a non-active gold mine and tourist attraction in Bendigo, Australia. It was listed on the Victorian Heritage Register on 18 November 1999.[1] The mine was opened in 1939 by the Central Deborah Gold Mining Company during a 1930s revival of the gold industry, extending an existing 108 ft shaft from many years earlier with new machinery. It was one of the last mines to open on the Bendigo goldfields and one of the few to stay open during World War II. It was expanded during 1945–46, with extensions and new machinery. It reached its maximum depth (now recorded as 412m) during the 1940s. It closed in November 1954, having produced 29,865 ounces of gold in its lifetime; the closure of the North Deborah Mine two weeks later marked the last mine in Bendigo to close Central Deborah Gold Mine is now a tourist destination, operated by Bendigo Heritage Attractions: https://www.central-deborah.com/about-us/central-deborah-gold-mine-s-history Blue waxed paper, features on plan drawn in pale pink and blue, title written in black text on centre bottom: 'Plan, Central Deborah Mine, Deborah Line of Reef, Bendigo, Scale 30 ft = 1 in.' Signature of J.J. Caldross, 13.10.45, written below name of mine. Handwritten on outside of plan in black pen: 'Mines Department, Cent. Deborah, Transverse section, Plan of levels' Plan notation shows No. 8 level on east leg of inner reef, level of east leg on outer reef, outer back, west leg, main shaft, numbers 5, 6, 7 and 10 levels. Mine map is part of the Margaret Roberts Collection. gold mining, gold, margaret roberts collection, central deborah gold mine, violet street, tourist attraction, bendigo -
 Flagstaff Hill Maritime Museum and Village
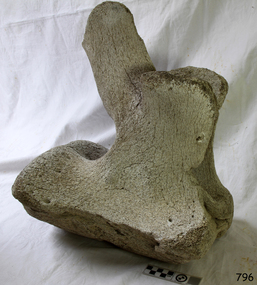
Animal specimen - Whale bone, Undetermined
... early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. ...early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. ...Prior to carrying out a detailed condition report of the cetacean skeletons, it is useful to have an understanding of the materials we are likely to encounter, in terms of structure and chemistry. This entry invites you to join in learning about the composition of whale bone and oil. Whale bone (Cetacean) bone is comprised of a composite structure of both an inorganic matrix of mainly hydroxylapatite (a calcium phosphate mineral), providing strength and rigidity, as well as an organic protein ‘scaffolding’ of mainly collagen, facilitating growth and repair (O’Connor 2008, CCI 2010). Collagen is also the structural protein component in cartilage between the whale vertebrae and attached to the fins of both the Killer Whale and the Dolphin. Relative proportions in the bone composition (affecting density), are linked with the feeding habits and mechanical stresses typically endured by bones of particular whale types. A Sperm Whale (Physeter macrocephalus Linnaeus, 1758) skeleton (toothed) thus has a higher mineral value (~67%) than a Fin Whale (Balaenoptera physalus Linnaeus, 1758) (baleen) (~60%) (Turner Walker 2012). The internal structure of bone can be divided into compact and cancellous bone. In whales, load-bearing structures such as mandibles and upper limb bones (e.g. humerus, sternum) are largely composed of compact bone (Turner Walker 2012). This consists of lamella concentrically deposited around the longitudinal axis and is permeated by fluid carrying channels (O’Connor 2008). Cancellous (spongy) bone, with a highly porous angular network of trabeculae, is less stiff and thus found in whale ribs and vertebrae (Turner Walker 2012). Whale oil Whales not only carry a thick layer of fat (blubber) in the soft tissue of their body for heat insulation and as a food store while they are alive, but also hold large oil (lipid) reserves in their porous bones. Following maceration of the whale skeleton after death to remove the soft tissue, the bones retain a high lipid content (Higgs et. al 2010). Particularly bones with a spongy (porous) structure have a high capacity to hold oil-rich marrow. Comparative data of various whale species suggests the skull, particularly the cranium and mandible bones are particularly oil rich. Along the vertebral column, the lipid content is reduced, particularly in the thoracic vertebrae (~10-25%), yet greatly increases from the lumbar to the caudal vertebrae (~40-55%). The chest area (scapula, sternum and ribs) show a mid-range lipid content (~15-30%), with vertically orientated ribs being more heavily soaked lower down (Turner Walker 2012, Higgs et. al 2010). Whale oil is largely composed of triglycerides (molecules of fatty acids attached to a glycerol molecule). In Arctic whales a higher proportion of unsaturated, versus saturated fatty acids make up the lipid. Unsaturated fatty acids (with double or triple carbon bonds causing chain kinks, preventing close packing (solidifying) of molecules), are more likely to be liquid (oil), versus solid (fat) at room temperature (Smith and March 2007). Objects Made From the Whaling Industry We all know that men set forth in sailing ships and risked their lives to harpoon whales on the open seas throughout the 1800s. And while Moby Dick and other tales have made whaling stories immortal, people today generally don't appreciate that the whalers were part of a well-organized industry. The ships that set out from ports in New England roamed as far as the Pacific in hunt of specific species of whales. Adventure may have been the draw for some whalers, but for the captains who owned whaling ships, and the investors which financed voyages, there was a considerable monetary payoff. The gigantic carcasses of whales were chopped and boiled down and turned into products such as the fine oil needed to lubricate increasing advanced machine tools. And beyond the oil derived from whales, even their bones, in an era before the invention of plastic, was used to make a wide variety of consumer goods. In short, whales were a valuable natural resource the same as wood, minerals, or petroleum we now pump from the ground. Oil From Whale’s Blubber Oil was the main product sought from whales, and it was used to lubricate machinery and to provide illumination by burning it in lamps. When a whale was killed, it was towed to the ship and its blubber, the thick insulating fat under its skin, would be peeled and cut from its carcass in a process known as “flensing.” The blubber was minced into chunks and boiled in large vats on board the whaling ship, producing oil. The oil taken from whale blubber was packaged in casks and transported back to the whaling ship’s home port (such as New Bedford, Massachusetts, the busiest American whaling port in the mid-1800s). From the ports it would be sold and transported across the country and would find its way into a huge variety of products. Whale oil, in addition to be used for lubrication and illumination, was also used to manufacture soaps, paint, and varnish. Whale oil was also utilized in some processes used to manufacture textiles and rope. Spermaceti, a Highly Regarded Oil A peculiar oil found in the head of the sperm whale, spermaceti, was highly prized. The oil was waxy, and was commonly used in making candles. In fact, candles made of spermaceti were considered the best in the world, producing a bright clear flame without an excess of smoke. Spermaceti was also used, distilled in liquid form, as an oil to fuel lamps. The main American whaling port, New Bedford, Massachusetts, was thus known as "The City That Lit the World." When John Adams was the ambassador to Great Britain before serving as president he recorded in his diary a conversation about spermaceti he had with the British Prime Minister William Pitt. Adams, keen to promote the New England whaling industry, was trying to convince the British to import spermaceti sold by American whalers, which the British could use to fuel street lamps. The British were not interested. In his diary, Adams wrote that he told Pitt, “the fat of the spermaceti whale gives the clearest and most beautiful flame of any substance that is known in nature, and we are surprised you prefer darkness, and consequent robberies, burglaries, and murders in your streets to receiving as a remittance our spermaceti oil.” Despite the failed sales pitch John Adams made in the late 1700s, the American whaling industry boomed in the early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. The machine tools that made the growth of industry possible in the United States were lubricated, and essentially made possible, by oil derived from spermaceti. Baleen, or "Whalebone" The bones and teeth of various species of whales were used in a number of products, many of them common implements in a 19th century household. Whales are said to have produced “the plastic of the 1800s.” The "bone" of the whale which was most commonly used wasn’t technically a bone, it was baleen, a hard material arrayed in large plates, like gigantic combs, in the mouths of some species of whales. The purpose of the baleen is to act as a sieve, catching tiny organisms in sea water, which the whale consumes as food. As baleen was tough yet flexible, it could be used in a number of practical applications. And it became commonly known as "whalebone." Perhaps the most common use of whalebone was in the manufacture of corsets, which fashionable ladies in the 1800s wore to compress their waistlines. One typical corset advertisement from the 1800s proudly proclaims, “Real Whalebone Only Used.” Whalebone was also used for collar stays, buggy whips, and toys. Its remarkable flexibility even caused it to be used as the springs in early typewriters. The comparison to plastic is apt. Think of common items which today might be made of plastic, and it's likely that similar items in the 1800s would have been made of whalebone. Baleen whales do not have teeth. But the teeth of other whales, such as the sperm whale, would be used as ivory in such products as chess pieces, piano keys, or the handles of walking sticks. Pieces of scrimshaw, or carved whale's teeth, would probably be the best remembered use of whale's teeth. However, the carved teeth were created to pass the time on whaling voyages and were never a mass production item. Their relative rarity, of course, is why genuine pieces of 19th century scrimshaw are considered to be valuable collectibles today. Reference: McNamara, Robert. "Objects Made From the Whaling Industry." ThoughtCo, Jul. 31, 2021, thoughtco.com/products-produced-from-whales-1774070.Whale bone was an important commodity, used in corsets, collar stays, buggy whips, and toys.Whale bone vertebrae. Advanced stage of calcification as indicated by deep pitting. Off white to grey.Noneflagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, whales, whale bone, corsets, toys, whips, whalebone -
 Flagstaff Hill Maritime Museum and Village
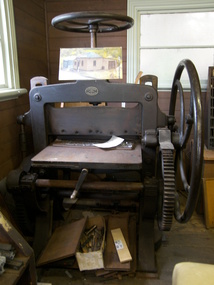
Machine - Guillotine, c. 1880's
... early model of a guillotine was patented in 1837 by Thirault, who built a model with a fixed blade. Guillotines similar in principal to this one were patented by Guillaume Massiquot in 1844 and 1852. Over the years many improvements have been made and operation has moved from man power to electricity. Oscar Friedheim Ltd. was the importer and wholesaler of a large range of machinery...early model of a guillotine was patented in 1837 by Thirault, who built a model with a fixed blade. Guillotines similar in principal to this one were patented by Guillaume Massiquot in 1844 and 1852. Over the years many improvements have been made and operation has moved from man power to electricity. Oscar Friedheim Ltd. was the importer and wholesaler of a large range of machinery ...This guillotine is a hand operated machine specifically designed to cut through multiple sheets of paper or card. It has a very heavy and sharp single blade knife mounted between vertical guides or runners. The main users of a machine like this is in by the printing and publication binding industry. Book binding companies use a guillotine to evenly trim the pages of a book after it has been bound. The way the guillotine is used is - paper or card is stacked squarely on the flat table and pushed firmly against the back guide - the handle below the table at the front of the machine is wound around, which brings the back guide forward, pushing the paper stack forward and positioning the centre of the stack below the vertical frame - the upper wheel is wound around, which brings the clamp and firmly in position on top of the paper, to hold it very firmly - the large wheel on the side of the machine is turned around to lower the long sharp blade down onto the pages and cut them through. The sharp edge of the blade is protected somewhat from becoming blunt; a block of wood sits in the table under the stack of paper An early model of a guillotine was patented in 1837 by Thirault, who built a model with a fixed blade. Guillotines similar in principal to this one were patented by Guillaume Massiquot in 1844 and 1852. Over the years many improvements have been made and operation has moved from man power to electricity. Oscar Friedheim Ltd. was the importer and wholesaler of a large range of machinery and equipment for the printing and bookbinding industry. He sold most of his equipment under his own name. On this guillotine or paper cutter he refers to the origin of the guillotine’s manufacture only as “German Manufacrure”. A reference book “Commercial Bookbinding: a description of the processes and the various machines used" by Geo. Stephen, 1910, recommends Oscar Friedheim, amongst others, for the supply of “reliable cutting machines for hand or power”. It also recommends Oscar Friedheim’s for a wide range of other printing machinery and processes. OSCAR FRIEDHEIM LIMITED, LONDON Oscar Friedheim Ltd. was established in 1884 and operated from Ludgate in London. The company was an importer and wholesale supplier in the 1880’s, offering machinery and equipment for the printing and packaging industry for the UK and Ireland. The company became incorporated in 1913. An advertisement of 1913 includes a telegraphic code plus two telephone numbers for Oscar Friedheim Ltd and invites readers to call at the Ludgate, London, showrooms to see the machines working. The company later became Friedheim International Ltd. The book titled “Friedheim, A Century of Service 1884-1984 by Roy Brewer, celebrates Oscar Friedheim’s achievements. Friedheim International currently operates from Hemel Hempstead, on the northern outskirts of London UK. It promotes itself as “… the leading supplier of finishing, converting and packaging machinery to the printing, graphic arts, and highly varied packaging industries in the UK and Ireland. The company’s policy is simple – “employ the best people, work with the best equipment manufacturers in the world, and treat our customers as partners!” The company still sells guillotines. The guillotine is significant for its ability to represent aspects of the printing trade in Warrnambool and in a typical port town circa 1850 to 1910. It represents communication methods and processes used in the time before electrically powered equipment became common in industry.Guillotine (or paper cutter), hand operated. Metal framework with vertical guides, stand and metal mechanical parts including wheels and gears. Table with back guide; handle below front of table winds to move the back guide. A wheel at top of machine winds to adjust pressure of the clamp on the work on the table below it. The cutting blade fits between vertical guides; a timber insert in the table below the blade helps minimise the loss of sharpness of the blade. A handle on the side of the machine turns a large spoked wheel, which rotates a large gear, causing the blade to move up and down. Makers details are on a small oval plaque with embossed maker’s details is screwed onto main body. Maker is O Friedheim, London, and the machine is of German manufacture, circa late 1880’s.Maker’s plaque inscribed "O. FRIEDHEIM / London / German Manufacture"flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, printing machinery, printer’s guillotine, paper guillotine, paper cutter machine, oscar friedheim ltd london, friedheim international ltd, bookbinding industry, printing industry -
 Flagstaff Hill Maritime Museum and Village
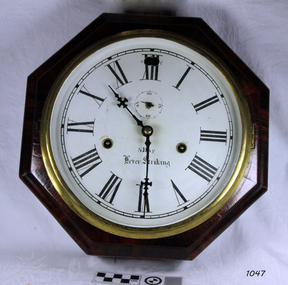
Clock, 1867-1870
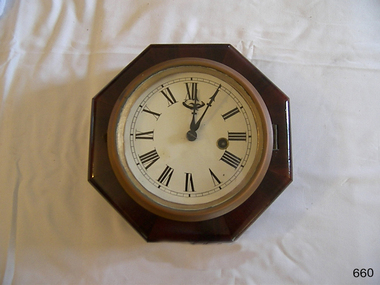
... early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery...early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery ...Chauncey Jerome (1793–1868) was an American clock maker in the early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery. Deciding to go into business for himself, Jerome began to make cases, trading them to Terry for wooden movements. In 1822 Jerome moved his business to Bristol New Haven, opening a small shop with his brother Noble and began to produce a 30-hour and eight-day wooden clocks. By 1837 Jerome's company was selling more clocks than any of his competitors. A one-day wood-cased clock, which sold for six dollars had helped put the company on the map. A year later his company was selling that same clock for four dollars. The company also sold one line of clocks at a wholesale price of 75 cents and by 1841 the company was showing an annual profit of a whopping $35,000, primarily from the sale of its brass movements. In 1842 Jerome moved his clock-case manufacturing operation to St. John Street in New Haven. Three years later, following a fire that destroyed the Bristol plant, Jerome relocated the entire operation to Elm City factory. Enlarging the plant, the company soon became the largest industrial employer in the city, producing 150,000 clocks annually. In 1850 Jerome formed the Jerome Manufacturing Co. as a joint-stock company with Benedict & Burnham, brass manufacturers of Waterbury. In 1853 the company then became known as the New Haven Clock Co, producing 444,000 clocks and timepieces annually, then the largest clock maker in the world. Jerome's future should have been secure but in 1855 he bought out a failed Bridgeport clock company controlled by P.T. Barnum, which wiped him out financially, leaving the Jerome Manufacturing Co. bankrupt. Jerome never recovered from the loss. By his admission, he was a better inventor than a businessman. When Jerome went bankrupt in 1856 the New Haven Clock Company purchased the company. One of the primary benefits of Jerome purchasing New Haven in the first place was the good reputation of the Jerome brand and the network of companies that remained interested in selling its clocks. In England, Jerome & Co. Ltd. sold Jerome clocks for the New Haven company until 1904, when New Haven purchased the English firm outright. After his involvement with the New Haven Company in 1856, Jerome traveled from town to town, taking jobs where he could, often working for clock companies that had learned the business of clock making using Jerome's inventions. On returning to New Haven near the end of his life, he died, penniless, in 1868 at the age of 74. The company struggled on after Jerome's bankruptcy until after World War II, when the company endeavored to continue through disruptions caused by a takeover along with poor sales, finally having to fold its operations in 1960 a little more than 100 years after it had been founded. The item is significant as it is associated with Chauncey Jerome who had made a historic contribution to the clock making industry during the 19th century when he began to substitute brass mechanisms for wooden mechanisms in his clocks. This was said to be the greatest and most far-reaching contribution to the clock industry. Because of his discovery of stamping out clockwork gears rather than using castings, Jerome was producing the lowest-priced clocks in the world. That can only add to his significance as the major clock manufacture of the 19th century. Jerome may have made and lost, a fortune selling his clocks but was perhaps the most influential and creative person associated with the American clock business during the mid-19th century. Also, he had served his community as a legislator in 1834, a Presidential elector in 1852 and mayor of New Haven, Connecticut from 1854 to 1855.Clock, marine, in octagonal rosewood veneer case. Roman numerals to dial, has a seconds dial. 2 key-winding holes slow-to-Fast adjustment pin through dial. Small lever in lower edge of case activates a chime. "8 day, 8 inch, Lever Striking escarpment " Paper label on the back of the clock "Jerome & Co, New Haven, Conn" "Manufacturers of every variety of Office and Home Clocks and Time Pieces".flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, clock, jerome & co, new haven, clock maker, chauncey jerome -
 Flagstaff Hill Maritime Museum and Village
Clock, 1867-1870
... early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery...early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery ...Chauncey Jerome (1793–1868) was an American clock maker in the early to mid 19th century. He made a fortune selling his clocks, and his business grew quickly. Jerome was born in Canaan USA in 1793 son of a blacksmith and nail-maker. He began his career in Plymouth, making dials for long-case clocks where he learned all he could about clocks, particularly clock cases, and then went to New Jersey to make seven-foot cases for clocks mechanisms. In 1816 he went to work for Eli Terry making "Patent Shelf Clocks," learning how to make previously handmade cases using machinery. Deciding to go into business for himself, Jerome began to make cases, trading them to Terry for wooden movements. In 1822 Jerome moved his business to Bristol New Haven, opening a small shop with his brother Noble and began to produce a 30-hour and eight-day wooden clocks. By 1837 Jerome's company was selling more clocks than any of his competitors. A one-day wood-cased clock, which sold for six dollars had helped put the company on the map. A year later his company was selling that same clock for four dollars. The company also sold one line of clocks at a wholesale price of 75 cents and by 1841 the company was showing an annual profit of a whopping $35,000, primarily from the sale of its brass movements. In 1842 Jerome moved his clock-case manufacturing operation to St. John Street in New Haven. Three years later, following a fire that destroyed the Bristol plant, Jerome relocated the entire operation to Elm City factory. Enlarging the plant, the company soon became the largest industrial employer in the city, producing 150,000 clocks annually. In 1850 Jerome formed the Jerome Manufacturing Co. as a joint-stock company with Benedict & Burnham, brass manufacturers of Waterbury. In 1853 the company then became known as the New Haven Clock Co, producing 444,000 clocks and timepieces annually, then the largest clock maker in the world. Jerome's future should have been secure but in 1855 he bought out a failed Bridgeport clock company controlled by P.T. Barnum, which wiped him out financially, leaving the Jerome Manufacturing Co. bankrupt. Jerome never recovered from the loss. By his admission, he was a better inventor than a businessman. When Jerome went bankrupt in 1856 the New Haven Clock Company purchased the company. One of the primary benefits of Jerome purchasing New Haven in the first place was the good reputation of the Jerome brand and the network of companies that remained interested in selling its clocks. In England, Jerome & Co. Ltd. sold Jerome clocks for the New Haven company until 1904, when New Haven purchased the English firm outright. After his involvement with the New Haven Company in 1856, Jerome traveled from town to town, taking jobs where he could, often working for clock companies that had learned the business of clock making using Jerome's inventions. On returning to New Haven near the end of his life, he died, penniless, in 1868 at the age of 74. The company struggled on after Jerome's bankruptcy until after World War II, when the company endeavored to continue through disruptions caused by a takeover along with poor sales, finally having to fold its operations in 1960 a little more than 100 years after it had been founded. The item is significant as it is associated with Chauncey Jerome who had made a historic contribution to the clock making industry during the 19th century when he began to substitute brass mechanisms for wooden mechanisms in his clocks. This was said to be the greatest and most far-reaching contribution to the clock industry. Because of his discovery of stamping out clockwork gears rather than using castings, Jerome was producing the lowest-priced clocks in the world. That can only add to his significance as the major clock manufacture of the 19th century. Jerome may have made and lost, a fortune selling his clocks but was perhaps the most influential and creative person associated with the American clock business during the mid-19th century. Also, he had served his community as a legislator in 1834, a Presidential elector in 1852 and mayor of New Haven, Connecticut from 1854 to 1855.Eight day movement wall clock with Roman numerals, octagonal shaped rosewood veneered casing, hinged face with locking clip. Wound from front. Face has adjustment for Fast-to-Slow.Part paper label on back of case can just make out "Jerome" and "ight and One" probable meaning is "Eight and One Day" describing the movements operational time between winding the mechanism.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, clock maker, jerome & co, new haven, chauncey jerome, canaan -
 Flagstaff Hill Maritime Museum and Village
Container - Ink bottle, MABIE TODD & Co. (Aust.) Pty. Ltd, Second half of 19th Century or first half of the 20th Century
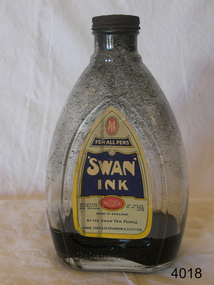
... early in the Second World War. Its prestigious Sunderland House headquarters was destroyed during the blitz, followed by destruction of its main factory in Harlesden, North London. Some machinery...early in the Second World War. Its prestigious Sunderland House headquarters was destroyed during the blitz, followed by destruction of its main factory in Harlesden, North London. Some machinery ...A Brief History Of Mabie Todd Ltd The company originated in America from the beginnings during the 1860s when a Mr. Todd and a Mr. Mabie began making pencil cases and pen holders in New York. Later they were joined by the Bard Brothers who made Gold nibs and by 1873 the company of Mabie Todd and Bard were established in New York. By 1878 the first patent was filed for the design and manufacture of a fountain pen, achieved under the design leadership of one William Washington Stewart. The first Swan fountain pen followed just 6 years later in 1884 with an over-under feed with ink delivery assisted by a twisted silver wire. This same year an office had been established in the UK with a showroom in Cheapside, London. The UK was being supplied with a steadily increasing supply of pens from New York and by 1905 new, larger showrooms were established in High Holborn. By this time the Swan pen had become synonymous with fountain pens at large. In 1906 the name of Bard was dropped in the US and the UK company subsequently adopted the title Mabie Todd & Co. New York. In 1907 British production began, using imported nibs from New York and whilst the company in the UK flourished, the business in the US started to diminish under stiff competition from new manufacturers.. By 1915 manufacturing was doing well in England from a factory in Weston Street, London and the New York company agreed to sell the rights to all European and Colonial business to Mabie Todd & Company Ltd of England. From then onwards, the development of the range mostly followed, rather than led the interests of the markets they were supplying. Even during the First World War the business continued to flourish. with factories in both London and Liverpool. At the end of 1919 a new expansion plan saw the establishment of a new Headquarters in Oxford Street, London. Throughout this period, some components were continuing to be imported from America, but gradually these diminished and during the 20s and 30s manufacturing facilities were expanded and by the end of the 1930s Mabie Todd were in full production, manufacturing pens in its London factory, gold nibs in Birmingham and ink in Liverpool. Another new headquarters grew out of this period of abundance and market domination. when in 1936 they moved into Sunderland House in Mayfair, London, a highly prized mansion building. Disaster struck early in the Second World War. Its prestigious Sunderland House headquarters was destroyed during the blitz, followed by destruction of its main factory in Harlesden, North London. Some machinery was saved and able to be used at another factory premises in the City, but like many other 'non essential' manufacturing, the main production was centred on wartime components such as rocket fuses and ammunition. After The War, in 1945 they moved out of their City premises to Park Royal and eventually in 1946 proper fountain pen production was resumed. In 1948 the company decided to go public. But at the time they had no plans to enter into the market for the now growing interest in ballpoint pens, the result was the beginning of their slide into obscurity and subsequent demise. They became Biro Swan in 1952 following a large share purchase by Biro Pens. Even though at this time they had just launched their new high profile Calligraph range to join the competition for the new market associated with a craze for italic writing, fountain pen manufacture under the new company was to suffer a lack of real support. The restyled ranges of 1956 failed to ignite market interest and with diminishing quality, the end of the Mabie Todd story was inevitable. After 80 years of Swan pens, the book was closed.This bottle of ink would have been supplied to schools. After a child was deemed old enough to progress from just using slate and board, he/she would have been supplied with a pen shaft made of wood and with a very basic metal nib. The ink bottle would be used to fill up the individual inkwells. This operation would have been conducted by the teacher him/herself, or by an older pupil under the close eye of the teacher.Ink bottle clear glass with 'Swan Ink' paper label. Has rusted screw on top & black ink inside.Label has 'Mabel Todd' manufacturer's logo at top,; 'Swan Ink' name clearly shown; 'Made in England' printed clearly; and 'Mable Todd & Co Ltd, London & Liverpool' printed at base of label.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, ink, bottle, mabie todd ltd -
 Flagstaff Hill Maritime Museum and Village
Machine - Treadle Lathe, 1920-1923
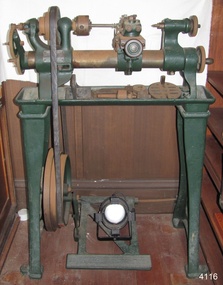
... early example of a lathe that was designed primarily for the hobbyist model maker. It is in good condition and sought today by collectors as many of it's attributes were innovative at the time and lead to further development and incorporation of some of its features into more industrial models of production machinery. flagstaff hill warrnambool shipwrecked coast flagstaff hill maritime museum maritime museum shipwreck coast flagstaff hill maritime village great ocean road lathe 1920-1923 round bed lathe treadle lathe drummond type a guildford surrey drummond brothers guildford surrey england tread'e "MADE BY DRUMMOND BROTHERS LIMITED - PATENT TEES - RYDE'S HILL n GUILDFORD SURREY", "Serial Number 01470," "L44" or "L45 " Lathe, round bed, treadle powered lathe, Drummond Type A, Serial number and maker's inscription. 1920-1923, Made by Drummond Brothers in Guildford, Surrey, England. ...The lathe-making business incorporated in 1902 as Drummond Bros Ltd originated in the fertile mind of Mr Arthur Drummond, said to have been living at that time at Pinks Hill, on the southern edge of Broad Street Common, west of Guildford. Mr Drummond, whose accomplishments included several pictures hung in the Royal Academy, was unable to find a lathe suitable for use in model engineering. In 1896 he designed for himself a ‘small centre lathe … which had a compound slide rest with feed-screws and adjustable slides’. He also designed and built ‘lathes of 4.5 inch and 5 inch centre height, which had beds of a special form whereby the use of a gap piece was eliminated but the advantages of a gap-bed lathe were retained’. Assisted by his brother, Mr Frank Drummond, who had served an apprenticeship to an engineering firm at Tunbridge Wells, the first lathes were made in a workshop adjoining Arthur Drummond’s house. The demand that speedily built up led to the decision to form a company and manufacture the lathes for sale commercially. Land was acquired nearby, at Rydes Hill, and the first factory built. The enterprise was a success, and the company quickly established ‘a high reputation in this country and abroad for multi-tool and copying lathes, and gear-cutting machines’. Other lathes were added to the range, including the first of the ’round bed’ machines for which the firm became widely known. A Drummond 3.5 inch lathe was among the equipment of Captain Scott’s 1912 expedition to the South Pole, and large numbers of 3.5 inch and 4 inch designs were exported to Australia, Canada and India. By the outbreak of war in 1914, 5 inch, 6 inch and 7 inch screw cutting lathes, arranged for power drive, were on sale. Large orders were received from the government for 3.5 inch lathes, for use in destroyers and submarines, and 5 inch lathes for the mechanised section of the Army Service Corps. The latter were used in mobile workshops. The factory worked night and day to supply the forces’ needs, until production was disrupted by a fire which destroyed a large part of the works in May 1915. As soon as rebuilding was complete work restarted. At the end of the war the entire production was being taken by the Government departments, a special feature being a precision screw lathe, bought by the Ministry of Munitions in 1918. Between the wars Drummond Bros Ltd introduced new machines for the motor vehicle, and later the aircraft industry, and the works were extended on many occasions to fulfill the increasing orders. The Maxicut multi-tool lathe (1925), designed for high-production turning operations, was one of the first machines of this type to be built in England. It was followed (1928) by an hydraulic version for turning gear blanks, and similar work. Further developments provided machines which, during the Second World War, turned all the crankshafts and propeller shafts for Bristol engines. Others, ordered by the Ministry of Supply were employed in turning shells, and many other specific needs of vehicle and aircraft manufacture were catered for by new types of Drummond lathes. Production of the small centre lathes ceased during the war when the company needed to concentrate on building multi-tool lathes and gear shapers. After the war a completely new Maxicut range was introduced, replacing the older versions, and fully automatic. The types were continually developed, and new versions manufactured until the end of the company’s life in 1980. The disappearance from the scene of Mr Arthur Drummond in 1946, and the end of the company’s autonomous existence in 1953 when the company was acquired by William Asquith Ltd, which was in turn bought by Staveley in 1966, meant that the factory at Rydes Hill became one – albeit very effective – part of a large national engineering company. Achievements at the Guildford works during its last years included the development of automated Maxicut gear-shapers in what was ‘probably the most fully automated gear shop in the country’, while a machine from Guildford was sent to the Osaka Fair in 1962. In 1963 an agreement was signed with Hindustan Machine Tools for the manufacture of Maxicut gear-shapers in state owned factories in Bangalore and Chandigarh. During 1963 the two largest multi-tool lathes ever made in the UK were installed in Ambrose Shardlow’s works in Sheffield for handling cranks up to 14 foot long. In 1976 Drummond lathes were included in Staveley’s £14,000,000 installation in Moscow of an automated production line for Zil motor cars. Up to the end invention continued at Guildford: a new Drummond Multi-turn memory-controlled machine was shown at the International Machine Tool Exhibition in 1977. This could not save the works from the pressures of the late 1970s, and Staveley Industries closed its Guildford site in 1980.An early example of a lathe that was designed primarily for the hobbyist model maker. It is in good condition and sought today by collectors as many of it's attributes were innovative at the time and lead to further development and incorporation of some of its features into more industrial models of production machinery. Lathe, round bed, treadle powered lathe, Drummond Type A, Serial number and maker's inscription. 1920-1923, Made by Drummond Brothers in Guildford, Surrey, England. Lathe is complete with Chuck, Tool post and Tail Stock in situ (30 extra parts)"MADE BY DRUMMOND BROTHERS LIMITED - PATENT TEES - RYDE'S HILL n GUILDFORD SURREY", "Serial Number 01470," "L44" or "L45 " flagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, lathe 1920-1923, round bed lathe, treadle lathe, drummond type a, guildford surrey, drummond brothers guildford surrey england, tread'e -
 Flagstaff Hill Maritime Museum and Village
Instrument - Foghorn, Late 19th century
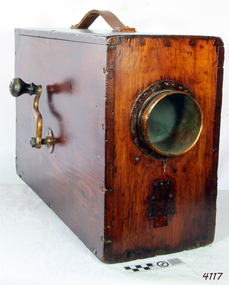
... Since the automation of lighthouses became common in the 1960s and 1970s, most older foghorn marine installations have been removed to avoid the need to run the complex machinery associated with them, and have been replaced with an electrically powered diaphragm or compressed air horns. The example in the collection is significant as it was used in the early 19th century for sailing vessels was important but these portable crank fog horns have also been superseded by modern electric varieties. ...A foghorn is a device that uses sound to warn of navigational hazards like rocky coastlines, or boats of the presence of other vessels, in foggy conditions. The term is most often used with marine transport. When visual navigation aids such as lighthouses are obscured, foghorns provide an audible warning of rocky outcrops, shoals, headlands, or other dangers to shipping. An early form of fog signal was to use a bell, gong, explosive signal or firing a cannon to alert shipping. From the early 20th century an improved device called the diaphone was used in place of these other devices, The diaphone horn was based directly on the organ stop of the same name invented by Robert Hope-Jones, creator of the Wurlitzer organ. Hope-Jones' design was based on a piston that was closed only at its bottom end and had slots, perpendicular to its axis, cut through its sides, the slotted piston moved within a similarly slotted cylinder. Outside of the cylinder was a reservoir of high-pressure air. Initially, this air would be admitted behind the piston, pushing it forward. When the slots of the piston aligned with those of the cylinder, air passed into the piston, making a sound and pushing the piston back to its starting position, whence the cycle would be repeated. This method of producing a low audible sound was further developed as a fog signal by John Northey of Toronto and these diaphones were powered by compressed air produced by an electric motor or other mechanical means that admitted extremely powerful low-frequency notes. The example in the Flagstaff collection is an early cased and portable diaphone used on pleasure or sailing craft. By manually turning the crank handle air is produced and fed into valves that direct air across vibrating metal reeds to produce the required sound. in foggy weather, fog horns are used to pinpoint a vessels position and to indicate how the vessel is sailing in foggy conditions. One blast, when sailing on starboard tack and two blasts, when sailing on a port tack and three dots, when with wind is behind the vessel. Since the automation of lighthouses became common in the 1960s and 1970s, most older foghorn marine installations have been removed to avoid the need to run the complex machinery associated with them, and have been replaced with an electrically powered diaphragm or compressed air horns. The example in the collection is significant as it was used in the early 19th century for sailing vessels was important but these portable crank fog horns have also been superseded by modern electric varieties. Therefore the item has a historical connection with sailing and maritime pursuits from our past.English Rotary Norwegian Pattern nautical foghorn within a boxed pine varnished case with exposed corner dovetailing, original leather carrying strap, brass side crank, and original copper trumped horn. Card accessory with Directions for Use in both English and French.Noneflagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, foghorn, maritime technology, maritime communication, marine warning signal, portable foghorn, bellows foghorn, crank handle, robert hope-jones, john northey -
 Flagstaff Hill Maritime Museum and Village
Equipment - Company seal embosser, Unknown
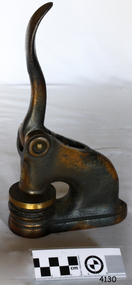
... early private company operations. It was regarded as a model mill in the late 1880s and was, from all accounts, well-planned and organised with machinery on a par with the great mills of England. ...The former Albion (West) Woollen and Worsted Mills is a functional structure which has been built in stages, possibly dating from the 1880s, with the earliest sections near to the Barwon River.The Worsted mill operated for about 50 years and at its peak employed around 500 people. In 1973 the mill merged with the British John Foster and Sons Company under some controversial stock and shareholding issues. The mill continued for a short period before closing at a time when much of the Australian textile industry was finding it difficult to compete with overseas operations. In the 30 plus years after the closure, the site was used for several ventures, including the Mill Vintage Markets and a vehicle trim manufacturing operation. In 2011 the site was purchased by Little Creatures of Western Australia to become their main brewery for the eastern states of Australia. Now owned by the Lion Group, Little Creatures started their 60 million dollar transformation of the old mill in 2012. Finally, in 2013 these former walls of industry were soon rattling away to the sounds of a different type of industry, as the first bottles of beer made their way out of the Geelong Little Creatures Brewery. The remaining building of the former Albion Woollen and Worsted Mills has historical significance as one of Geelong's major woollen mills. The venture has operated on the same site for more than a century. The Albion Woollen Mill was one of the four key sites along with Victoria, Barwon and Union Mills that was established in the late 1860s to mid-1870s. These mills were in constant operation on the west side of the Barwon Bridge over the last century and led to Geelong's fame as milling and scouring locality. The Albion Mill was probably the most successful survivor of the early private company operations. It was regarded as a model mill in the late 1880s and was, from all accounts, well-planned and organised with machinery on a par with the great mills of England. It produced high-quality tweeds. Together with the (now demolished) Union Mill it was regarded as the borough's principal industry over the 1870-1900 period and was one of Australia's most significant producers of tweed by 1900. These two mills were more successful, competitive and long-lived than the Barwon and Victoria Mills. The remaining building form is an important reminder of the private ventures of both the Albion and Union Mills and represents a key site of spinning, carding and finishing as well as scouring and dying that occurred in the lower section near to the river. The loss of the adjacent former Union Mill is unfortunate because the complex, together with the former Collins Union Mill office building, was an important reminder of the success of these industries and the reputation they earned for the Geelong region as a centre for quality textile products. Company seal embosser hand operated matte black & brass colour Western District Worsted Mills emblem on frontflagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village -
 Flagstaff Hill Maritime Museum and Village
Machine - Diving Compressor, Siebe Gorman & Co. Ltd, 1880-1890
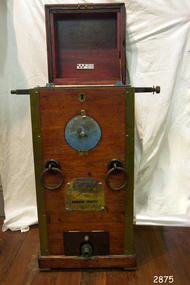
... , measuring machinery, water-pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on, and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ..., measuring machinery, water-pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on, and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ...This compressor was part of the E.G. Ward Collection. It is connected to the diving suit and boots, also in our collection. Siebe Gorman & Company Ltd was a British company that developed diving equipment and breathing equipment and worked on commercial diving and marine salvage projects. The company advertised itself as 'Submarine Engineers'. It was founded by Augustus Siebe, a German-born British engineer chiefly known for his contributions to diving equipment. Siebe Gorman traded as an engineering firm for over 180 years, from 1819 to 1999. The early success of the business was due to its founder, the Prussian immigrant Christian 'Augustus' Siebe (1788-1872). For business reasons, he applied for and was granted British citizenship in 1856. He was a gifted engineer who was able to translate theoretical problems into practical, working products. During the industrial Victorian period, the business traded as 'A. Siebe's at 145 High Street, Holborn, London, but in 1828, new premises were acquired at 5 Denmark Street, Soho. The family firm produced a wide range of manufactured goods, including paper-making machinery, measuring machinery, water-pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on, and the company gained a reputation for the manufacture of safe, reliable diving apparatus. Augustus Siebe is best remembered for the development and manufacture of the ‘closed’ Diving Dress based on the ideas of Charles and John Deane, George Edwards and Charles Pasley. Apart from some small modifications to valves and diver communications, the basic 12 bolt ‘closed’ diving dress remained relatively unchanged after the 1870s. Later company successes were also based on innovation, with new products that could be successfully developed and manufactured to high standards. This was largely attributed to the inventive nature, foresight, engineering and entrepreneurial skills of Robert Henry Davis (1870-1965). In 1882, RH Davis joined the company of 'Siebe & Gorman' as a young 11-year-old office boy, and he was to remain with the company until he died in 1965. Augustus Siebe retired in 1869 and handed over the company to a new partnership of Henry H. Siebe (1830-1885) and William A. O'Gorman (1834-1904). The new firm traded as 'Siebe & Gorman' (1870-1879) from premises in and around Mason Street, Westminster Bridge Road, Lambeth, London. The two partners soon recognised the potential of R.H. Davis, and in 1894, aged 24, he became General Manager of Siebe & Gorman. Davis increasingly ran the company until the surviving partner (W.A. Gorman) died in 1904. The firm was disposed of to the Vickers (armaments) family, and a new company, Siebe Gorman & Co. Ltd. (1905-1998) was formed. Under the chairmanship of Albert Vickers, R.H. Davis was kept on as Managing Director, and the company forged ahead. However, after WW1, the Great Depression caused manufacturing output and share prices to slump. In 1924, Robert Davis made a deal with the Vickers Board and acquired control of the company through majority shares. Under his leadership, the Siebe Gorman Company flourished, and in time, four of his sons also joined the firm. The company gained a worldwide reputation for the manufacture of diving apparatus, decompression and observation chambers, and safety breathing apparatus of all types for use on the land, in the air and under the sea (including mine rescue, tunnelling, aircraft, diving, submarine escape and in other hazardous environments). Close research and development links with the MOD (especially the Admiralty), also provided a lucrative outlet for the company's products. In 1932, Robert Davis was knighted by King George V, principally for his invention of the ‘Davis Submerged Escape Apparatus’ (D.S.E.A.). Siebe Gorman essentially remained a family firm from the beginning (under A Siebe) until it became a public company for the first time in 1952. However, following WW2, British manufacturing stagnated through stifled investment and post-war austerity, and there was little innovation. Siebe Gorman's fortunes began to decline as an ageing Sir Robert Davis failed to invest or change the company's business and management practices. In 1959, Siebe Gorman was acquired by the “Fairy Group” and the ailing Sir Robert was made Life President. Consequently, nothing changed, and the slow decline continued until Sir Robert's death in March 1965. Around 1960, Siebe Gorman acquired the diving apparatus manufacturer C E Heinke, and for a brief period, it manufactured some diving equipment under the combined name of Siebe Heinke. Around 1964, Mr E. 'Barry' Stephens was appointed as the new Managing Director to modernise Siebe Gorman. Changes were made, including a move to a new factory in Wales in 1975. The new company concentrated on firefighting breathing apparatus and escape equipment, and the move coincided with the loss of many of the older, traditional craft skills. Between 1985 and 1998, Siebe expanded through acquisitions, and several other companies were acquired. The Siebe Gorman (diving apparatus) company has therefore traded as A. Siebe (1819-1870); Siebe & Gorman (1870-1879); Siebe Gorman & Co (1880-1904); Siebe Gorman & Co. Ltd (1905-1998).The diving compressor, along with associated equipment in the Flagstaff Hill collection, represents a highly significant snapshot of marine history. These items are particularly important in understanding the evolution of diving equipment, with a special focus on their use in salvage operations before and throughout the Second World War. Manufactured by a company renowned for its inventions, development, and innovation in marine engineering, the equipment demonstrates the progression of technology in deep-sea diving. Early helmets and related items produced by this company remain highly sought after by collectors worldwide, highlighting their historical and technological value. The presence of these items within the Flagstaff Hill Maritime Museum allows for a unique insight into the working conditions and methods employed by divers. It also illustrates the considerable dangers they faced while performing such essential and hazardous work, underscoring the critical role played by these professionals in maritime history.A single cylinder divers' pump by Siebe Gorman & Co Ltd, London, eccentric hand cranked in brass, brass-mounted mahogany case with instructions to the underside of the lid, brass-covered pressure gauge and air outlet, brass maker's plaque to the front, water inlet and outlet to the rear, green-painted lifting rings. Machinery has some blue-painted areas on the metal. This compressor is part of the E.G. Ward Collection.Plate on the back 'WATER SUPPLY" "WATER OVERFLOW" "WATER DRAIN-IN" Pressure gauge dial "BOURDON'S PRESSURE GAUGE" STEBE GORMAN & CO. LONDON", "LBS PRESSURE" "FEET OF SALT WATER" Plate on the front " PATENT, Siebe Gorman & Co Ltd Submarine Engineers" below emblem (Lion, Crown, Horse)flagstaff hill, warrnambool, flagstaff-hill, maritime-museum, diving compressor, london, siebe gorman & co ltd, marine technology, life saving, deep sea diving, maritime museum, maritime village, manine history, maritime history, marine engineers, marine diving, deep-sea diving, e g ward, vintage diving compressor, e. g. ward, e.g. ward, edward ward, ted ward -
 Flagstaff Hill Maritime Museum and Village
Tyre Bender, 1884
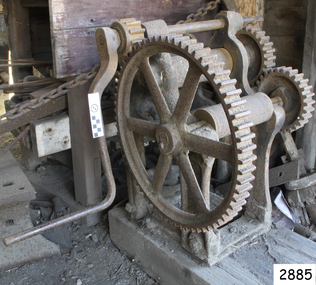
... The Day Bros foundry, makers of this tyre bender, was operating as the manufacture of wheel right and blacksmith tools and general machinery in the 19th century in the USA and successfully exported their goods all over the world. Wagon tyre benders would have been very common circa 1850-1920, so there were probably many makers over the years. Early...The Day Bros foundry, makers of this tyre bender, was operating as the manufacture of wheel right and blacksmith tools and general machinery in the 19th century in the USA and successfully exported their goods all over the world. Wagon tyre benders would have been very common circa 1850-1920, so there were probably many makers over the years. Early ...A tyre bender is used to bend and shape metal rims for wooden wagon wheels. This tyre bender’s model first appeared in the Day Bros catalogue in 1884 as the “Giant” model. The catalogue of 1883 only showed a lighter duty model called the “Lion”. It can be assumed that this later “Giant” model was a heavy duty improvement over the 1883 "Lion" and other smaller models which were still being advertised for sale in 1884. The Day Bros foundry, makers of this tyre bender, was operating as the manufacture of wheel right and blacksmith tools and general machinery in the 19th century in the USA and successfully exported their goods all over the world. Wagon tyre benders would have been very common circa 1850-1920, so there were probably many makers over the years. Early on, it would have become clear to the blacksmiths about which designs worked best so, eventually, the various makers would have made similar products to each other. This tyre bender was once used by Harry Goodall of H. Goodall & Sons Pty. Ltd. corner of McKinnon and High Streets, Terang. Victoria. Henry Goodall & Sons Henry Goodall (1870-1936) was proprietor of garages as H. Goodall & Sons Pty. Ltd., at both Terang (McKinnon and High Streets) and Mortlake (Dunlop Street). His business was in operation in at least in 1916 and perhaps well before, considering the date of the tyre bender and its use for wagons with wooden wheels. It was still in operation in 1953, chasing up debtors in Mount Gambier Court. Amongst the employees of H. Goodall & Sons Pty. Ltd. was Ernie Entwistle, a blacksmith (a soldier who died in 1916 ) and Alfred Hodgetts, radio expert (killed in a fatal accident in 1943, when he was in his early 30s ). Henry Goodall was involved in the community as a Justice of Peace, a deputy coroner, President of the Mortlake Hospital, trustee of the Soldiers’ Memorial Hall, and as a prominent Freemason. He and his wife had two sons (Charles and John) and one daughter (Mrs. Chas. Newton, of Skipton). The tyre bender is significant as it demonstrates how blacksmiths or wheelwrights could make new metal rims for wagon wheels for carts, wagons, stage coaches and carriages over a 135 years ago. The machine is a part of our social history as it demonstrates part of the process of making wagon wheels, which played an important part in aiding the continuation of daily transport needs that people had at the time, such as farming, personal transport and commercial activities. The machine or tool is locally significant as it was used by a local company in Terang and Mortlake in their blacksmith, wheelwright and garage business. Steel tyre bender mounted on timber base, used for wagon wheel steel rims. Made from cast iron and steel, double geared with four cogs to unite the upper and lower steel rollers. There are adjustable guide collars to keep the iron in line while it is being bent. It can also be used with two cranks for heavy duty work utilising the use to two operators. It is the Giant model, made in 1884 by Day Bros. of Philadelphia. This tyre bender once belonged to Harry Goodall & Sons, blacksmith's of Terang. Victoria. “DAY BROS. PHILAP. PA” cast into the side of machineflagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, machinery, wagon wheel, wheelwrights, blacksmith, steel rim wheels, tyre bender, tire bender, the giant tyre bender, henry goodall (1870-1936), terang, wheelwright tool, blacksmith trade, blacksmithing equipment and supplies, wagon tyre bender, day bros. philadelphia pennsylvania, h. goodall & sons of terang, terang blacksmith, h. goodall & sons pty ltd, mortlake, ernie entwistle blacksmith, alfred hodgetts radio expert, charles goodall, john goodall, mrs. chas. newton nee goodall -
 Flagstaff Hill Maritime Museum and Village
Machine - Steam Engine, Tangyes engineering, Mid-1880s
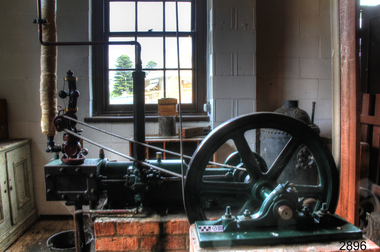
... machinery merchants Cameron & Sutherland, which also operated in Bendigo and Ballarat. A local cheese maker once used the engine to drive factory equipment. It was later donated to the Warrnambool Technical School, which then donated it to Flagstaff Hill to add to its historical steam engine collection. Between its manufacture and its donation to Flagstaff Hill, the governor had been replaced by the current Pickering governor. This engine design was very popular in the late 19th and early...machinery merchants Cameron & Sutherland, which also operated in Bendigo and Ballarat. A local cheese maker once used the engine to drive factory equipment. It was later donated to the Warrnambool Technical School, which then donated it to Flagstaff Hill to add to its historical steam engine collection. Between its manufacture and its donation to Flagstaff Hill, the governor had been replaced by the current Pickering governor. This engine design was very popular in the late 19th and early ...This Tangye B-size, single-cylinder, horizontal steam engine was likely manufactured in England around the mid-1880s. It was distributed by Melbourne machinery merchants Cameron & Sutherland, which also operated in Bendigo and Ballarat. A local cheese maker once used the engine to drive factory equipment. It was later donated to the Warrnambool Technical School, which then donated it to Flagstaff Hill to add to its historical steam engine collection. Between its manufacture and its donation to Flagstaff Hill, the governor had been replaced by the current Pickering governor. This engine design was very popular in the late 19th and early 20th centuries. When connected and powered up, the engine could drive an overhead line shaft via a flat belt off its flywheel. The line shaft would then drive the machinery via flat belts. It could drive virtually any type of machinery, such as water and sewerage pumps, mine elevators, winches, cranes, metal forges, air blowers, and marine machinery. This engine features a mechanical governor, which controls the speed of the engine regardless of whether it is under load. It also has a water pump built into the valve rod, which is used to supply the boiler with water. Steam enters the cylinder via a slide valve and applies pressure to the piston; it is like a modern internal combustion engine, but in the case of the steam engine, the pressure is exerted in turn on either side of the piston. In other words, the connecting rod is pushed by steam via the piston and piston rod and then pulled back again by steam pushing on the opposite side of the piston. Thus, power is exerted almost continuously, except at the end of each piston stroke, when it reverses direction. In the 1880s, many local butter and cheese manufacturers installed Tangye steam engines to power their machinery. A comprehensive article in the Gippsland Mercury in September 1889 extolled the magnificence of the Farnham Butter Factory in Dennington, Warrnambool, and described how one Tangye engine was used to drive several machines in the cheese- and butter-making processes. A report in the Warragul Guardian in December 1890 notes that the newly opened Warrnambool Butter Factory used a Tangye steam engine to pump water from a 60-foot well. Tangye: Richard Tangye (1833–1906) and four of his brothers—James, Joseph, Edward, and George—were the sons of Joseph Tangye, a Quaker Cornish miner. In 1857, they founded the engineering firm Richard Tangye & Brothers in Birmingham, UK. In 1860, the firm became Tangye Brothers and moved to Cornwall Works in Birmingham. The business encouraged inventors to join the company and develop their patents there, as happened with Weston’s differential pulley block, invented by the Englishman Thomas Aldridge Weston in 1854. Tangye bought the patent in 1858, giving the firm the sole right to manufacture it. The design received a medal for “original application, practical utility and success” at the 1862 International Exhibition in London. Also in 1858, the Tangye firm was commissioned by Brunel’s shipping company to manufacture hydraulic lifting jacks, or rams, to launch the steamship SS Great Eastern. The success of this project brought favourable attention to the firm, and it became involved in other notable projects, including the erection of Cleopatra’s Needle in London in 1878 and work on the Forth Road Bridge in Scotland. The firm underwent several name changes over the years, including James Tangye and Brothers (1857), Tangye Brothers and Price (1859), Tangye Brothers (1860), Tangye Brothers & Holman (1876), Tangye Brothers (by 1878), Tangye Ltd. (1881), and then simply Tangye. Its machinery and equipment were exported worldwide. In 1884, a branch with showrooms, offices, and a warehouse was opened in Melbourne at Cornwall House, Collins Street West. The firm was well known for producing high-quality machinery for agriculture and industry. Even today, new Tangye machinery is available for a subsidiary of Allspeeds. An extensive account of the firm’s history, names, inventions, and further references is available in Grace’s Guide, which also includes references to and diagrams of the Tangye horizontal steam engine. The horizontal steam engine was made by the well-known engineering firm Tangye, known for its high quality of manufacture. It was an important development in machinery because it helped improve productivity. Engines of this type are still used in some parts of the world today. This engine is a good example of a late 19th-century steam engine used in industry and agriculture and adapted for many different purposes. It is also important locally because it was connected to a local cheese making business and part of the thriving western district dairy industry. It may have been one of the Tangyes engines used at the Farnham butter factory or the Warrnambool Butter Factory, which was reported to be one of the most important in the Colony. It is also connected to the Warrnambool Technical School, established in 1968. Steam engine: stationary Tangye Size B, single-cylinder, horizontal Mill type steam engine. It has a 4-inch diameter cylinder with an 8-inch stroke. The body is painted green, and the Pickering governor is red. It was manufactured in Birmingham, England, in accordance with Tangye's Patent 238930, and distributed by Cameron and Sunderland, Melbourne, in the mid-1880s. TANGEYS PATENT BIRMINGHAM B SIZE 238930 CAMERON & SUTHERLAND MELBOURNE THE PICKERING PORTLAND . GOVERNOR . CONN. U.S.A.flagstaff hill, warrnambool, maritime village, maritime museum, flagstaff hill maritime museum and village, shipwreck coast, great ocean road, machine, invention, engine, steam, steam engine, horizontal steam engine, tangyes horizontal steam engine, stationary steam engine, single cylinder steam engine, manufacturing, farming, pumps, lifting equipment, engines, machine tools, hydraulic rams, hydraulic pumps, steam pumps, differential pulleys, mill type steam engine, 4 inch cylinder, weston’s differential pulley, thomas aldridge weston, 1862 international exhibition in london, brunel, ss great eastern, cleopatra’s needle, forth road bridge, cornwall house, collins street melbourne, agricultural machinery, industrial machinery, allspeeds, dairy, pump, richard tangye & brothers, james tangye and brothers, tangye brothers and price, tangye brothers, tangye brothers & holman, tangyes ltd., tangye, richard tangye, james tangye, joseph tangye, edward tangye, george tangye, cornwall works, birmingham, pickering governor, pickering portland connecticut usa, 19th century, dairy plant, steam power, tangye's patent 238930, tangye b size engine, cameron & sutherland, machine merchants, 1880s, mid-1880s, cheese manufacturer, butter manufacturer, diary industry, warrnambool technical school, belt driven machinery, agriculture, mechanical governor, farnham butter factory, warrnambool butter factory -
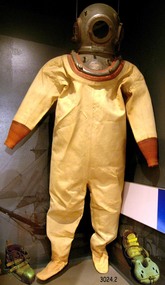 Flagstaff Hill Maritime Museum and Village
Functional object - Diving Suit, boots and weight, Early-to-mid 20th century
... , measuring machinery, water pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ..., measuring machinery, water pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ...This diving suit with helmet, boots and weight is part of the E. G.Ward collection, along with the diving compressor and a photograph of a diver in this equipment. Siebe Gorman & Company Ltd was a British company that developed diving equipment and breathing equipment and worked on commercial diving and marine salvage projects. The company advertised itself as 'Submarine Engineers'. It was founded by Augustus Siebe, a German-born British engineer chiefly known for his contributions to diving equipment. Siebe Gorman traded as an engineering firm for over 180 years from 1819 to 1999. The early success of the business was due to its founder, the Prussian immigrant Christian 'Augustus' Siebe (1788-1872). For business reasons, he applied for and was granted British citizenship in 1856. He was a gifted engineer who was able to translate theoretical problems into practical, working products. During the industrial Victorian period, the business traded as 'A. Siebe' at 145 High Street Holborn London, but in 1828 new premises were acquired at 5 Denmark Street, Soho. The family firm produced a wide range of manufactured goods including paper-making machinery, measuring machinery, water pumps, refrigeration equipment and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. Augustus Siebe is best remembered for the development and manufacture of the ‘closed’ Diving Dress based on the ideas of Charles and John Deane, George Edwards and Charles Pasley. Apart from some small modifications to valves and diver communications, the basic 12-bolt ‘closed’ diving dress remained relatively unchanged after the 1870s. Later company successes were also based on innovation, with new products that could be successfully developed and manufactured to high standards. This was largely attributed to the inventive nature, foresight, engineering and entrepreneurial skills of Robert Henry Davis (1870-1965). In 1882, RH Davis joined the company of 'Siebe & Gorman' as a young 11-year-old office boy and he was to remain with the company until he died in 1965. Augustus Siebe retired in 1869 and handed over the company to a new partnership of Henry H. Siebe (1830-1885) and William A. O'Gorman (1834-1904). The new firm traded as 'Siebe & Gorman' (1870-1879) from premises in and around Mason Street, Westminster Bridge Road, Lambeth, London. The two partners soon recognised the potential of R.H. Davis and in 1894, aged 24, he became General Manager of Siebe & Gorman. Davis increasingly ran the company until the surviving partner (W.A. Gorman) died in 1904. The firm was disposed of to the Vickers (armaments) family and a new company 'Siebe Gorman & Co. Ltd.' (1905-1998) was formed. Under the chairmanship of Albert Vickers, R.H. Davis was kept on as Managing Director, and the company forged ahead. However, after WW1, the Great Depression caused manufacturing output and share prices to slump. In 1924 Robert Davis made a deal with the Vickers Board and acquired control of the company through majority shares. Under his leadership, the Siebe Gorman Company flourished and within time, four of his sons also joined the firm. The company gained a worldwide reputation for the manufacture of diving apparatus, decompression and observation chambers, and safety breathing apparatus of all types for use on the land, in the air and under the sea (including mine rescue, tunnelling, aircraft, diving, submarine escape and in other hazardous environments). Close research and development links with the MOD (especially the Admiralty), also provided a lucrative outlet for the company products. In 1932, Robert Davis was knighted by King George V, principally for his invention of the ‘Davis Submerged Escape Apparatus’ (D.S.E.A.). Siebe Gorman essentially remained a family firm from the beginning (under A.Siebe) until it became a public company for the first time in 1952. However, following WW2, British manufacturing stagnated through stifled investment and post-war austerity, and there was little innovation. Siebe Gorman fortunes began to decline as an ageing Sir Robert Davis failed to invest, or change the company business and management practices. In 1959, Siebe Gorman was acquired by the “Fairy Group” and the ailing Sir Robert was made Life President. Consequently, nothing changed and the slow decline continued until Sir Robert's death in March 1965. Around 1960, Siebe Gorman acquired the diving apparatus manufacturer C E Heinke, and for a brief period, it manufactured some diving equipment under the combined name of Siebe Heinke. Around 1964, Mr E. 'Barry' Stephens was appointed as the new Managing Director to modernise Siebe Gorman. Changes were made, including a move to a new factory in Wales in 1975. The new company concentrated on fire-fighting breathing apparatus and escape equipment, and the move coincided with the loss of many of the older, traditional craft skills. Between 1985 and 1998, Siebe expanded through acquisitions, and several other companies were acquired. The Siebe Gorman (diving apparatus) company has therefore traded as A. Siebe (1819-1870); Siebe & Gorman (1870-1879); Siebe Gorman & Co (1880-1904); Siebe Gorman & Co. Ltd (1905-1998).The diving suit, helmet, boots, and weights, along with associated equipment in the Flagstaff Hill collection, represent a highly significant snapshot of marine history. These items are particularly important in understanding the evolution of diving equipment, with a special focus on their use in salvage operations before and throughout the Second World War. Manufactured by a company renowned for its inventions, development, and innovation in marine engineering, the equipment demonstrates the progression of technology in deep-sea diving. Early helmets and related items produced by this company remain highly sought after by collectors worldwide, highlighting their historical and technological value. The presence of these items within the Flagstaff Hill Maritime Museum allows for a unique insight into the working conditions and methods employed by divers. It also illustrates the considerable dangers they faced while performing such essential and hazardous work, underscoring the critical role played by these professionals in maritime history.Diving suit including helmet, boots and a weight. Diving suit is made of canvas with knitted cuffs. The helmet is metal. The boots have a thick sole and thick leather upper that is held on with leather straps and buckles. The toe of the boot is heavy metal. The weight is worn next to the trunk of the diver and it has an inscription to mark the front. It is worn with straps and buckles holding it in place. Royal Navy Admiralty Pattern 6 bolt No 3 light Siebe Gorman light diving helmet circa 1960, used by the Royal Navy before and after World War 2. This equipment is part of the E. G. Ward Collection."Siebe Gorman & Co Ltd Marine Engineers London. Patent" with "E G Ward" on front and back plate. On weight "FRONT"flagstaff hill, warrnambool, diving suit, siebe gorman and co ltd., siebe gorman and co ltd marine engineers london, marine engineers, diving helmet, diving boots, diving weight, marine diving, maritimemuseum, maritime village, maritime history, marine technology, life saving, deep sea diving, maritime museum, siebe gorman and co ltd., siebe gorman and co ltd, london, deep-sea diving, e. g. ward, e g ward, e.g. ward, edward ward, ted ward -
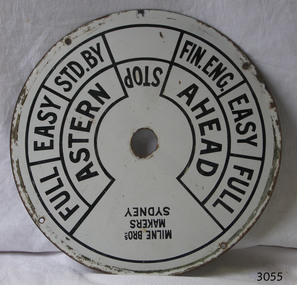 Flagstaff Hill Maritime Museum and Village
Equipment - Ships' Telegraph section, Milne Brothers, Copper and Brass Works, Early-to mid-20th century
... machinery and gauges for the Railways. The Engine Room section is significant for being part of the communications system on the ship SS Rip, owned by Melbourne's Ports & Harbours department and used to service and maintain the navigation signals of Port Phillip Bay and at Queenscliffe in the mid-20th century. The dial is an example of marine equipment made in Australia and used for the safety of Victorian vessels. It is also significant for being made by an early ...This Engine Room section of a ship's telegraph system was part of the equipment of the Ports and Harbour ship the SS Rip. The vessel serviced and maintained the lights and buoys at Port Phillip Bay and Queenscliffe. The SS Rip was possibly the former gunboat "Albert". The ship’s communication system that was used from the late 19th century to early-to-mid-20th-century is called an Engine Order Telegraph (E.O.T.) or ship’s telegraph. The system has two parts, the Bridge Section and the Engine Room Section. The Bridge Section is usually mounted on top of a pedestal, and the Engine Room Section is often attached to a vertical surface. The standard commands printed or stamped onto the dial are the directions of AHEAD and ASTERN, and the speeds of STOP, FULL, EASY, STD. BY. and FIN. ENG. The ship’s pilot on the Bridge of a vessel sends his Orders for speed and direction to the to the Engine Room with the E.O.T. He moves the lever or levers, depending on the number of engines the ship has, to change the indicator on the Bridge Section’s dial to point in the new direction and speed of travel. This change causes the Orders to be duplicated on the Engine Room Section’s dial and a bell to signal the change simultaneously. The engineer then adjusts the ship’s engines and steering equipment to follow the pilot’s Order. The manufacturer, Mulne Bros., was a copper and brass works at 166 Sussex Street Sydney, in December 1892, and previously from 1870 at 128 to 130 Sussex Street. The company made and sold a wide range of equipment including machinery and gauges for the Railways.The Engine Room section is significant for being part of the communications system on the ship SS Rip, owned by Melbourne's Ports & Harbours department and used to service and maintain the navigation signals of Port Phillip Bay and at Queenscliffe in the mid-20th century. The dial is an example of marine equipment made in Australia and used for the safety of Victorian vessels. It is also significant for being made by an early Australian manufacturer, Milne Brothers of Sydney.Engine Room Section of a ship’s telegraph or Engine Order Telegraph (E.O.T.). The round metal dial has inscriptions stamped around the edges. The inscriptions are nautical terms for direction and speed and include the maker’s details. The dial was made by Milne Bros. of Sydney. It was part of the equipment on the "SS Rip" in Victoria.Black paint around dial: "MILNE BROS. / MAKERS / SYDNEY" "FULL EASY STD. BY " "FIN ENG. EASY FULL" ""ASTERN" "STOP" "AHEAD"flagstaff hill, warrnambool, maritime museum, maritime village, great ocean road, shipwreck coast, marine technology, marine communications, engine order telegraph, e.o.t., ship’s telegraph, bridge section, engine room section, ship’s engine telegraph section, marine telegraph, milne bros., milne brothers, sydney, copper and brass works, ports & harbours ship, ss rip, gunboat albert, service ship, maintenance ship -
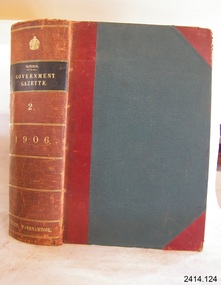 Flagstaff Hill Maritime Museum and Village
Book - Reference/Colonial Government Notification Gazette, James Kemp, The Victorian Government Gazette 1906 Vol 2 /129, 1906
... Under his management, the GPO expanded its reliance on automated typesetting machinery such as Linotype and Monotype systems to handle the immense volume of legislative work required by two levels of government. During his leadership, the Victorian GPO was also responsible for printing Australian colonial and state postage stamps, as well as early post-Federation Commonwealth stamp issues prior to the opening of the dedicated Commonwealth Stamp Printing Office. ...Under his management, the GPO expanded its reliance on automated typesetting machinery such as Linotype and Monotype systems to handle the immense volume of legislative work required by two levels of government. During his leadership, the Victorian GPO was also responsible for printing Australian colonial and state postage stamps, as well as early post-Federation Commonwealth stamp issues prior to the opening of the dedicated Commonwealth Stamp Printing Office. ...The Victoria Government Gazette and other government documents from 1887 were printed and published by Robert S. Brain, Government Printer, Melbourne. Brain held the position of Victorian Government Printer through the 1890s and into the early 1900s. The same imprint appears on other official Victorian publications from that era, such as the annual reports of the Board for the Protection of the Aborigines and the colony's Statistical Register. There wasn't really an editor in the modern sense the Gazette was compiled and issued under the authority of the colonial government, via the Chief Secretary's Department, with Brain's printing office producing and publishing it. In May 1906, James Kemp succeeded him, serving as Government Printer from May 1906 to August 1912, with the title of Acting Government Printer right at the very start of his tenure he was stepping into the role Brain had just vacated, and by later in December 1906 he was signing gazettes in that capacity, apparently before his appointment was made permanent. Then in 1913 Albert James Mullett took over the role starting from January 1913.Hard cover book. The Victorian Government Gazette 1906 Vol 2 /129 Printer: James Kemp Publisher: James Kemp Publisher: Authority of The Colonial Government Date: 1906 Further Information: Textured hard cover bound book leather burgundy colour spine with gilt lettering, covers embossed blue cloth & reinforced corners to front and back cover. non-fictionThe Victoria Government Gazette and other government documents from 1887 were printed and published by Robert S. Brain, Government Printer, Melbourne. Brain held the position of Victorian Government Printer through the 1890s and into the early 1900s. The same imprint appears on other official Victorian publications from that era, such as the annual reports of the Board for the Protection of the Aborigines and the colony's Statistical Register. There wasn't really an editor in the modern sense the Gazette was compiled and issued under the authority of the colonial government, via the Chief Secretary's Department, with Brain's printing office producing and publishing it. In May 1906, James Kemp succeeded him, serving as Government Printer from May 1906 to August 1912, with the title of Acting Government Printer right at the very start of his tenure he was stepping into the role Brain had just vacated, and by later in December 1906 he was signing gazettes in that capacity, apparently before his appointment was made permanent. Then in 1913 Albert James Mullett took over the role starting from January 1913. flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, book, the victoria government gazette 1906 2 vol 129, the victoria government gazette 1906, the victoria government gazette -
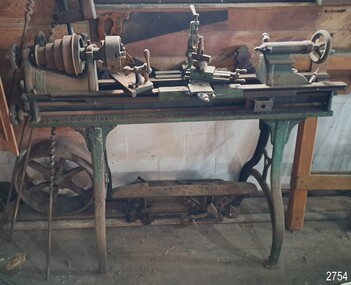 Flagstaff Hill Maritime Museum and Village
Machine - Lathe, W F & John Barnes, early 1900s
... Such a configuration reflects manufacturing practices from the late 1800s and early 1900s, when steam power was the predominant source for driving workshop and factory machinery. ...Such a configuration reflects manufacturing practices from the late 1800s and early 1900s, when steam power was the predominant source for driving workshop and factory machinery. ...This woodworking lathe, connected to both a pulley and a flywheel, demonstrates its historical operation with a steam engine. Such a configuration reflects manufacturing practices from the late 1800s and early 1900s, when steam power was the predominant source for driving workshop and factory machinery. Large machine shops often utilised a single power source, distributing power via roof-mounted belts and pulleys to operate several machines simultaneously. Over time, petrol-driven motors were introduced, and eventually, electricity became the standard power source. Conversion kits were made available in the late 19th and early 20th centuries to adapt older lathes to these newer, cleaner fuels. Manufacturer's History: W.F. & J. Barnes was a renowned maker of hand- and foot-powered treadle woodworking and metalworking machinery, established in 1869. The partnership between William F. Barnes and John Barnes was formalised in 1872, and the firm was incorporated in 1884. Their machines were used for both ‘farm’ applications and professional engineering. By 1881, the company began producing electrically powered machinery. By 1937, W.F. & J. Barnes expanded into manufacturing machinery for automotive assembly. The business closed in 1983, and in 1998, LeBlond Ltd. of Ohio acquired the firm. The lathe was donated by Briggs Marine, Melbourne: In Flagstaff Hill’s formative years, 1972-1975, Briggs Marine, Melbourne (Briggs Brass Foundry), donated equipment and objects used or made at their premises. The foundry was established in 1912 by Herbert Harrison Briggs. In 1965, the firm was owned by partners Cyril Briggs and Frank Lee: Cyril died in 1967, and Frank died in 1971, so the foundry was then run by his son and daughter-in-law, Les and Eva Lee. Briggs Marine’s Warrnambool Branch closed in 1972 after the death of Frank Lee in 1971. Flagstaff Hill’s founding director, John Lindsay, recalled that Briggs Marine’s family members gave personal assistance in setting up the displays in the original village shops, particularly the ‘Brass Foundry’ building, around the time the Maritime Museum opened in 1975. Briggs Marine still exists today, but the Briggs family is no longer involved. This early 1900s lathe marks a significant stage in the evolution of machinery, positioned between the era of hand-operated machines and the advent of electrically powered equipment. Its presence exemplifies the progression of industrial technology and craftsmanship during this period. The lathe is particularly notable for its association with the Briggs Brass Foundry. The foundry was known for developing a specialised brass alloy composed of non-ferrous metals, a formulation that resulted in durable products built to withstand the demanding conditions of marine environments. This focus on resilience and longevity made Briggs Brass Foundry’s goods highly sought after within the maritime sector. Briggs Maine, a long-established business, utilised the foundry’s capabilities to create cast goods tailored to the needs of the marine industry. The facility was equipped to deliver both custom-designed and mass-produced items, ensuring versatility in meeting various requirements. Many of Briggs Foundry’s products found their place on sailing and steam vessels throughout Victoria’s coastline, including in the port town of Warrnambool, where there was once a brancy of Briggs Marine. In addition to general marine fittings, Briggs Marine earned recognition for its expertise in bell-founding. The foundry’s reputation is closely linked to the restoration of the Schomberg Bell at Flagstaff Hill, a small but historically significant bell from a luxury migrant vessel dating back to the mid-19th century. The successful restoration of the Schomberg Bell demonstrates Briggs Brass Foundry’s commitment to preserving craftsmanship and maritime heritage.The lathe is a green, bench-type, steam-powered woodworking machine. Its bench is supported by decorative posts at each end, with each post dividing into arched legs. The lathe is mechanically connected to both a pulley and a flywheel, designed to be operated in conjunction with a steam engine. Included with the lathe is a range of accessories. Across the front of the machine, an inscription is cast, and a stamped, metal lathe pulley guide is attached to the drive mechanism. The lathe was manufactured by W. F. and J. Barnes, Rockford, Illinois, USA, during the 1900s.“W F and J Barnes, Rockford, USA” "1820" "1887"flagstaff hill, flagstaff hill maritime museum and village, warrnambool, maritime museum, maritime village, great ocean road, shipwreck coast, lathe, steam-operated lathe, steam-operated pulley, steam power, steam engine, machine, steam operated machine, metal work, foundry work, metal working trade, tool, pulley driven, metalworking, woodworking, barnes lathe, briggs marine, belt driven, wordworking lathe, free standing lathe, bench lathe, steam powered, vintage lathe, woodturning lathe, w. f. and j. barnes, illanois, early 20th century, briggs, briggs brass foundry, briggs marine foundry, briggs marine products, herbert harrison briggs, george edward briggs, cyril falkiner mckinnon briggs, collingwood, moorabbin, frank lee, les lee, eva lee, briggs marine warrnambool, non-ferrous founders, bell specialists, ship bell specialists, sand cast, marine equipment, marine fittings, foundry, brass foundry, founders -
 Flagstaff Hill Maritime Museum and Village
Equipment - Pattern, Briggs Brass Foundry, Early 20th century
... In the early years of Flagstaff Hill, the Briggs family generously donated the crate of patterns along with other related items such as brassware, tools and machinery. ...In the early years of Flagstaff Hill, the Briggs family generously donated the crate of patterns along with other related items such as brassware, tools and machinery. ...The wooden pattern forms part of a larger collection, securely stored within a durable wooden crate. This pattern was an essential tool at Briggs’ Brass Foundry, specifically designed for creating sand casts. Sand casting is a time-honoured technique, with a history exceeding 2,000 years. The handcrafted nature of this process results in the production of brass and copper alloy items, which are particularly suitable for maritime applications. Typical products include bells, boat hooks, cowls, propellers, handles, lids, rowlocks, hooks, letters, bolts, rail holders, brackets, deck plates, flanges, rudder guides, portholes and covers. The distinctive bronze mixture used at Briggs’ Foundry is copper-based, composed of local ingots of copper, tin, zinc and lead, blended in precisely measured quantities. The resulting alloy is non-ferrous, known for its exceptional durability and longevity. In the early years of Flagstaff Hill, the Briggs family generously donated the crate of patterns along with other related items such as brassware, tools and machinery. These items were prominently displayed in a simulated Brass Foundry within the Village, alongside other working crafts, trades and services typical of a maritime town. From the completion of the building in 1986 until its repurposing in 1994, visitors could view these items and gain insight into the foundering and metalwork trades that supported maritime industries, including shipwrights and boatbuilders. The castings produced at the foundry were also vital for farmers, manufacturers and other local industries. The Brass Foundry display featured a historic Cornish chimney, constructed as a working model to illustrate the process of smelting metal in furnaces and pouring it into sand moulds. The chimney, crafted from specially curved bricks, currently stands at approximately two-thirds of its original height, having previously been located at the Grassmere Cheese factory. The craft of sand-casting, which utilises intricately carved wooden patterns to create metal objects, stands as a testament to the enduring value of traditional skills. This age-old technique remains relevant today, linking past craftsmanship to ongoing industrial practices. The foundry pattern set holds particular significance due to its strong associations with brass foundries, both locally and in coastal regions across Victoria. In these areas, marine industries such as ship and boat building have long depended on high-quality metal castings for the machinery, equipment, and fittings essential to their operations. The alloys formulated by Briggs Brass Foundry, crafted from non-ferrous metals, were specifically designed to provide superior longevity and durability in maritime environments. These patterns are closely tied to the history of the Briggs Brass Foundry, a respected and long-running company that specialised in producing cast goods for the marine sector. The foundry was equipped to supply both unique, one-off items and mass-produced components, ensuring that its products found their way onto a variety of sail and steam vessels along the Victorian coast, including in Warrnambool. In addition to its broader marine applications, Briggs Brass Foundry established itself as a bell-founder specialist. The company’s expertise is notably linked to the historic Schomberg Bell at Flagstaff Hill, which they restored to its original splendour as a fine example of a bell from a luxury migrant ship of the mid-19th century. The significance of the pattern set is further heightened by its association with Briggs Brass Founders, a firm established in the early 20th century and widely recognised for its proficiency in producing, repairing, and restoring ship bells and other marine equipment. Renowned for their non-ferrous metal casting, Briggs Brass Founders consistently supplied high-quality fittings and equipment vital to maritime pursuits. Moreover, the company expanded its influence by opening a branch in Warrnambool. Through this local presence, Briggs Brass Founders supported the regional marine industry and forged strong connections with fishermen and businesses. This not only reinforced their reputation as skilled manufacturers but also highlighted their commitment to community engagement and support. Pattern; hexagonal wooden shape painted orange. The thick carved wooden shape is in halves forming a hole when locked together with the dowel pegs and opposing drilled holes. The pattern is part of a set of foundry patterns from Briggs Brass Foundry.flagstaff hill, flagstaff hill maritime museum and village, warrnambool, maritime museum, maritime village, great ocean road, shipwreck coast, briggs' bronze, trade, sand cast, cast, brass alloy, copper alloy, pattern, mould, foundry, brass foundry, metal foundry, casting, sand mould, sand casting, marine equipment, marine tools, marine fittings, copper tin zinc lead, non-ferrous, non-corrosive, brassware, metalware, foundering, metalwork, maritime, bell founders, ship chandlers, marine products, briggs family, herbert harrison briggs, h h briggs, george edward briggs, cyril falkiner mckinnon briggs, cyril briggs, briggs & son brass foundry, h h briggs & sons foundry, briggs marine, alliance casting & engineering solutions, grassmere cheese factory, cornish chimney, curved bricks, collingwood, moorabbin, collingwood foundry, moorabbin foundry, 1912, briggs, briggs brass foundry, briggs marine foundry, briggs marine products, frank lee, les lee, eva lee, briggs marine warrnambool, non-ferrous founders, bell specialists, ship bell specialists, founders, traditional send casting -
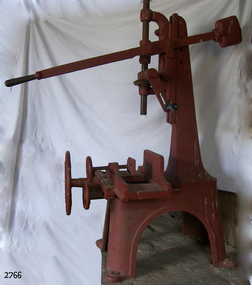 Flagstaff Hill Maritime Museum and Village
Tool - Mortice Machine, Mathieson and Son, 1910-1940
... McPherson's started as an Australian retailer of hardware products in Melbourne going on to become a company that supplied machinery and other items for the establishment of major infrastructure projects in Australia during the early days of the colony that assisted in linking the various states and territories which became a precursor of Federation. ...In 1792 John Manners had set up a workshop making woodworking planes at 14 Saracens Lane Glasgow. He also had employed an apprentice Alexander Mathieson (1773-1851). But in the following year at Saracen's Lane, the 1841 census describes Alexander Mathieson as a master plane-maker now at 38 Saracen Lane with his son Thomas Adam working with him as a journeyman plane-maker. Presumably, Alexander must have taken over the premises and business of John Manners. Now that the business had Thomas Adam Mathieson working with his father it gradually grew and became more diversified, and it is recorded at the time by the Post-Office Glasgow Annual Directory that by 1847-1848 Alexander Mathieson was a “plane, brace, bit, auger & edge tool maker” In 1849 the firm of James & William Stewart at 65 Nicolson Street, Edinburgh was taken over and Thomas was put in charge of the business, trading under the name Thomas A. Mathieson & Co. as plane and edge-tool makers. Thomas's company went on to acquire the Edinburgh edge-tool makers “Charles & Hugh McPherson” and took over their premises in Gilmore Street. In the Edinburgh directory of 1856/7, the business is recorded as being Alexander Mathieson & Son, plane and edge-tool makers at 48 Nicolson Street and Paul's Work, Gilmore Street Edinburgh. In the 1851 census, Alexander is recorded as working as a tool and plane-maker employing eight men. Later that year Alexander died and his son Thomas took over the business. Under the heading of an edge-tool maker in the 1852/3 Post-Office Glasgow Annual Directory the firm is now listed as Alexander Mathieson & Son, with further entries as "turning-lathe and vice manufacturers". By the early 1850s, the business had moved to 24 Saracen Lane. The directory for 1857/8 records that the firm had moved again only a few years later to East Campbell Street, off the Gallowgate area, and that through further diversification was also manufacturing coopers' and tinmen's tools. The ten-yearly censuses report the firm's growth in 1861 stating that Thomas was a tool manufacturer employing 95 men and 30 boys; in 1871 he had 200 men working for him and in 1881 300 men. By 1899 the firm had been incorporated as Alexander Mathieson & Sons Ltd, even though only Alexander's son Thomas appears ever to have joined the firm so the company was still in his fathers' name. In September 1868 Thomas Mathieson put a notice in the newspapers of the Sheffield & Rotherham Independent and the Sheffield Daily Telegraph stating that his firm had used the trade-mark of a crescent and star "for some time" and that "using or imitating the Mark would be proceeded against for infringement". The firm had acquired its interest in the crescent-and-star mark from the heirs of Charles Pickslay, the Sheffield cutler who had registered it with the Cutlers' Company in 1833 and had died in 1852. The year 1868 seems also to be the one in which the name Saracen Tool Works was first adopted; not only does it figure at the foot of the notice in the Sheffield press, it also makes its first appearance in the firm's entry in the Post-Office Glasgow Annual Directory in the 1868/9 edition. As Thomas Mathieson's business grew, so too did his involvement in local public life and philanthropy. One of the representatives of the third ward on the town council of Glasgow, he became a river bailie in 1868, a magistrate in 1870, and a preceptor of Hutcheson's Hospital in 1878. He had a passion for books and was an "ardent Ruskinian". He served on the committee handling the bequest for the setting up of the Mitchell Library in Glasgow. When he died at Coulter Maynes near Biggar in 1899, he left an estate worth £142,764. Company's later years: Both Thomas's sons, James Harper and Thomas Ogilvie were involved in the continuing life of the firm. James followed in his father's footsteps in becoming a local public figure. He was appointed Deputy Lieutenant of the County of the City of Glasgow and was made a deacon of the Incorporation of the Hammermen of Glasgow in 1919. His brother Thomas Ogilvie was recorded as a tool manufacturer and employer in the 1911 census. Thomas Ogilvie's son Thomas Alastair Sutherland Ogilvie Mathieson was born in 1908 took a rather different approach to engineering, however, by becoming a racing driver. In 1947 he wed the French film actress Mila Parély. The firm had won many awards at world fairs for their goods. At the Great Exhibition, London, 1851. Prize medal for joiners' tools in the class of Cutlery & Edge Tools, Great London Exposition, 1862. Prize medal honoris causa. International Exhibition, Melbourne, 1880. Gold medal International Exhibition of Industry, Science and Art, Edinburgh, 1886 Prize medal. See note section for Thomas McPherson Australian Retailer information: The firm of Alexander Mathieson & Sons was one of the leading makers of hand tools and later woodworking machines in Scotland. Its success went hand in hand with the growth of the shipbuilding industries on the Firth of Clyde in the nineteenth century and the emergence of Glasgow regarded as the "second city of the Empire". It also reflected the firm's skill in responding to an unprecedented demand for quality tools by shipyards, cooperages, and other industries, both locally and throughout the world. McPherson's started as an Australian retailer of hardware products in Melbourne going on to become a company that supplied machinery and other items for the establishment of major infrastructure projects in Australia during the early days of the colony that assisted in linking the various states and territories which became a precursor of Federation. From a humble beginning McPherson's became one of Australia's leading retail, and later manufacturing businesses that is still in existence today.Mortice machine metal with long metal lever handle with counter weight & 3 adjustment wheels & metal crank with wood end. Has 4 feet that can be bolted to floor & vertical moving piece that a cutting bit would fit into.Imprinted Alex Mathieson & Son Trademark Saracen Tool works Glasgow' also a brass plate "Thomas McPherson & Son Machinery Importer Melbourne"flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village -
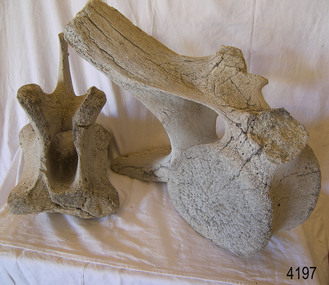 Flagstaff Hill Maritime Museum and Village
Animal specimen - Whale bone, Undetermined
... early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. ...early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. ...Prior to carrying out a detailed condition report of the cetacean skeletons, it is useful to have an understanding of the materials we are likely to encounter, in terms of structure and chemistry. This entry invites you to join in learning about the composition of whale bone and oil. Whale bone (Cetacean) bone is comprised of a composite structure of both an inorganic matrix of mainly hydroxylapatite (a calcium phosphate mineral), providing strength and rigidity, as well as an organic protein ‘scaffolding’ of mainly collagen, facilitating growth and repair (O’Connor 2008, CCI 2010). Collagen is also the structural protein component in cartilage between the whale vertebrae and attached to the fins of both the Killer Whale and the Dolphin. Relative proportions in the bone composition (affecting density), are linked with the feeding habits and mechanical stresses typically endured by bones of particular whale types. A Sperm Whale (Physeter macrocephalus Linnaeus, 1758) skeleton (toothed) thus has a higher mineral value (~67%) than a Fin Whale (Balaenoptera physalus Linnaeus, 1758) (baleen) (~60%) (Turner Walker 2012). The internal structure of bone can be divided into compact and cancellous bone. In whales, load-bearing structures such as mandibles and upper limb bones (e.g. humerus, sternum) are largely composed of compact bone (Turner Walker 2012). This consists of lamella concentrically deposited around the longitudinal axis and is permeated by fluid carrying channels (O’Connor 2008). Cancellous (spongy) bone, with a highly porous angular network of trabeculae, is less stiff and thus found in whale ribs and vertebrae (Turner Walker 2012). Whale oil Whales not only carry a thick layer of fat (blubber) in the soft tissue of their body for heat insulation and as a food store while they are alive, but also hold large oil (lipid) reserves in their porous bones. Following maceration of the whale skeleton after death to remove the soft tissue, the bones retain a high lipid content (Higgs et. al 2010). Particularly bones with a spongy (porous) structure have a high capacity to hold oil-rich marrow. Comparative data of various whale species suggests the skull, particularly the cranium and mandible bones are particularly oil rich. Along the vertebral column, the lipid content is reduced, particularly in the thoracic vertebrae (~10-25%), yet greatly increases from the lumbar to the caudal vertebrae (~40-55%). The chest area (scapula, sternum and ribs) show a mid-range lipid content (~15-30%), with vertically orientated ribs being more heavily soaked lower down (Turner Walker 2012, Higgs et. al 2010). Whale oil is largely composed of triglycerides (molecules of fatty acids attached to a glycerol molecule). In Arctic whales a higher proportion of unsaturated, versus saturated fatty acids make up the lipid. Unsaturated fatty acids (with double or triple carbon bonds causing chain kinks, preventing close packing (solidifying) of molecules), are more likely to be liquid (oil), versus solid (fat) at room temperature (Smith and March 2007). Objects Made From the Whaling Industry We all know that men set forth in sailing ships and risked their lives to harpoon whales on the open seas throughout the 1800s. And while Moby Dick and other tales have made whaling stories immortal, people today generally don't appreciate that the whalers were part of a well-organized industry. The ships that set out from ports in New England roamed as far as the Pacific in hunt of specific species of whales. Adventure may have been the draw for some whalers, but for the captains who owned whaling ships, and the investors which financed voyages, there was a considerable monetary payoff. The gigantic carcasses of whales were chopped and boiled down and turned into products such as the fine oil needed to lubricate increasing advanced machine tools. And beyond the oil derived from whales, even their bones, in an era before the invention of plastic, was used to make a wide variety of consumer goods. In short, whales were a valuable natural resource the same as wood, minerals, or petroleum we now pump from the ground. Oil From Whale’s Blubber Oil was the main product sought from whales, and it was used to lubricate machinery and to provide illumination by burning it in lamps. When a whale was killed, it was towed to the ship and its blubber, the thick insulating fat under its skin, would be peeled and cut from its carcass in a process known as “flensing.” The blubber was minced into chunks and boiled in large vats on board the whaling ship, producing oil. The oil taken from whale blubber was packaged in casks and transported back to the whaling ship’s home port (such as New Bedford, Massachusetts, the busiest American whaling port in the mid-1800s). From the ports it would be sold and transported across the country and would find its way into a huge variety of products. Whale oil, in addition to be used for lubrication and illumination, was also used to manufacture soaps, paint, and varnish. Whale oil was also utilized in some processes used to manufacture textiles and rope. Spermaceti, a Highly Regarded Oil A peculiar oil found in the head of the sperm whale, spermaceti, was highly prized. The oil was waxy, and was commonly used in making candles. In fact, candles made of spermaceti were considered the best in the world, producing a bright clear flame without an excess of smoke. Spermaceti was also used, distilled in liquid form, as an oil to fuel lamps. The main American whaling port, New Bedford, Massachusetts, was thus known as "The City That Lit the World." When John Adams was the ambassador to Great Britain before serving as president he recorded in his diary a conversation about spermaceti he had with the British Prime Minister William Pitt. Adams, keen to promote the New England whaling industry, was trying to convince the British to import spermaceti sold by American whalers, which the British could use to fuel street lamps. The British were not interested. In his diary, Adams wrote that he told Pitt, “the fat of the spermaceti whale gives the clearest and most beautiful flame of any substance that is known in nature, and we are surprised you prefer darkness, and consequent robberies, burglaries, and murders in your streets to receiving as a remittance our spermaceti oil.” Despite the failed sales pitch John Adams made in the late 1700s, the American whaling industry boomed in the early to mid-1800s. And spermaceti was a major component of that success. Spermaceti could be refined into a lubricant that was ideal for precision machinery. The machine tools that made the growth of industry possible in the United States were lubricated, and essentially made possible, by oil derived from spermaceti. Baleen, or "Whalebone" The bones and teeth of various species of whales were used in a number of products, many of them common implements in a 19th century household. Whales are said to have produced “the plastic of the 1800s.” The "bone" of the whale which was most commonly used wasn’t technically a bone, it was baleen, a hard material arrayed in large plates, like gigantic combs, in the mouths of some species of whales. The purpose of the baleen is to act as a sieve, catching tiny organisms in sea water, which the whale consumes as food. As baleen was tough yet flexible, it could be used in a number of practical applications. And it became commonly known as "whalebone." Perhaps the most common use of whalebone was in the manufacture of corsets, which fashionable ladies in the 1800s wore to compress their waistlines. One typical corset advertisement from the 1800s proudly proclaims, “Real Whalebone Only Used.” Whalebone was also used for collar stays, buggy whips, and toys. Its remarkable flexibility even caused it to be used as the springs in early typewriters. The comparison to plastic is apt. Think of common items which today might be made of plastic, and it's likely that similar items in the 1800s would have been made of whalebone. Baleen whales do not have teeth. But the teeth of other whales, such as the sperm whale, would be used as ivory in such products as chess pieces, piano keys, or the handles of walking sticks. Pieces of scrimshaw, or carved whale's teeth, would probably be the best remembered use of whale's teeth. However, the carved teeth were created to pass the time on whaling voyages and were never a mass production item. Their relative rarity, of course, is why genuine pieces of 19th century scrimshaw are considered to be valuable collectibles today. Reference: McNamara, Robert. "Objects Made From the Whaling Industry." ThoughtCo, Jul. 31, 2021, thoughtco.com/products-produced-from-whales-1774070.Whale bone was an important commodity, used in corsets, collar stays, buggy whips, and toys.Whale bone in two pieces. Advanced stage of calcification as indicated by deep pitting. Off white to grey.None.flagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, whale bones, whale skeleton, whales, whale bone, corsets, toys, whips -
 Federation University Historical Collection
Book, Machinery for Metalliferous Mines, 1894, 1894
... machinery used in late 19th century metal mining in the UK and overseas is very rare. It covers a wide range of equipment - pumps, steam engines, drills, winding engines, stamps & concentration mills, aerial ropeways, tramways and early uses of electricity etc. mining cornish pump linkenbach table water wheel ventilation oil engine california america water steam boilers steam engines oil engines pumpimg rock drilling boring jiggers milling silver gold drying and roasting chlorination cyaniding lead zinc copper electricity electric lighting wire ropes transport wind engine poppet head Brown hard cloth covered book. xvi 564 pages with additional advertisements, with over 300 illustrations and drawings, some fold out. ...The 1st edition of this famous work, giving an excellent account of the machinery used in late 19th century metal mining in the UK and overseas is very rare. It covers a wide range of equipment - pumps, steam engines, drills, winding engines, stamps & concentration mills, aerial ropeways, tramways and early uses of electricity etc. Brown hard cloth covered book. xvi 564 pages with additional advertisements, with over 300 illustrations and drawings, some fold out. Chapters include Water as a motive power, Wind engines and ventilating machinery, Steam boilers/engines and oil engines, hoisting machinery, draining of Mines, pumping engines, rock drilling machinery, boring machinery, concentration machinery, sizing and classifications trommels, joggers and jigging, fine concentration, milling of gold ores, milling of silver ores, amalgamation plates and machinery, dry and roasting machinery, chlorination and cyandide processes for the extraction of gold, electricity as a motive power for mining, electric lighting and blasting, aerial wire ropeways, transport by rail and road. There a a number of lovely line illustrations in the book including: Poncelot's undershot waterwheel; Fromont furnace;Victor turbine; Pelton waterwheel; Root's positive blower;Cross section and front elevation of Lancashire boiler; Robey's Compound Mill Engine; Portable Winding Plant; Iron Pit Head Gear ; Loading Arrangement in an Incline Shaft; kibble; Worthington Pump; California Pump; Scram's Air Compressor; Rock drill Bits; Special Sharpening tools; Boring tools;Rotating Picking table; Ore Feeder; roller crusher; stamp battery; round buddle; slime table; vanner; amalgamating plant; belt elevator;roasting furnace;splicing wire rope; capel; tipping waggon;mining, cornish pump, linkenbach table, water wheel, ventilation, oil engine, california, america, water, steam boilers, steam engines, oil engines, pumpimg, rock drilling, boring, jiggers, milling, silver, gold, drying and roasting, chlorination, cyaniding, lead, zinc, copper, electricity, electric lighting, wire ropes, transport, wind engine, poppet head -
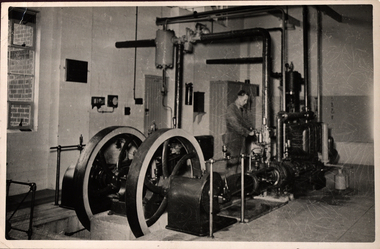 Federation University Historical Collection
Photograph - Photograph - Black and white, Ballarat School of Mines Model Steam Engine
... In the early stages the steam engine was used to drive an overhead transmission shaft for machinery in the adjacent workshop. ...In the early stages the steam engine was used to drive an overhead transmission shaft for machinery in the adjacent workshop. ...The Davey Paxman Experimental Steam Engine was purchased as the result of a bequest from Thomas Bath. The 'substantial sum' was used to build an Engineering Laboratory. The Ballarat School of Mines Council minutes of 08 November 1901 record: - Plans for [the] proposed building were submitted ... and ... it was resolved that a temporary building for an Engineering Laboratory be put up.' This laboratory, as an existing building, is first mentioned in the Ballarat School of Mines President's Annual Report of 1901, presented on 28 February 1902, reporting 'the erection of a building 67ft long by 33 ft wide' This report also lists all the equipment that would be accommodated in the Engineering Laboratory, including the experimental steam engine and boiler. The experimental Davey-Paxman steam engine arrived in Ballarat towards the end of 1902. The Engineering Laboratory was opened on 14 August 1903 by His Excellency Sir Sydenham Clarke. This engineering laboratory remained in use till about 1945. By 1944 preparations were under way at the Ballarat School of Mines to expand existing facilities, to be ready for the influx of returned soldiers. A new Heat Engines laboratory was built, this time of brick construction, replacing the previous corrugated-iron shed. In the early stages the steam engine was used to drive an overhead transmission shaft for machinery in the adjacent workshop. Later the steam engine was moved to a space that became the Heat Thermodynamics Laboratory. At the end of 1969 the engine was relocated to the Thermodynamics Laboratory at the then Ballarat Institute of Advanced Education (BIAE) Mt Helen Campus. It was donated to Sovereign Hill in 2006. According to the research of Rohan Lamb in 2001 around five experimental steam engines were made by Davey Paxman, and three of these had similar configuration to the Ballarat School of Mines Steam Engine, however, each of these was also unique with different valve arrangements. The list, which was on a scrap of paper in a folio held in the Essex Archives, confirmed that one was sent to India. The Ballarat steam engine can be dated to late 1901 to early 1902. Zig Plavina was responsible for moving the steam engine to Mount Helen, and worked on it as a technician for many years. He observed the following: * The condenser is driven by the low pressure engine. * The following arrangements are possible: i) the high pressure engine alone, exhausting to atmosphere. Condenser not used, crankshaft flanges not coupled. ii) crankshafts coupled, mains pressure (120 psi) steam supplied to high pressure engine, partially expanded steam delivered to low pressure engine (Tandem operation). Choice available re exhaust steam: either to the condenser or to atmosphere. iii) crankshafts not coupled, reduced pressure steam supplied to low pressure engine. Exhaust steam - either to the condenser or to atmosphere. * Valve arrangement - a choice of Pickering cut-off or throttle governor. On low pressure engine - throttle governor only.Black and white photograph of the Davey Paxman Experimental Steam Engine installed at the Ballarat School of MInes. steam engine, model steam engine, davey paxman, thomas bath, experimental steam engine -
 Flagstaff Hill Maritime Museum and Village
Ceramic - Jug, Baker & Co, 1891 to 1893
... By the early 1840s, William Baker was running it alone and was then using 'machinery for the potteries manufacturing operations in addition to the mill that was producing the raw clay. ...By the early 1840s, William Baker was running it alone and was then using 'machinery for the potteries manufacturing operations in addition to the mill that was producing the raw clay. ...W Baker and Co-produced many different types of pottery at their Fenton Potteries, Stoke-on-Trent, Staffordshire England. The company was established in 1790 by Ralph Bourne and William Baker the company was working at capacity by the end of the century. By the late 1820's Bourne and Baker, in partnership with John Bourne, had acquired additional works opposite the first in 1833. With the deaths of John Bourne and William Baker, the partnership was dissolved, and then for a short time, the business was carried on by Ralph Bourne and William Baker junior and John Baker. By the early 1840s, William Baker was running it alone and was then using 'machinery for the potteries manufacturing operations in addition to the mill that was producing the raw clay. The business was subsequently carried on by William Baker and Company that were known for the making of printed, sponged, and pearl-white granite ware for export in the early 1880s at the Fenton works between Manor and Fountain Streets. The original works on the south side of City Road were by then an en-caustic tile works, apparently still in the hands of the Baker family. The pottery works flourished under William Baker’s management and by the middle of the nineteenth century with almost 500 employees was the biggest firm in Fenton. An early piece of ironstone Staffordshire pottery now a collector's item showing the types of domestic items that were exported from England to its colonies towards the end of the nineteenth century and into the beginning of the twentieth.Water pitcher ironstone ceramic white with raised embossed Lilly of the valley decoration around handle and lip sections. Marked on bottom, "Royal stone china, Baker and Co, England" with emblem of lion, crown and unicornflagstaff hill, warrnambool, shipwrecked coast, flagstaff hill maritime museum, maritime museum, shipwreck coast, flagstaff hill maritime village, great ocean road, jug, kitchen utensil, kitchen ware, water pitcher -
 Flagstaff Hill Maritime Museum and Village
Tool - Machinery Oiler Can, First half of the 20th century
... machinery. Oil cans were made by companies like Noera Manufacturing Company and Perfection in the late 19th and early 20th centuries and around this time, oil cans frequently leaked and contributed to fires. ...machinery. Oil cans were made by companies like Noera Manufacturing Company and Perfection in the late 19th and early 20th centuries and around this time, oil cans frequently leaked and contributed to fires. ...An oil can or oiler is a can that holds oil usually motor oil for lubricating machines. An oil can can also be used to fill oil-based lanterns. An occupation, referred to as an oiler, can use an oil can (among other tools) to lubricate machinery. Oil cans were made by companies like Noera Manufacturing Company and Perfection in the late 19th and early 20th centuries and around this time, oil cans frequently leaked and contributed to fires. In 1957, aluminium oil cans were introduced, produced by companies like the American Can Company. Rocanville, Saskatchewan, Canada is home to a large-scale oil can industry because of the Symons Oiler factory which produced oil cans during World War II.The subject item at this time cannot be associated with an historical event, person or place, provenance is unknown, item a is believed to have been produced in the first half of the 20th century for marine use.Conical oiler can with spout, screw top lid and top hook for hanging, side handle missing.Noneflagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, conical pot, pot -
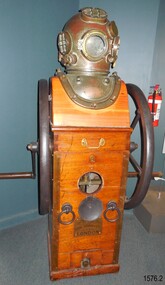 Flagstaff Hill Maritime Museum and Village
Equipment - Diving compressor and helmet, 1944
... , measuring machinery, water pumps, refrigeration equipment, and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ..., measuring machinery, water pumps, refrigeration equipment, and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. ...Siebe Gorman & Company Ltd was a British company that developed diving equipment and breathing equipment and worked on commercial diving and marine salvage projects. The company advertised itself as 'Submarine Engineers'. It was founded by Augustus Siebe, a German-born British engineer chiefly known for his contributions to diving equipment. Siebe Gorman traded as an engineering firm for over 180 years from 1819 to 1999. The early success of the business was due to its founder, the Prussian immigrant Christian 'Augustus' Siebe (1788-1872). For business reasons, he applied for and was granted British citizenship in 1856. He was a gifted engineer who was able to translate theoretical problems into practical, working products. During the industrial Victorian period, the business traded as 'A. Siebe' at 145 High Street Holborn London, but in 1828 new premises were acquired at 5 Denmark Street, Soho. The family firm produced a wide range of manufactured goods including paper-making machinery, measuring machinery, water pumps, refrigeration equipment, and diving apparatus. Augustus Siebe specialised in submarine engineering early on and the company gained a reputation for the manufacture of safe, reliable diving apparatus. Augustus Siebe is best remembered for the development and manufacture of the ‘closed’ Diving Dress based on the ideas of Charles and John Deane, George Edwards, and Charles Pasley. Apart from some small modifications to valves and diver communications, the basic 12 bolt ‘closed’ diving dress remained relatively unchanged after the 1870s. Later company successes were also based on innovation, with new products that could be successfully developed and manufactured to high standards. This was largely attributed to the inventive nature, foresight, engineering, and entrepreneurial skills of Robert Henry Davis (1870-1965). In 1882, RH Davis joined the company of 'Siebe & Gorman' as a young 11-year-old office boy and he was to remain with the company until he died in 1965. Augustus Siebe retired in 1869 and handed over the company to a new partnership of Henry H. Siebe (1830-1885) and William A. O'Gorman (1834-1904). The new firm traded as 'Siebe & Gorman' (1870-1879) from premises in and around Mason Street, Westminster Bridge Road, Lambeth, London. The two partners soon recognised the potential of R.H. Davis and in 1894, aged 24, he became General Manager of Siebe & Gorman. Davis increasingly ran the company until the surviving partner (W.A. Gorman) died in 1904. The firm was disposed of to the Vickers (armaments) family and a new company 'Siebe Gorman & Co. Ltd.' (1905-1998) was formed. Under the chairmanship of Albert Vickers, R.H. Davis was kept on as Managing Director, and the company forged ahead. However, after WW1, the Great Depression caused manufacturing output and share prices to slump. In 1924 Robert Davis made a deal with the Vickers Board and acquired control of the company through majority shares. Under his leadership, the Siebe Gorman Company flourished and within time, four of his sons also joined the firm. The company gained a worldwide reputation for the manufacture of diving apparatus, decompression and observation chambers, and safety breathing apparatus of all types for use on the land, in the air, and under the sea (including mine rescue, tunneling, aircraft, diving, submarine escape and in other hazardous environments). Close research and development links with the MOD (especially the Admiralty), also provided a lucrative outlet for the company products. In 1932, Robert Davis was knighted by King George V, principally for his invention of the ‘Davis Submerged Escape Apparatus’ (D.S.E.A.). Siebe Gorman essentially remained a family firm from the beginning (under A.Siebe) until it became a public company for the first time in 1952. However, following WW2, British manufacturing stagnated through stifled investment and post-war austerity, and there was little innovation. Siebe Gorman's fortunes began to decline as an aging Sir Robert Davis failed to invest, or change the company's business and management practices. In 1959, Siebe Gorman was acquired by the “Fairy Group” and the ailing Sir Robert was made Life President. Consequently, nothing changed and the slow decline continued until Sir Robert's death in March 1965. Around 1960, Siebe Gorman acquired the diving apparatus manufacturer C E Heinke, and for a brief period, it manufactured some diving equipment under the combined name of Siebe Heinke. Around 1964, Mr E. 'Barry' Stephens was appointed as the new Managing Director to modernise Siebe Gorman. Changes were made, including a move to a new factory in Wales in 1975. The new company concentrated on fire-fighting breathing apparatus and escape equipment, and the move coincided with the loss of many of the older, traditional craft skills. Between 1985 and 1998, Siebe expanded through acquisitions, and several other companies were acquired. The Siebe Gorman (diving apparatus) company has therefore traded as A. Siebe (1819-1870); Siebe & Gorman (1870-1879); Siebe Gorman & Co (1880-1904); Siebe Gorman & Co. Ltd (1905-1998). (For information regards the diving helmet & Frank King see Notes Section at the end of this document)The items are very significant as a snapshot into marine history and the development of diving equipment generally especially that used for salvage operations before and during WW2. The company that made the equipment was a leading inventor,developer and innovator of marine equipment with its early helmets and other items eagerly sought after today for collections around the world. The items in the Flagstaff Hill collection give us an insight as to how divers operated and the dangers they faced doing a very necessary and dangerous job. Frank Kings' diving helmet and compressor (communication pipe stored separately). Compressor is hand cranked. US Navy diving helmet, Mark V. Two maker's plates attached. Made in 1944.On rear "WATER SUPPLY" On front 'PATENT" " Logo: Images (Lion, Crown, Horse, Shield within an oval) "SIEBE, GORMAN & Co. Ltd. SUBMARINE ENGINEERS, LONDON.flagstaff hill, warrnambool, maritime museum, great ocean road, us navy diving helmet, commonwealth government salvage, diving helmet, marine salvage, frank king, diver, siebe. gorman & co ltd, submarine equipment, diving equipment, communication under water, hand cranked, diving compressor -
 Flagstaff Hill Maritime Museum and Village
Instrument - Chronometer
... machinery and parts from the USA to Moscow in order to establish the factory. Twenty-one former "Dueber-Hampden" watchmakers, engravers and various other technicians helped to train the Russian workers in the art of watchmaking as part of the Soviet's first five-year plan. The movements of very-early...machinery and parts from the USA to Moscow in order to establish the factory. Twenty-one former "Dueber-Hampden" watchmakers, engravers and various other technicians helped to train the Russian workers in the art of watchmaking as part of the Soviet's first five-year plan. The movements of very-early ...First State Watch Factory: This factory was founded in 1930 under orders from Joseph Stalin, the "First State Watch Factory" was the first large-scale Soviet watch and mechanical movement manufacturer in the USSR. Via its USA-based trading company (Amtorg), the Soviet government bought the defunct Ansonia Clock Company of Brooklyn, New York in 1929, and the "Dueber-Hampden Watch Company of Canton", based in Ohio. The soviets moved twenty-eight freight cars full of machinery and parts from the USA to Moscow in order to establish the factory. Twenty-one former "Dueber-Hampden" watchmakers, engravers and various other technicians helped to train the Russian workers in the art of watchmaking as part of the Soviet's first five-year plan. The movements of very-early products were still stamped "Dueber-Hampden, Canton, Ohio, USA" (examples of these watches are very collectible today). In 1935 the factory was named after the murdered Soviet official Sergei Kirov. During the second world war, as the Germans closed in on Moscow in 1941, the factory was hurriedly evacuated to (Zlatoust USSR). By 1943 the Germans were in retreat, and the factory was moved back to Moscow, adopting the "First Moscow Watch Factory" name. In 1947 the first wristwatches under the brand name "Pobeda" and the first Marine Chronometers and Deck watches were produced. By 1951 the production of wristwatches had increased to 1.1 million. In 1975 new machinery and equipment for manufacturing complex watches were imported from Switzerland. The first chronograph called "Okean" (3133) was produced for the space station "Soyuz-23."The Chronometer is of recent manufacture and an excellent example of the type of instrument used to navigate the seas in the 19th century. It is of good quality and of a type regarded as very accurate and well made. The maker, First Watch Factory, has a dept that is still producing the "8916" standard Chronometer for horologists and collectors. Marine chronometer of Russian make in wooden case, metal handles on sides, inscription on a metal plaque on the front of the case. Polished square wooden outer case with green felt lining and, a leather carrying strap and buckle. Outer case is hinged and has a metal latch on the front. Outer case has a red velvet covering with a button and loop closure. Inscription on box are in Russian & translate as follows: ХРОНОМЕТР, = CHRONOMETER МОРСКОЙ, = NAUTICAL ГОСТ, 8916-77 = Gost ЛОЛ ЕТ, on dial face = LOL ETflagstaff hill, warrnambool, shipwrecked-coast, flagstaff-hill, flagstaff-hill-maritime-museum, maritime-museum, shipwreck-coast, flagstaff-hill-maritime-village, chonometer, russian, watch factory, marine, navigational instrument
